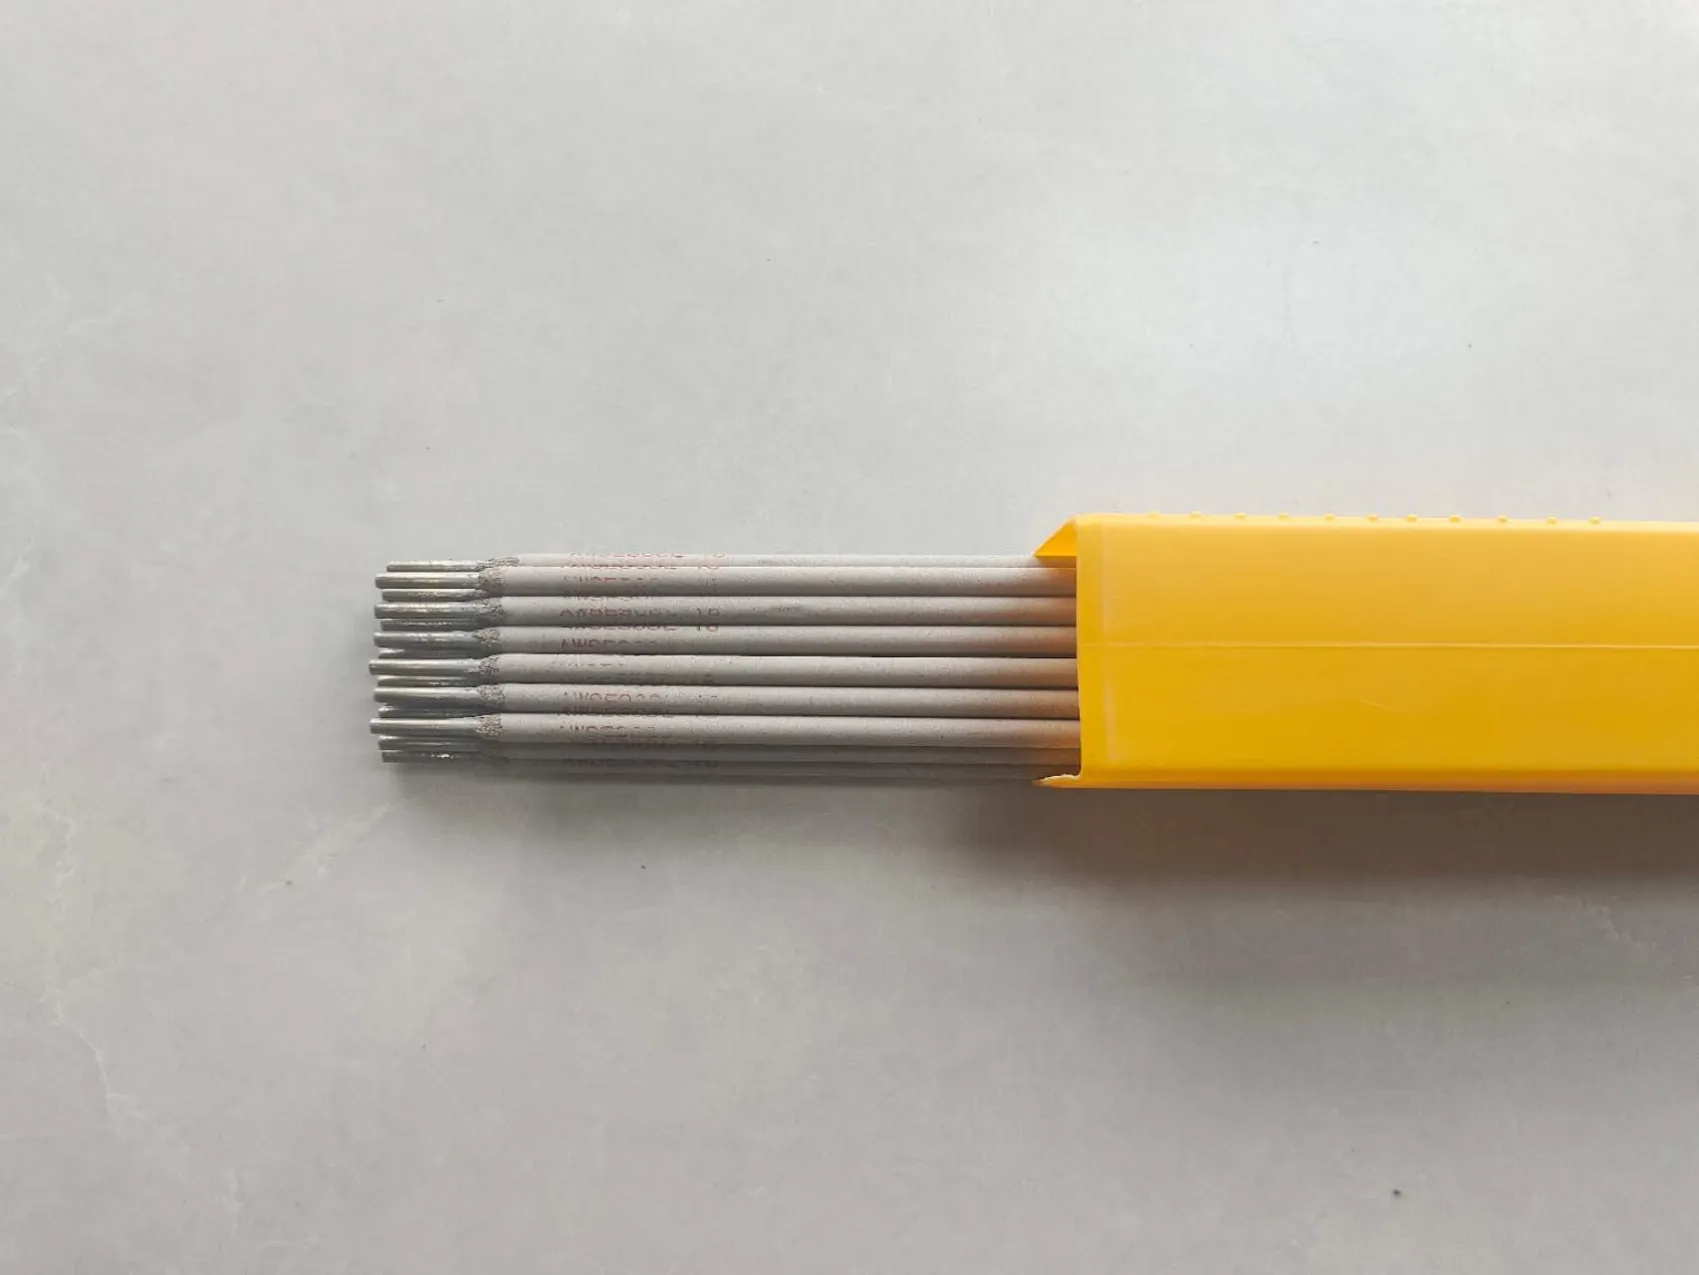
Welding Electrode
A607 E330MoMnWNb-15 High Temperature Stainless Steel Welding Electrode
A607 E330MoMnWNb-15 is a low-hydrogen austenitic stainless steel welding electrode classified under GB/T 983. It is designed for high-temperature stainless steel welding, particularly components operating at approximately 850–900°C. A607 is commonly used for hydrogen reformer furnace collector pipes, expansion pipes, Cr20Ni32 and Cr18Ni37 stainless steel components where high-temperature welding performance is required.
Key Features
- High-temperature service: Designed for applications at approximately 850–900°C.
- Cr16Ni35 austenitic weld metal: Provides a highly alloyed Cr-Ni weld deposit for demanding furnace applications.
- Mo-W-Nb alloy system: Contains controlled additions of molybdenum, tungsten and niobium for high-temperature service.
- Reformer furnace applications: Suitable for collector pipes and expansion pipes used in hydrogen reforming equipment.
- Specialty stainless steels: Applicable to Cr20Ni32 and Cr18Ni37 high-temperature stainless steels.
- Low-hydrogen coating: Basic coating with DC+ operation.
Applications & Base Materials
A607 is intended for specialty stainless steel welding rather than general fabrication.
Typical applications include:
- Hydrogen reformer furnace collector pipes
- Reformer furnace expansion pipes
- Cr20Ni32 stainless steel
- Cr18Ni37 stainless steel
- High-temperature furnace components
- High-temperature stainless steel fabrication and repair
- Industrial equipment operating at approximately 850–900°C
Its specific application range makes A607 particularly relevant to hydrogen production, petrochemical and high-temperature furnace equipment.
Classification & Welding Characteristics
Item | Specification |
|---|---|
Product Grade | A607 |
GB/T 983 | E330MoMnWNb-15 |
Weld Metal | Cr16Ni35 austenitic |
Coating | Low-hydrogen / basic |
Welding Process | SMAW / MMA |
Polarity | DC+ |
Welding Position | All-position |
Typical Diameter | 2.0–5.0 mm |
Typical Weld Metal Chemical Composition
Element | Reference (%) |
|---|---|
C | ≤0.20 |
Mn | ≤3.50 |
Si | ≤0.70 |
P | ≤0.035 |
S | ≤0.030 |
Cr | 15.0–17.0 |
Ni | 33.0–37.0 |
Mo | 2.0–3.0 |
Cu | ≤0.75 |
W | 2.0–3.0 |
Nb | 1.0–2.0 |
Actual weld-metal chemistry should be confirmed against the manufacturer's TDS or MTC.
Mechanical Properties
Property | Minimum Requirement |
|---|---|
Tensile Strength | ≥590 MPa |
Elongation | ≥25% |
Welding Current
Electrode Diameter | Current Range |
|---|---|
2.0 mm | 40–80 A |
2.5 mm | 50–100 A |
3.2 mm | 70–120 A |
4.0 mm | 90–160 A |
5.0 mm | 140–200 A |
Actual welding current should be selected according to electrode diameter, welding position, joint design and qualified WPS.
Electrode Drying
A607 electrodes should be properly dried before welding. Published product instructions commonly specify approximately 250°C for 1 hour. The manufacturer's current TDS should be followed for the exact redrying condition.
For critical furnace components, welding procedure qualification and control of heat input, interpass temperature and other welding conditions should follow the applicable project specification.
Supply from GD WELD
GD WELD supplies A607 E330MoMnWNb-15 stainless steel welding electrodes for high-temperature furnace, hydrogen reformer and specialty stainless steel welding applications.
For quotation, specify:
- Electrode diameter
- Quantity
- Base material
- Service temperature
- Applicable specification
- Certification and packaging requirements
Tags
A607, E330MoMnWNb-15, A607 welding electrode, E330MoMnWNb-15 welding electrode, A607 stainless steel electrode, high temperature welding electrode, high temperature stainless steel welding electrode, Cr16Ni35 welding electrode, Cr20Ni32 welding electrode, Cr18Ni37 welding electrode, hydrogen reformer welding electrode, reformer furnace welding electrode, furnace tube welding electrode, collector pipe welding electrode
Know more other Stainless Steel Welding Electrode,
Please Link,