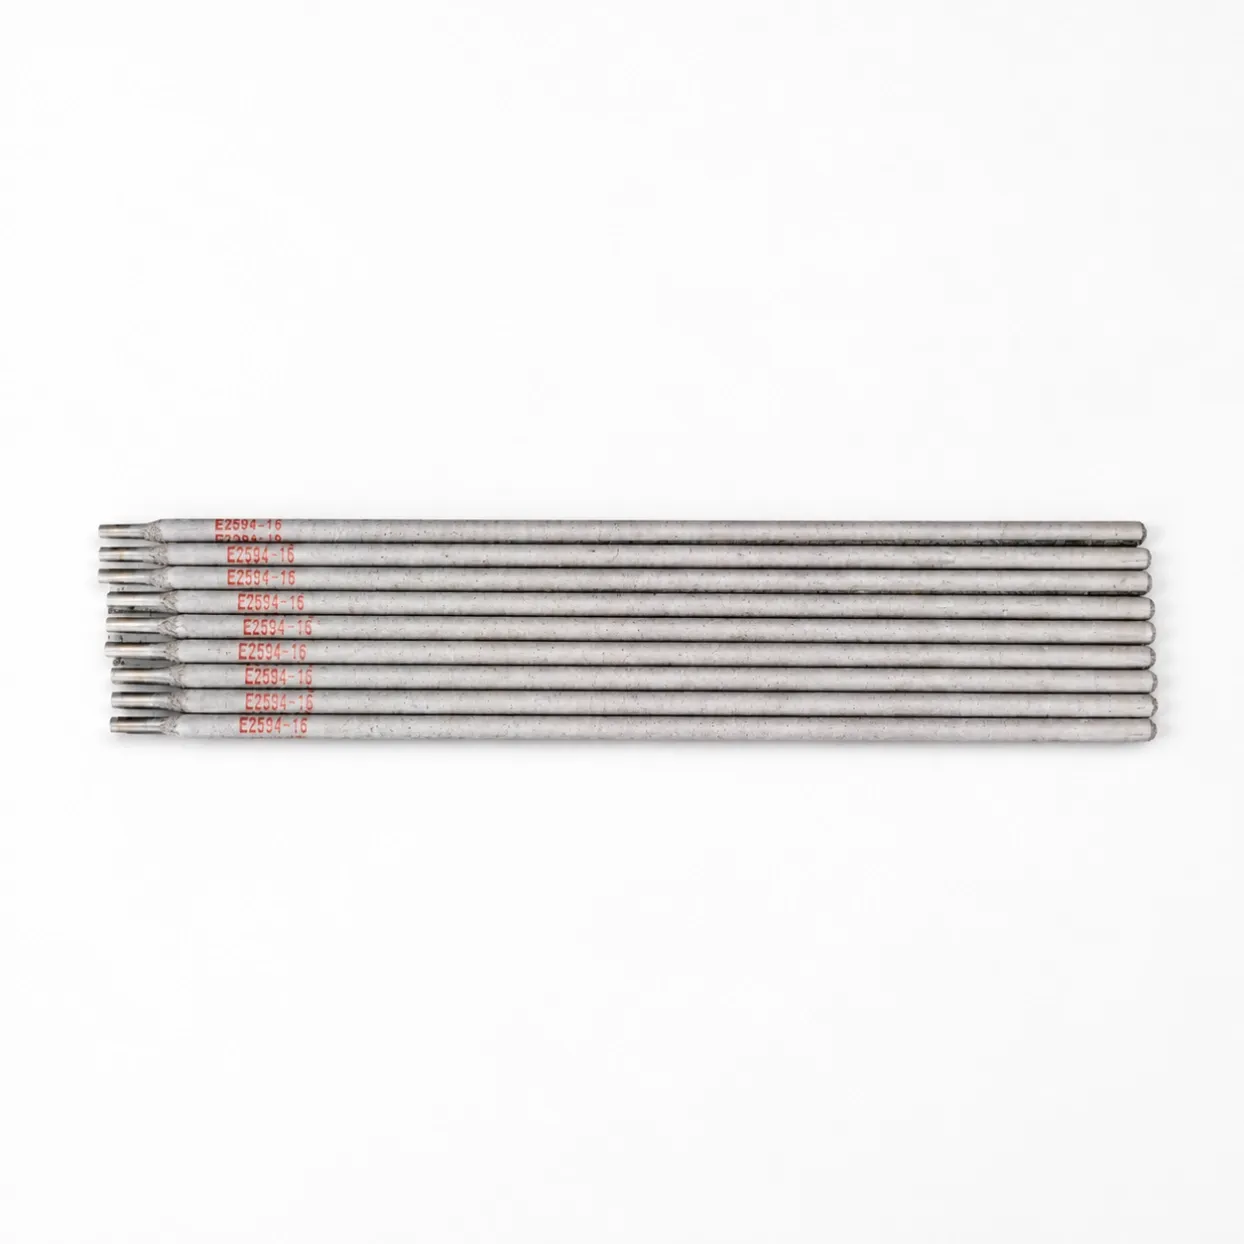
Welding Electrode
E2594-16 Super Duplex Welding Electrode
E2594-16 is a super duplex stainless steel welding electrode for SMAW applications on 2507-type materials. It provides high-strength weld metal with excellent resistance to pitting, crevice corrosion and stress corrosion cracking. It is commonly used for UNS S32750, UNS S32760 and similar super duplex stainless steels in offshore, oil & gas, seawater, chemical and pressure equipment applications.
For Super Duplex 2507 and Similar Grades
E2594-16 is designed for welding super duplex stainless steels with approximately 25% chromium, 9% nickel, 4% molybdenum and nitrogen.
Typical base materials include:
- UNS S32750 / 2507 / SAF 2507 / EN 1.4410
- UNS S32760 / Zeron 100 / EN 1.4501
- UNS S32550 and similar super duplex grades
- Selected super duplex castings such as ASTM A890 and A995 grades
It can also be considered for selected dissimilar joints between super duplex and stainless, carbon or low-alloy steels when the welding specification requires E2594-16 weld metal.
Typical Applications
E2594-16 is commonly selected where high strength and resistance to chloride corrosion are required.
Typical applications include:
- Offshore oil and gas equipment
- Seawater and desalination systems
- Chemical and petrochemical process equipment
- Pumps, valves and piping
- Pressure vessels and heat exchangers
- Marine equipment
- Flue gas and other chloride-containing environments
For 2507-type materials, E2594-16 is a matching SMAW consumable used to maintain the required super duplex weld-metal chemistry and corrosion resistance. Alleima lists AWS A5.4 E2594-16 as a recommended MMA/SMAW filler for SAF 2507.
International Classifications
Standard / Market | Classification |
|---|---|
USA / Canada | AWS A5.4 E2594-16 |
ASME | SFA-5.4 E2594-16 |
Europe | EN ISO 3581-A E 25 9 4 N L R |
EN ISO | ES2594-16 |
China | GB/T 983 E2594-16 |
Common material terms | 2507, UNS S32750, UNS S32760, SAF 2507, Zeron 100, EN 1.4410 |
The exact EN ISO suffix may vary with electrode coating and classification details; current commercial products include E 25 9 4 N L R 3 2.
Technical Data
Typical / Standard Chemical Composition of All-Weld Metal
Element | Reference Range / Limit |
|---|---|
C | ≤ 0.04% |
Si | ≤ 1.00% |
Mn | 0.5–2.5% |
P | ≤ 0.04% |
S | ≤ 0.03% |
Cr | 24.0–27.0% |
Ni | 8.0–10.5% |
Mo | 3.5–4.5% |
N | 0.20–0.30% |
Cu | ≤ 0.75% |
These values are reference classification limits and should not be treated as a guaranteed batch analysis. Actual weld-metal chemistry depends on the electrode manufacturer, batch and welding conditions.
Mechanical Properties
- Tensile Strength: ≥ 760 MPa reference minimum
- Elongation: ≥ 15% reference minimum
- Typical commercial products may show tensile strength around 820–935 MPa and elongation around 18–28%, depending on product and test conditions.
For a specific order, GD WELD can provide the applicable TDS and MTC for the supplied product.
Welding Parameters
E2594-16 is generally suitable for AC or DC+ (DCEP). Typical commercial current ranges are:
Diameter | Typical Current |
|---|---|
2.0 mm | 25–55 A |
2.5–2.6 mm | 50–85 A |
3.2 mm | 70–115 A |
4.0 mm | 95–150 A |
5.0 mm | 135–180 A |
Actual welding current should be selected according to electrode diameter, welding position, joint design and the manufacturer's TDS. Different manufacturers specify different ranges for flat, horizontal, vertical and overhead welding.
E2594-16 vs E2209-16
E2594-16 is primarily associated with super duplex 2507 / S32750 / S32760 and higher-alloy corrosion-resistant applications.
E2209-16 is primarily used for duplex 2205 / S31803 / S32205.
The two electrodes should not be selected only by strength. Base-metal grade, chloride exposure, corrosion requirements, welding procedure and applicable project specification should all be considered.
Tags
E2594-16, E2594-16 welding electrode, Super Duplex Welding Electrode, AWS A5.4 E2594-16, 2507 welding electrode, UNS S32750, UNS S32760, SAF 2507, Zeron 100, EN 1.4410, GB/T 983 E2594-16, duplex stainless steel electrode, offshore welding electrode, oil and gas welding electrode