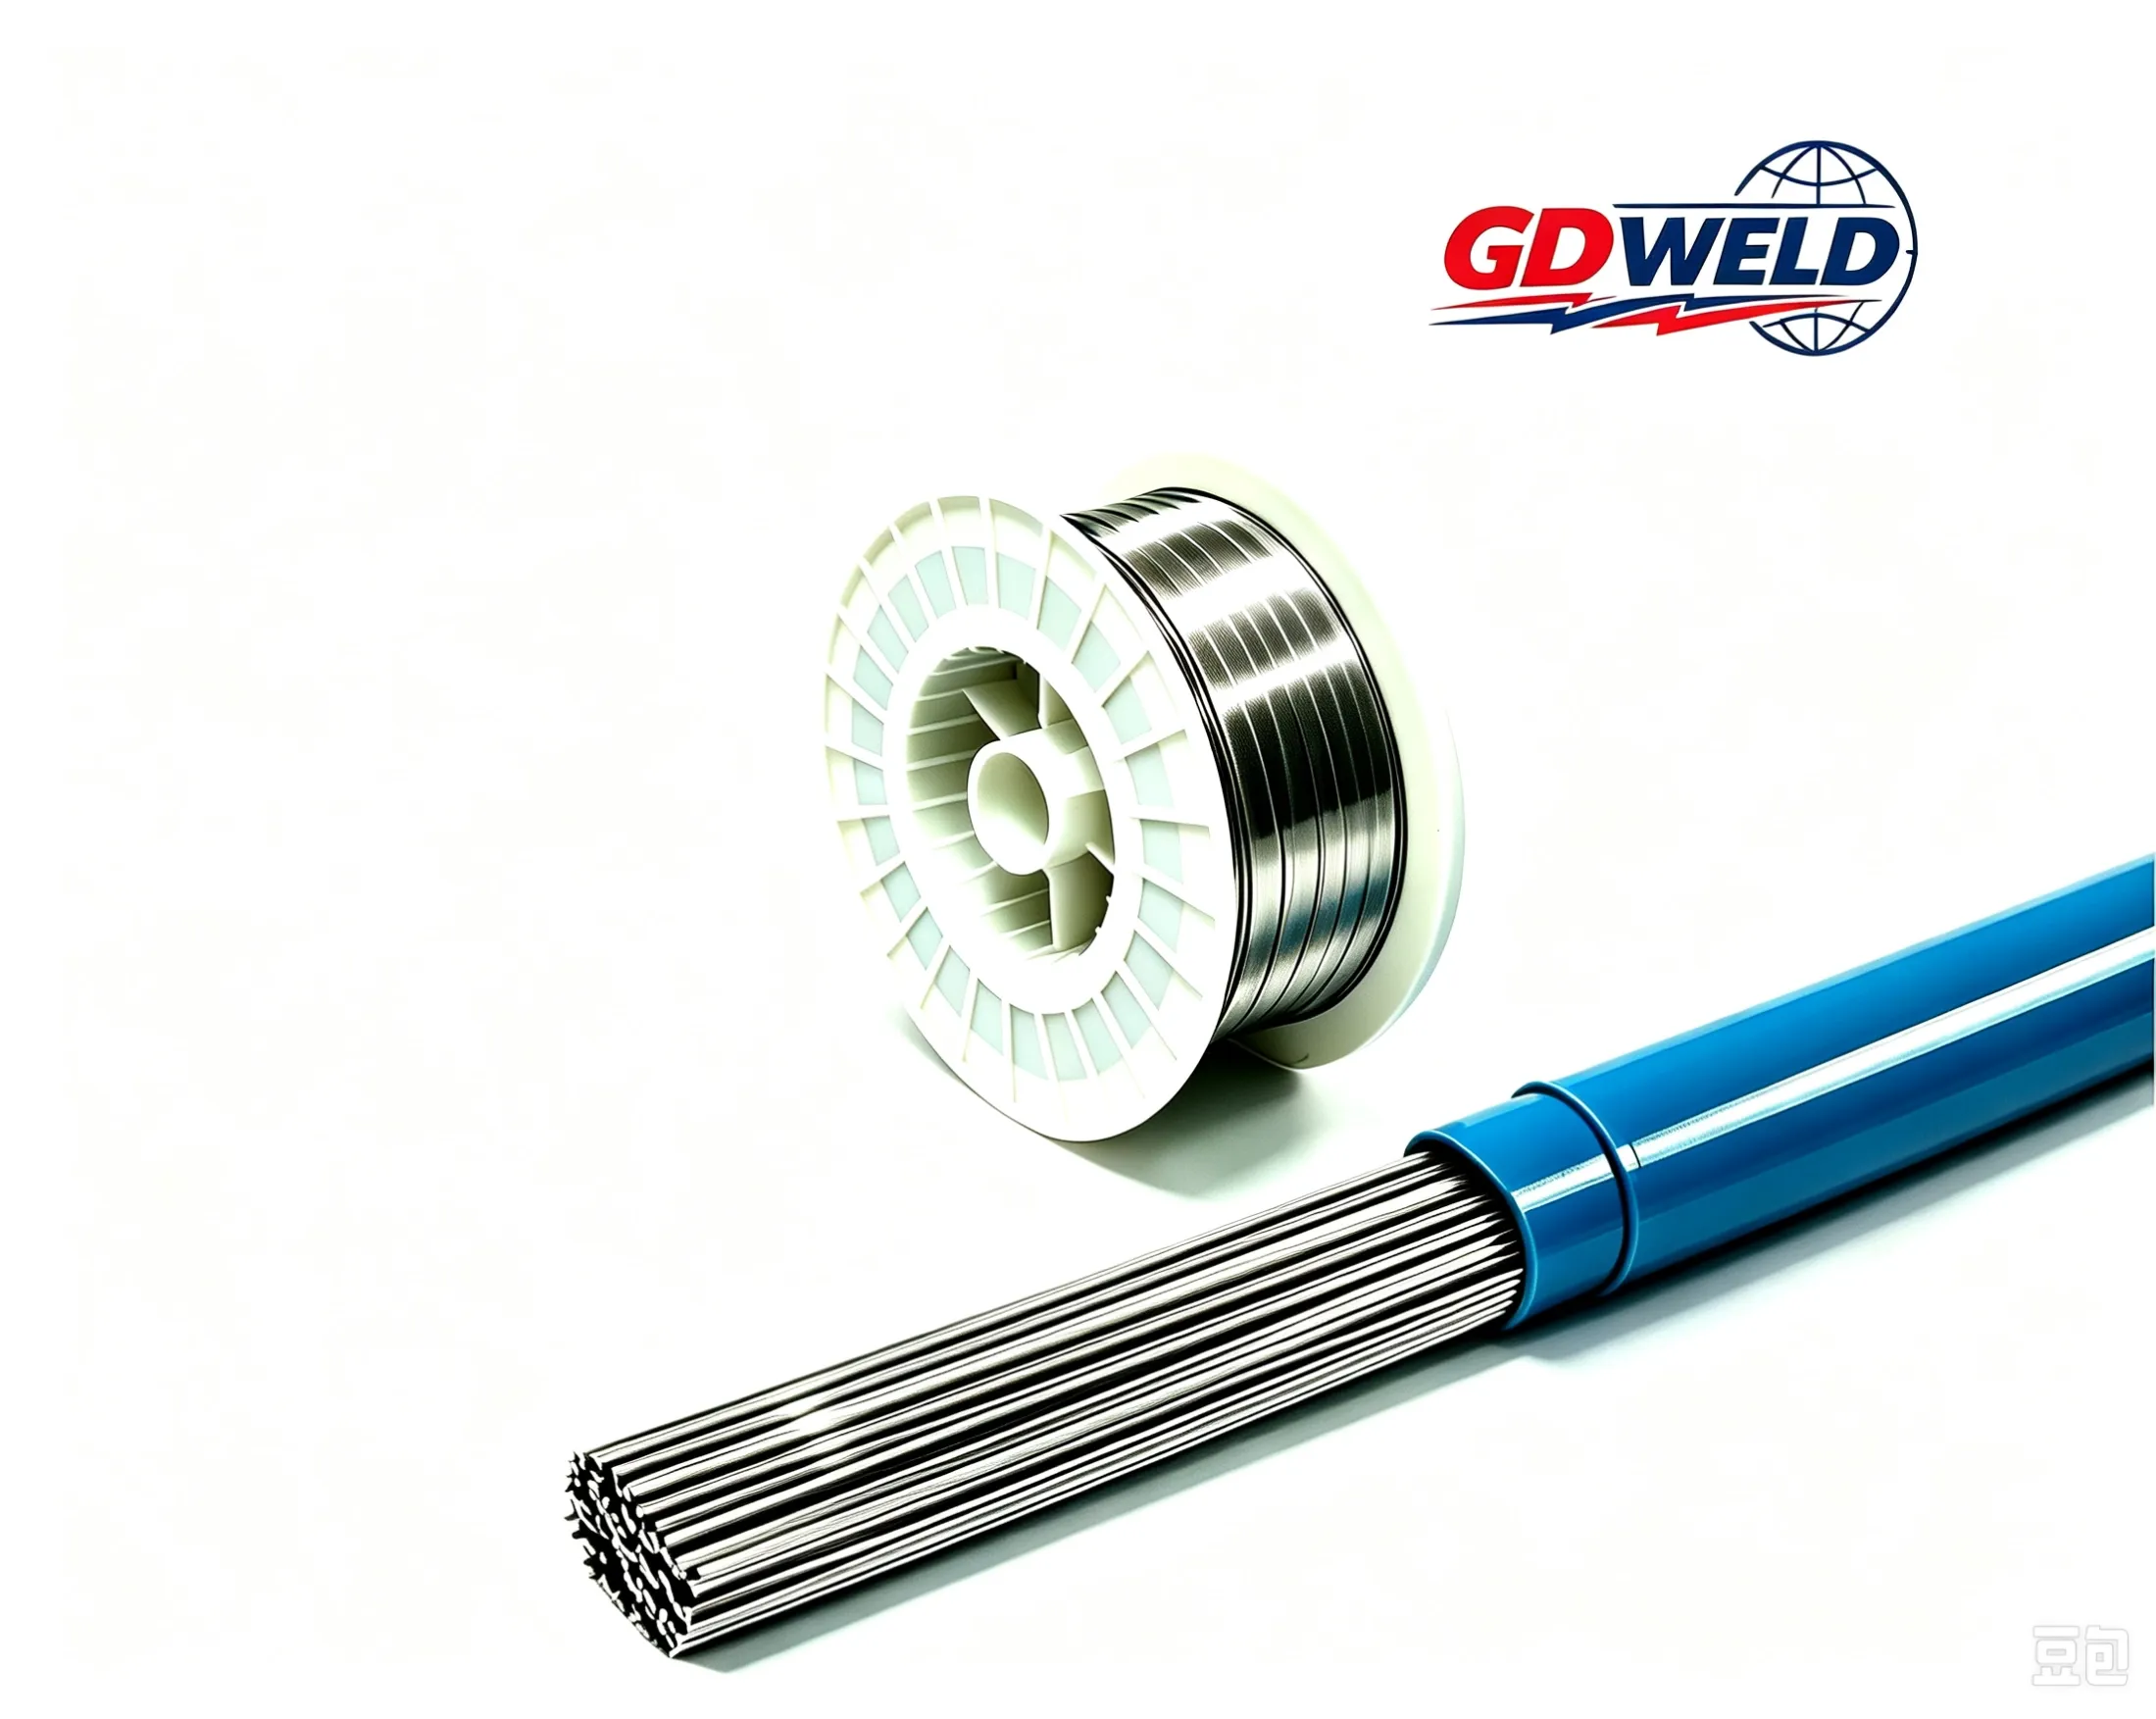
Welding Wire
ER316L
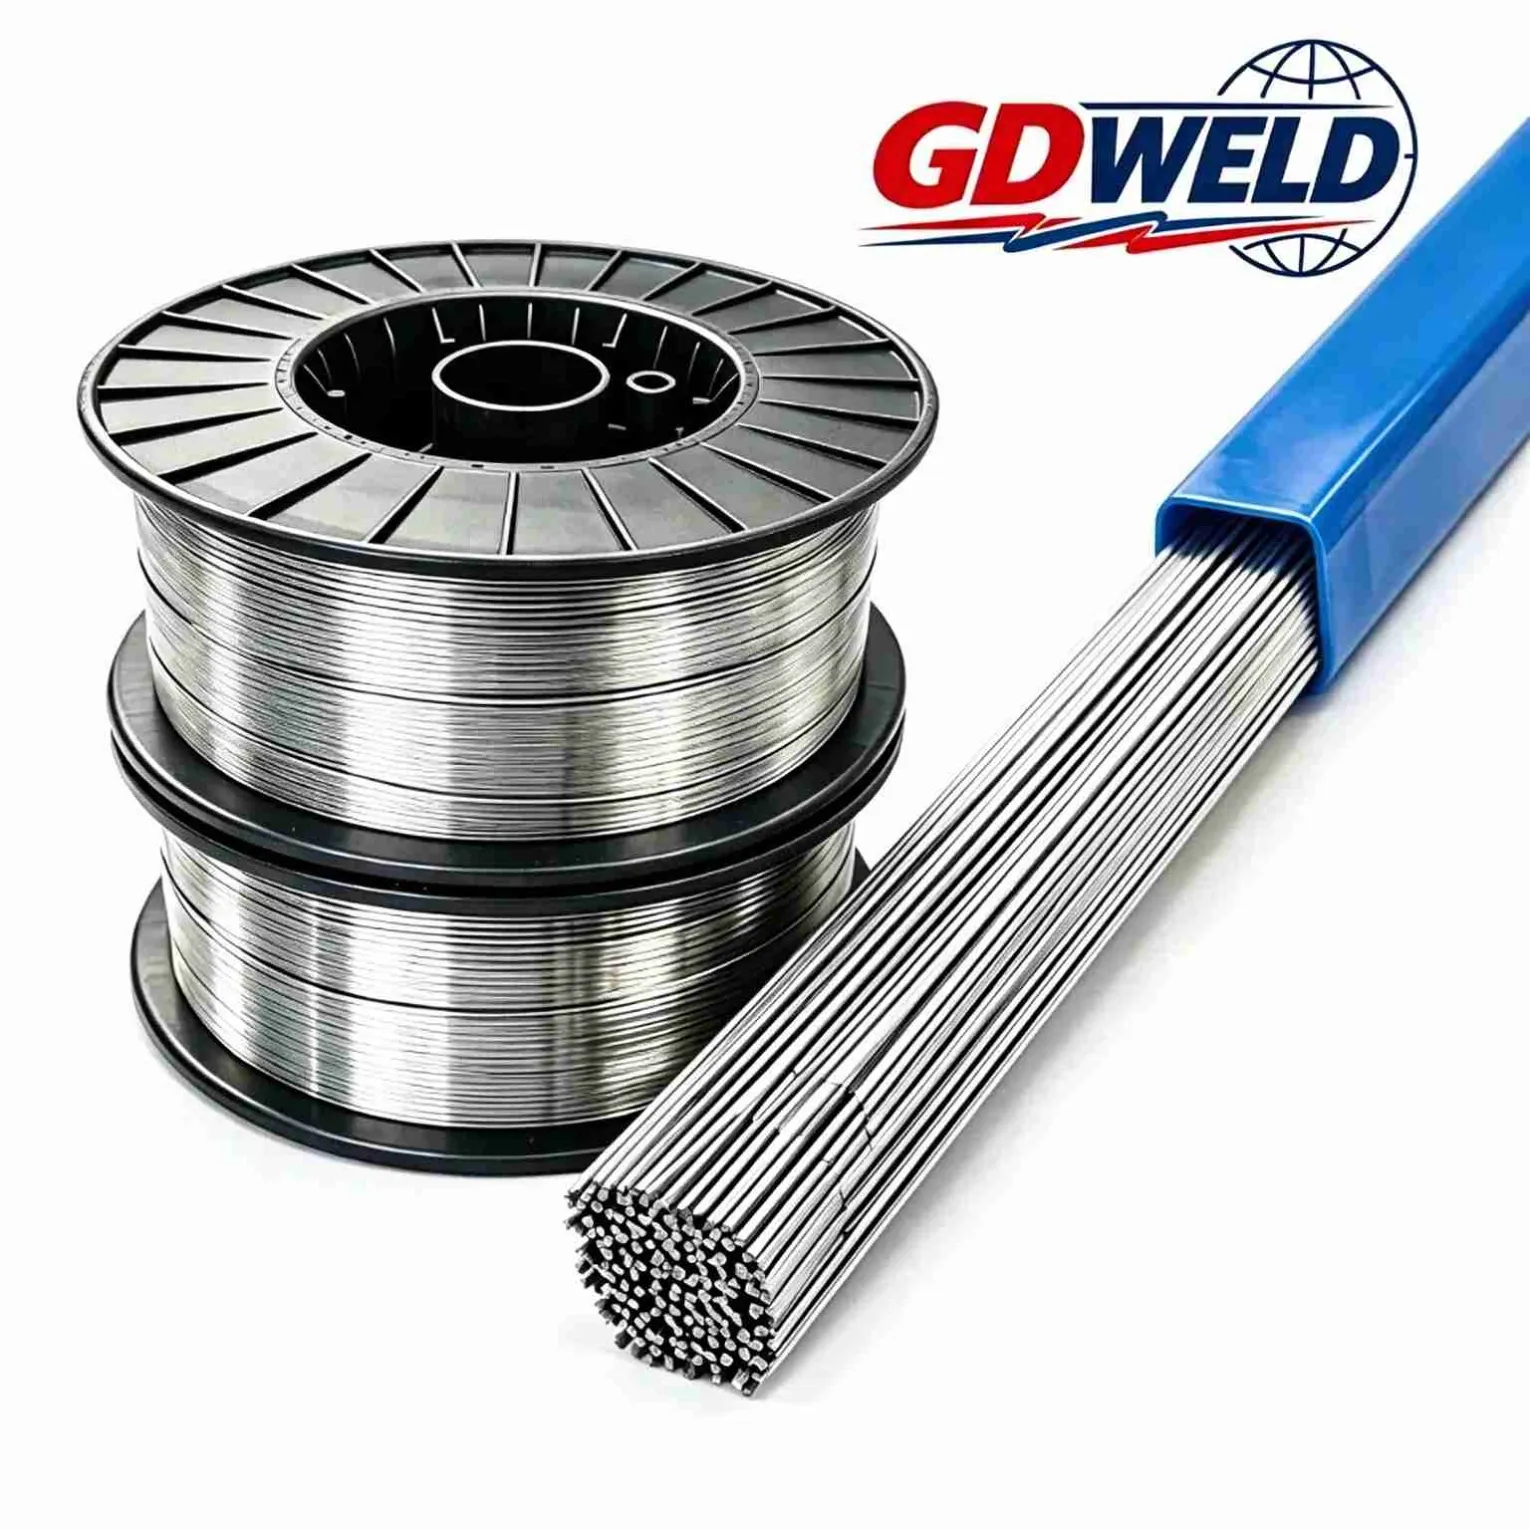
ER316L is copper-coated ultra-low carbon 19Cr-12Ni-2Mo austenitic stainless steel solid wire, suitable for GMAW (MIG/MAG) and GTAW (TIG) welding.
ER316L
ER316L is copper-coated ultra-low carbon 19Cr-12Ni-2Mo austenitic stainless steel solid wire, suitable for GMAW (MIG/MAG) and GTAW (TIG) welding.
Features
• Ultra-low carbon avoids intergranular corrosion; molybdenum element greatly improves pitting & chloride corrosion resistance
• Low ferrite content, excellent toughness at cryogenic temperature
• Stable arc, minimal spatter, smooth weld surface and good fluidity
• Excellent all-position welding, stable wire feeding; ideal for marine, chemical severe corrosion working conditions
• Continuous service temperature: ≤300°C
Diameter & Packaging
MIG:0.8 / 1.0 / 1.2 / 1.6 mm 1KG Spool/5KG Spool/15KG Spool
TIG:2.0 / 2.4 / 3.2 mm /4.0mm 5kg plastic tube
Welding Parameters
Polarity: DC+ (DCRP, Direct Current Reverse Polarity)
MIG / MAG
Shielding Gas: 98%Ar + 2%O₂ Gas Flow Rate: 20~25 L/min Reference Current for common sizes: Φ0.8mm:70–150 A Φ1.0mm:100–200 A Φ1.2mm:140–220 A
TIG (GTAW)
Shielding Gas: 99.99% High Purity Argon
Gas Flow Rate: 8–15 L/min. Back purging is recommended for thick plates.
Base Metal Matching
Suitable for 316 / 316L, 317L stainless steel; also weldable for 304/304L with chloride corrosion requirements.
Applications
Marine equipment, seawater pipelines, chemical reaction vessels, pharmaceutical machinery, food dairy equipment, cryogenic containers, desalination equipment.
⚠️ Not for carbon steel & stainless steel dissimilar welding (poor anti-crack performance)
Welding Precautions
• Thoroughly remove oil, rust, scale and moisture from grooves before welding to avoid porosity. Use stainless steel-specific grinding wheels/wire brushes to prevent carbon steel contamination.
• Control interpass temperature below 150°C. Adopt narrow bead welding to reduce heat input.
• Wind protection is required for outdoor welding if wind speed exceeds 1.0 m/s to avoid weld oxidation.
• Not recommended for dissimilar joints of carbon steel and stainless steel; select ER309L instead.
ER316L vs ER308L
✅ ER316L (contains Mo): First choice for chloride, seawater, acid medium corrosion environments, cryogenic equipment
✅ ER308L (Mo-free): Only for ordinary food, clean water non-chloride corrosion stainless steel
Important Cautions
• Do not use pure CO₂ or gas mixtures with high CO₂ content. It will increase carbon content in weld metal and drastically reduce corrosion resistance.
• Cannot be replaced by ER308L for chloride-containing corrosive working conditions.