What Is the Difference Between ER80S-B6 and ER80S-B8? Which One Should I Use?
ER80S-B6 and ER80S-B8 are both Cr-Mo welding wires, but they are designed for different material systems. So what is the difference, and can one replace the other?
Technical Blog
Practical guides for selecting welding consumables, understanding AWS classifications and solving material-specific welding challenges.

ER80S-B6 and ER80S-B8 are both Cr-Mo welding wires, but they are designed for different material systems. So what is the difference, and can one replace the other?

What welding wire is used for P91 steel? Should you use ER90S-B9 or ER90S-B91, and why are preheat and PWHT important?

What welding wire should you use for P11, P22, P5, P9 or P91 steel? Compare ER80S-B2, B3, B6, B8 and B9/B91 for Cr-Mo welding.

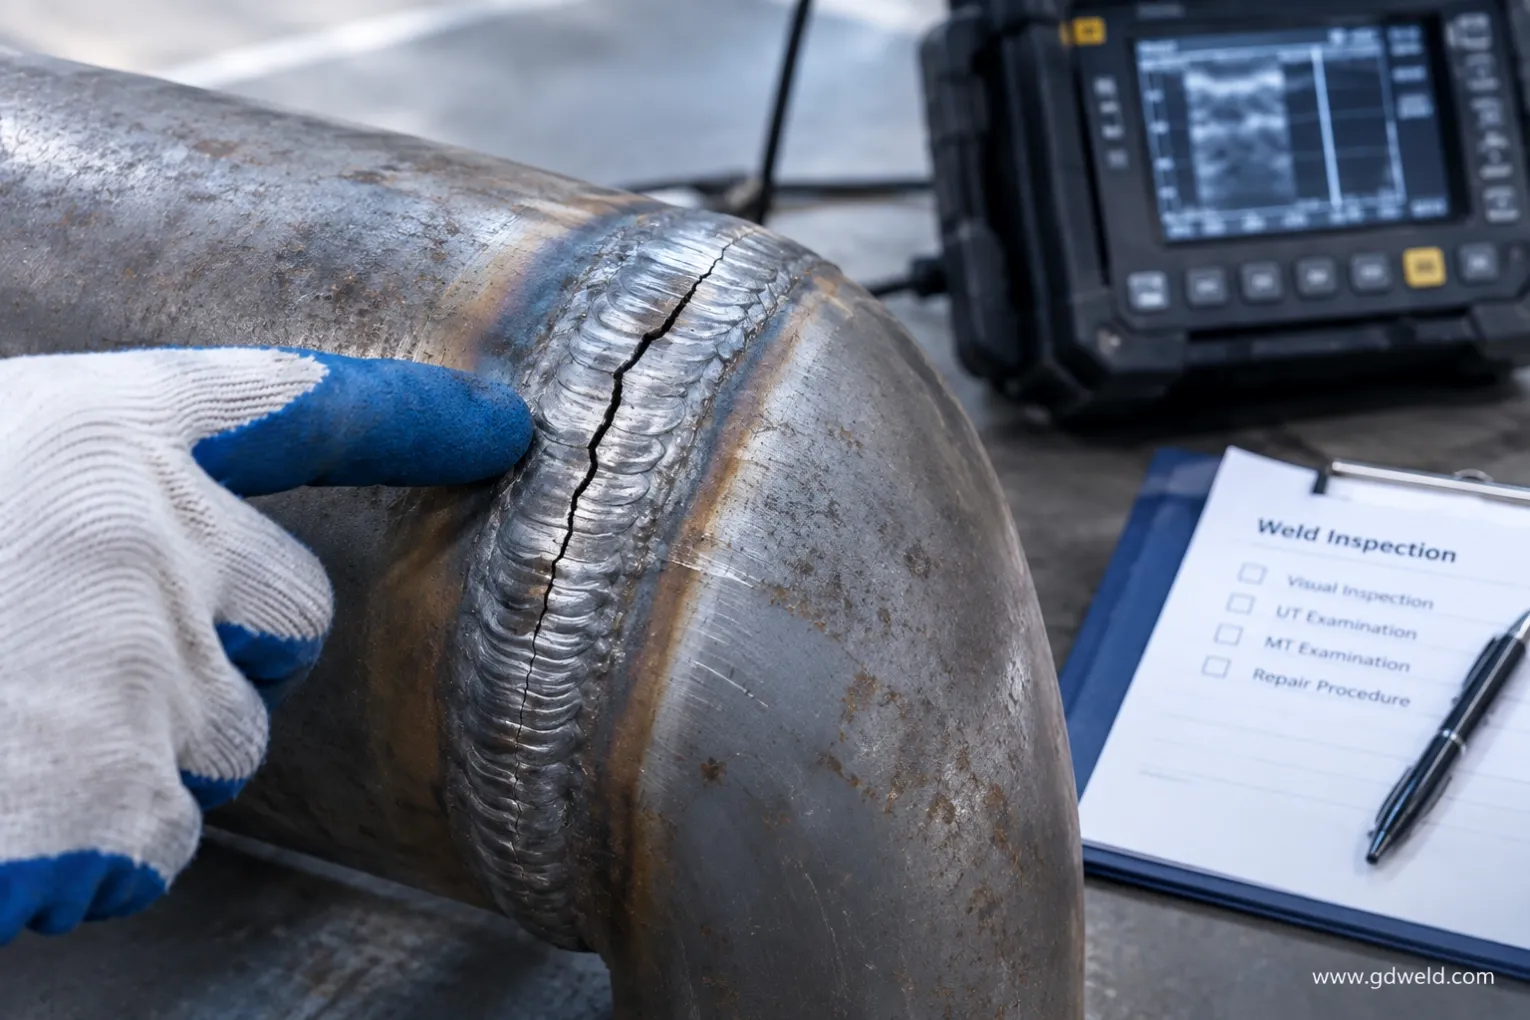
Why does high-strength steel crack after welding? What should you check before repairing the weld—crack location, timing, welding wire, preheat, or the WPS?

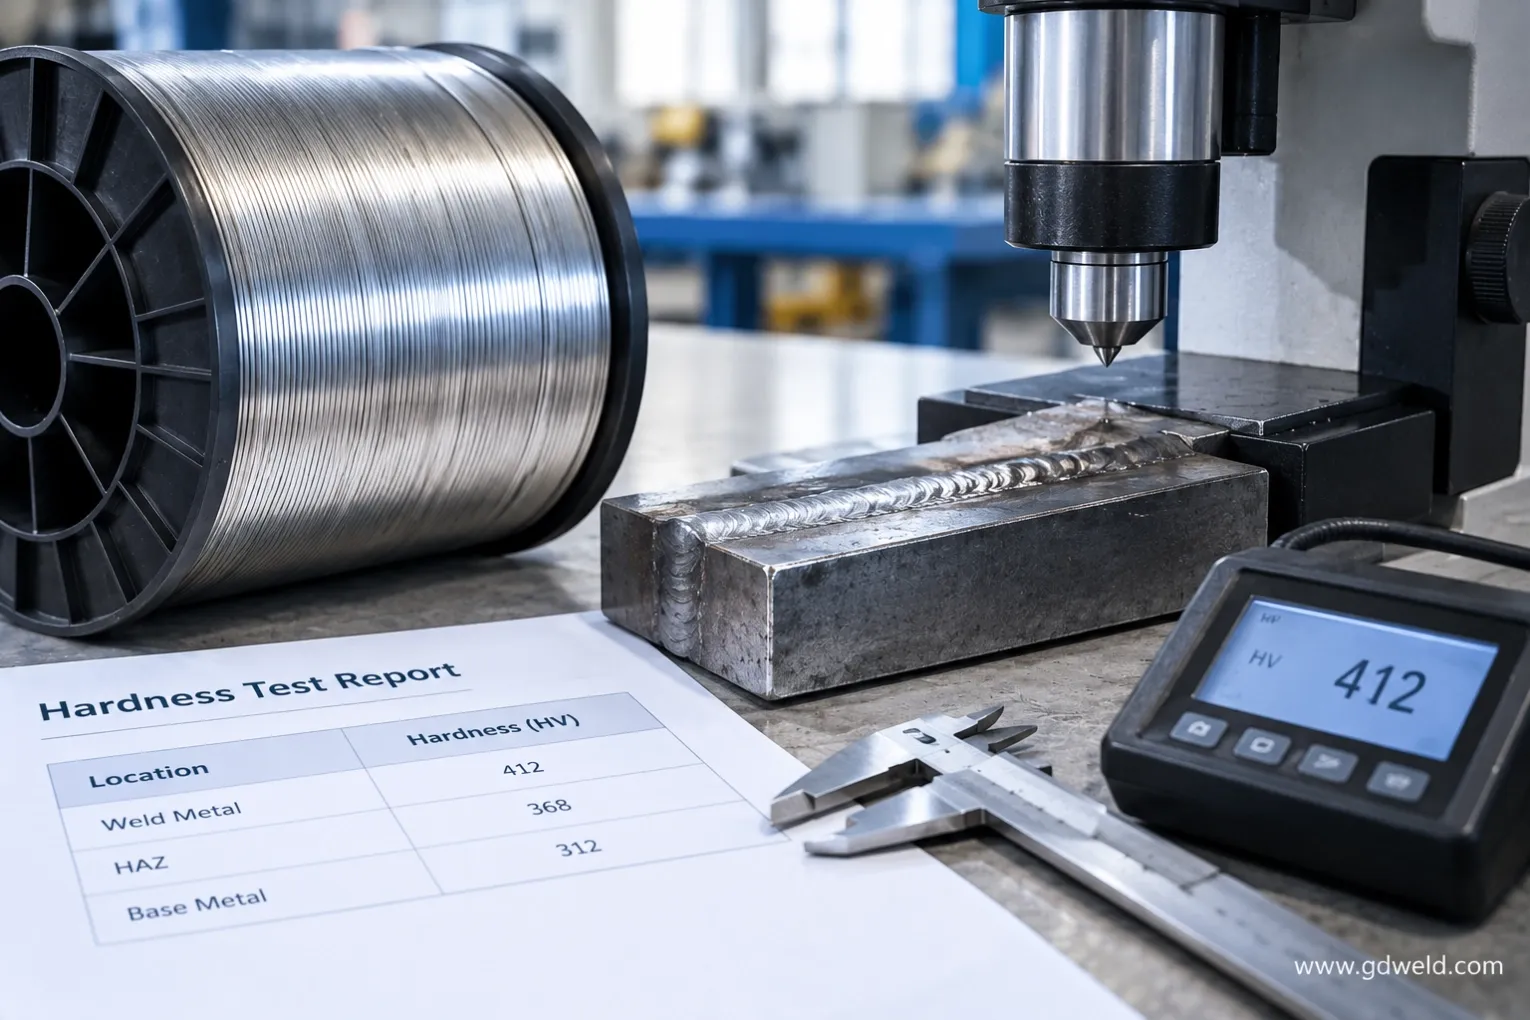
Why is my high-strength weld too hard after welding or PWHT? Is the problem the welding wire, HAZ, cooling rate, heat input, or heat treatment?

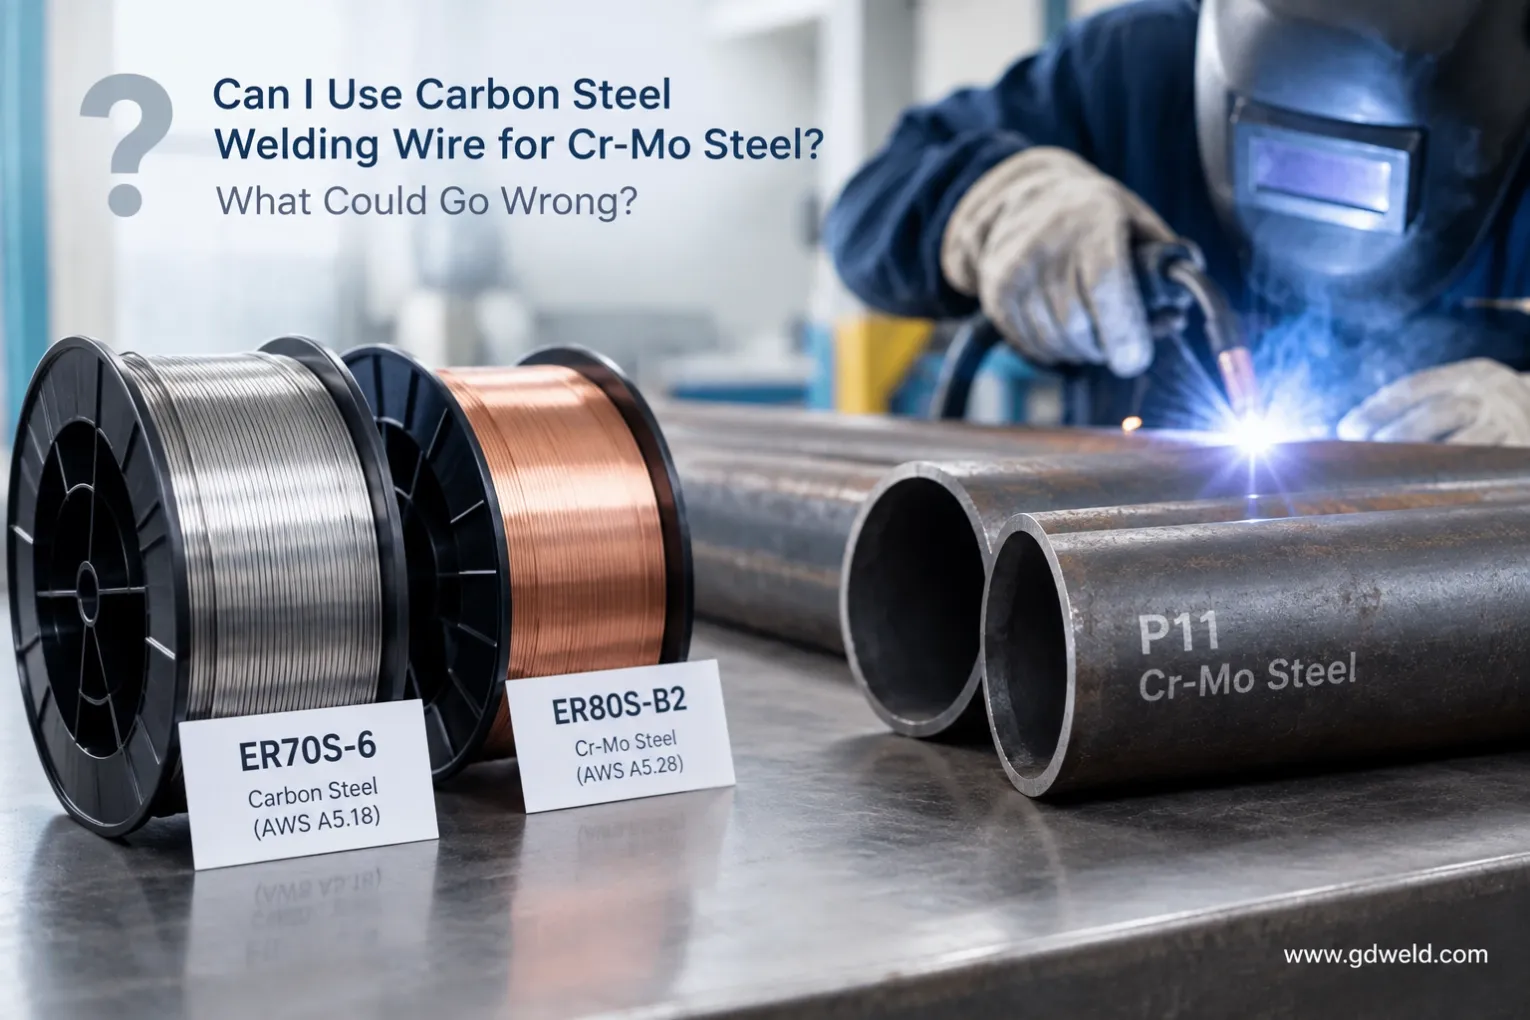
Can you use ER70S-6 carbon steel welding wire for Cr-Mo steel? What could go wrong, and when should ER80S-B2 or another Cr-Mo welding wire be used instead?

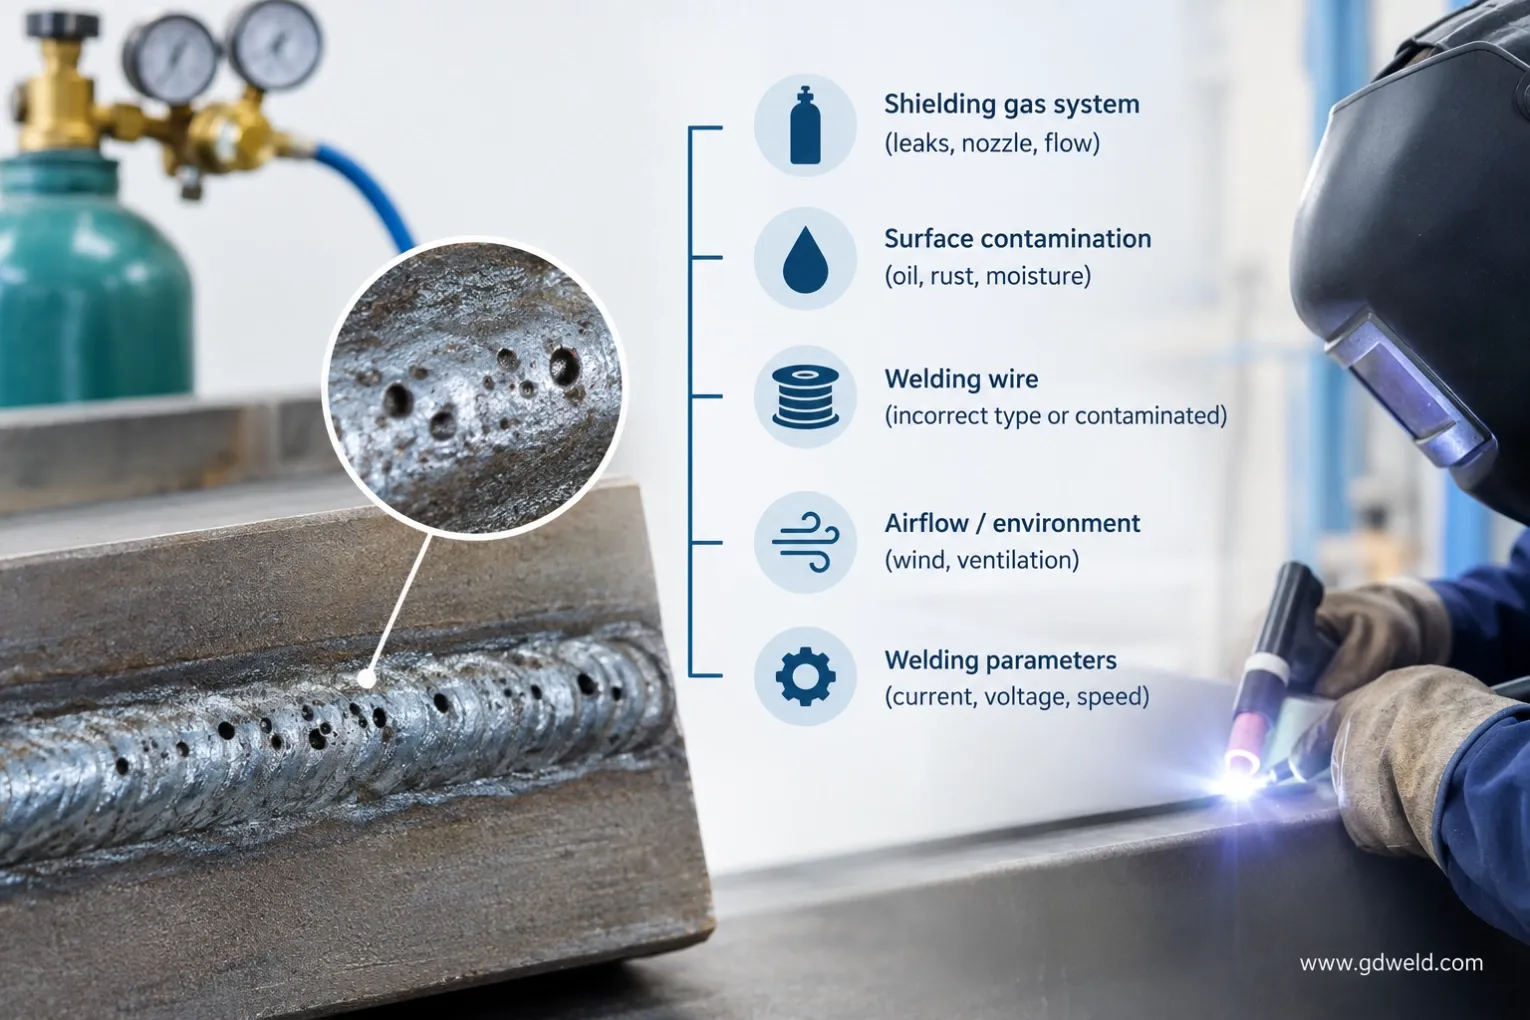
Low-alloy weld has porosity even when gas flow is normal? Find the likely causes in shielding, moisture, surface contamination, welding wire and parameters.

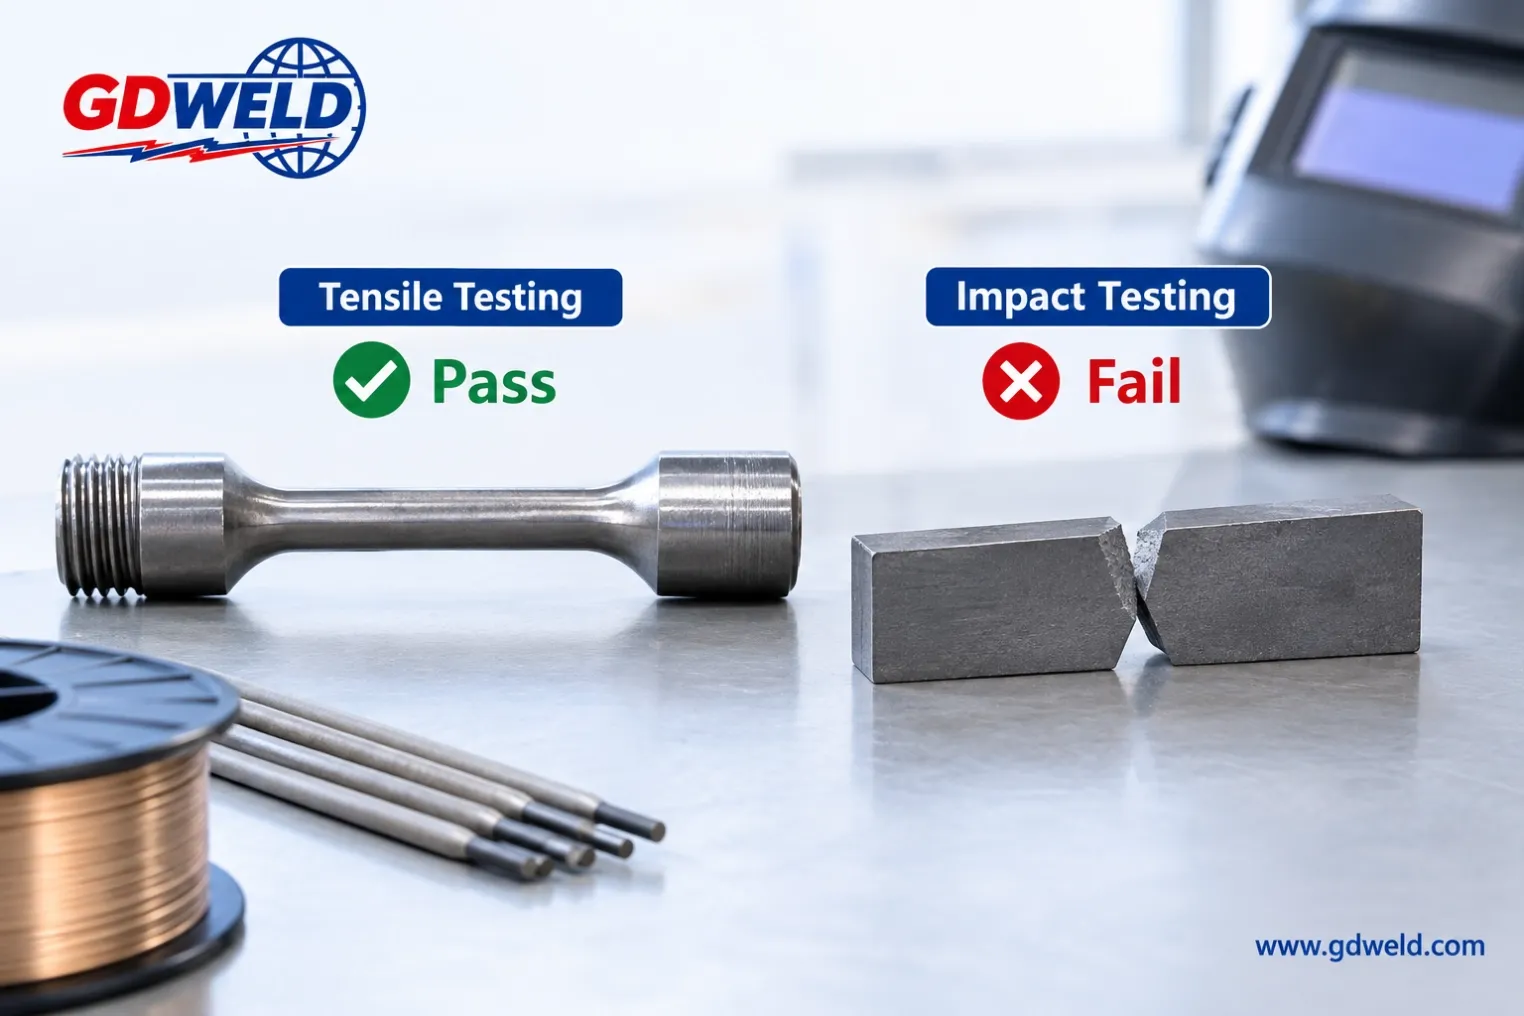
Why can a high-strength weld pass tensile testing but fail impact testing? Learn the common causes and how to improve weld impact toughness.

For Cr-Mo steel welding, PWHT is commonly used to reduce residual stress and obtain the required weld properties. But sometimes the weld hardness is still too high after PWHT.

Learn how ER80S-Ni1 welding wire is used for low-temperature steel, including pipelines, pressure vessels and tanks. Compare toughness, applications and key selection factors.
Recommended products
Popular pieces selected to support the routines, repairs, and ideas featured in our journal.

WE600 is a specialty alloy steel welding electrode associated with repair welding and dissimilar-metal applications. It is considered for selected difficult-to-weld steels and industrial components. Confirm the original product identity, technical data sheet (TDS), and compatibility with the base metal before use.

E71T-1M/9M is a gas-shielded flux cored welding wire classified under AWS A5.20 for suitable carbon steel and low-alloy steel applications. Its dual classification meets applicable E71T-1M and E71T-9M requirements, making it a candidate for specification-driven structural steel fabrication and industrial welding.

E307T1-1 stainless steel flux cored welding wire is an AWS A5.22-classified consumable for gas-shielded flux-cored arc welding. Its high-manganese austenitic weld metal is designed for selected difficult-to-weld materials, dissimilar-metal joints and applications requiring good resistance to weld cracking.