Aluminum & Copper Alloys
ER5183 Aluminum Welding Wire – MIG Wire & TIG Rods
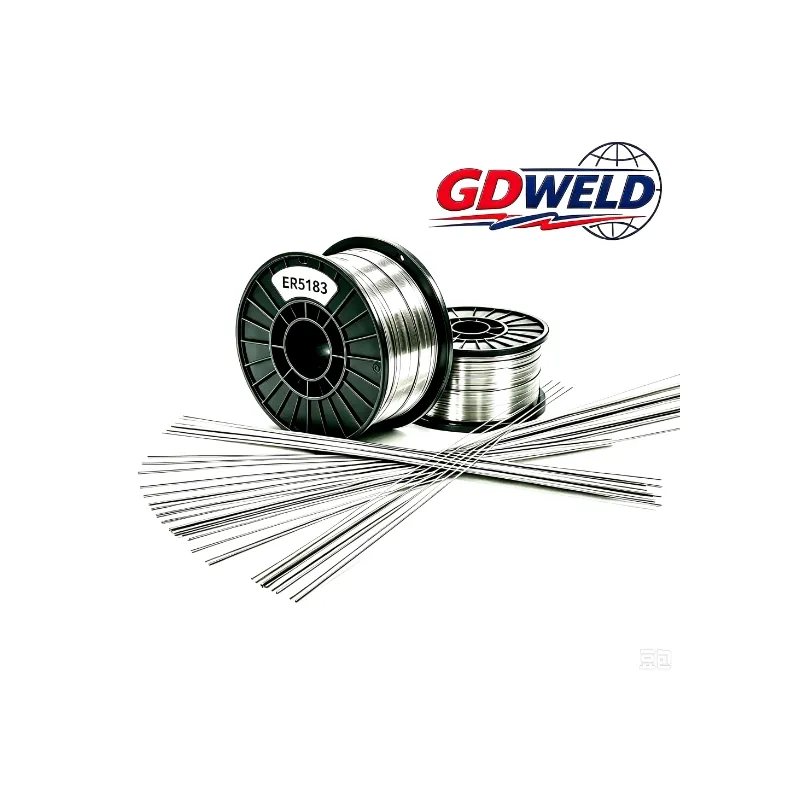
ER5183 is an aluminum-magnesium-manganese filler metal classified under AWS A5.10. With 4.3–5.2% magnesium, it is commonly selected for compatible high-magnesium aluminum alloys, including 5083 and 5086. Available in MIG wire and TIG filler rod forms, ER5183 is used in selected marine, transportation and low-temperature applications. Confirm the base alloy, service conditions and required properties before ordering.
ER5183 for 5083 Aluminum Welding Applications
ER5183 is an aluminum-magnesium-manganese filler metal used for welding compatible high-magnesium aluminum alloys. It is commonly considered for 5083, 5086 and selected 5456 aluminum applications where weld-metal strength and service performance are important.
For 5083 aluminum welding, ER5183 is a recognized filler-metal option. Suitability for a particular joint depends on the base-metal temper, design requirements, welding procedure and service environment.
Base-Metal Selection Guide
Base material or application | ER5183 selection considerations |
|---|---|
5083 aluminum plate | Verify required weld-metal strength and applicable welding code |
5086 aluminum structures | Confirm compatibility with the base alloy and joint design |
5456 aluminum | Check the qualified welding procedure and project requirements |
Marine aluminum structures | Assess corrosion requirements and service conditions |
Cryogenic equipment | Verify design qualification and required low-temperature properties |
Dissimilar aluminum alloys | Conduct a specific filler-metal compatibility assessment |
These are potential application areas, not a guarantee that ER5183 meets every project requirement.
Why Is ER5183 Specified for High-Magnesium Aluminum?
ER5183 combines magnesium with a controlled manganese addition. This Al-Mg-Mn composition distinguishes it from aluminum-silicon filler metals and makes it a candidate for compatible high-magnesium aluminum applications.
When selecting ER5183, consider:
- Weld-metal strength: Confirm that the filler classification and qualified procedure meet the joint's design requirements.
- Marine service: Evaluate the complete welding system, base material and exposure conditions.
- Low-temperature service: Confirm that the applicable design and qualification requirements are satisfied.
- Elevated-temperature exposure: Review the expected service temperature and duration, as prolonged elevated-temperature exposure can affect the performance of aluminum-magnesium weldments.
The filler metal alone does not guarantee corrosion resistance, mechanical performance or suitability for a specific service condition.
ER5183 Technical Specifications
Item | Specification |
|---|---|
AWS classification | AWS A5.10 ER5183 |
ISO classification | ISO 18273: S Al 5183 (AlMg4.5Mn0.7(A)); confirm the designation on the product certificate |
Alloy system | Aluminum-Magnesium-Manganese |
Product forms | MIG solid wire and TIG filler rods, subject to availability |
MIG polarity | DCEP |
Common shielding gas | 100% argon; Ar-He mixtures may be considered for specific procedures |
MIG wire diameters | 0.8, 0.9, 1.0, 1.2 and 1.6 mm, subject to availability |
TIG rod diameters | 1.6, 2.0, 2.4, 3.2, 4.0 and 5.0 mm, subject to availability |
TIG rod length | 1,000 mm, subject to availability |
Packaging | Confirm available spool sizes, rod packaging and order quantity |
Available dimensions and packaging should be confirmed before ordering. Welding current, voltage, gas flow and heat input depend on wire diameter, material thickness, joint configuration and the qualified welding procedure.
ER5183 Chemical Composition (wt.%)
The following are commonly published AWS ER5183 classification limits for reference. They are not batch-specific chemical analysis results.
Element | Composition (wt.%) |
|---|---|
Silicon (Si) | ≤ 0.40 |
Iron (Fe) | ≤ 0.40 |
Copper (Cu) | ≤ 0.10 |
Manganese (Mn) | 0.50–1.00 |
Magnesium (Mg) | 4.30–5.20 |
Chromium (Cr) | 0.05–0.25 |
Zinc (Zn) | ≤ 0.25 |
Titanium (Ti) | ≤ 0.15 |
Beryllium (Be) | ≤ 0.0003 |
Aluminum (Al) | Remainder |
Other elements | Each ≤ 0.05; total ≤ 0.15 |
Confirm the applicable standard edition and supplied product certificate when certified chemical composition is required.
Choosing the Right Aluminum Welding Wire
ER5183 is commonly considered for compatible 5083 and 5086 aluminum welding applications. Other filler metals may be more appropriate for different alloys or welding requirements.
- ER5356 aluminum welding wire: Review ER5356 Aluminum Welding Wire for compatible aluminum-magnesium welding applications.
- ER4043 aluminum welding wire: See ER4043 Aluminum Welding Wire for general welding applications involving compatible aluminum alloys.
- ER4047 aluminum welding wire: Explore ER4047 Aluminum Welding Wire when higher silicon content and weld pool fluidity are important selection factors.
These filler metals are not interchangeable in every application. Confirm the base-metal grade, service conditions, required weld properties and applicable welding procedure before making a final selection.
Important Checks Before Ordering ER5183
Base-metal grade: Identify the exact alloy and temper. Do not select filler metal by series number alone.
Service conditions: Marine exposure, low-temperature service and other demanding environments may impose additional requirements for corrosion performance, toughness or weld-metal properties.
Surface finish: If the component will be anodized, confirm appearance requirements and conduct a suitable trial when color matching is critical.
Certification: If the project requires classification certificates, batch traceability or third-party approvals, confirm these requirements before placing the order.
Mechanical properties: Use values from the applicable GD WELD technical data sheet or project qualification. Do not treat typical values from another manufacturer as guaranteed values for the supplied product.
Request a Quote for ER5183 Aluminum Welding Wire
Looking for ER5183 MIG wire or TIG filler rods for a specified 5083, 5086 or other compatible aluminum welding application?
Send GD WELD your base-metal grade, welding process, required diameter, packaging preference, order quantity and certification requirements. We can review your requirements and confirm available supply options.