Oct 19, 2026
Can ER2209 Solid Wire Replace E2209 Flux-Cored Wire for Duplex 2205?
Can you replace E2209 flux-cored wire with ER2209 solid wire for Duplex 2205? Learn what to check before changing your welding consumable.
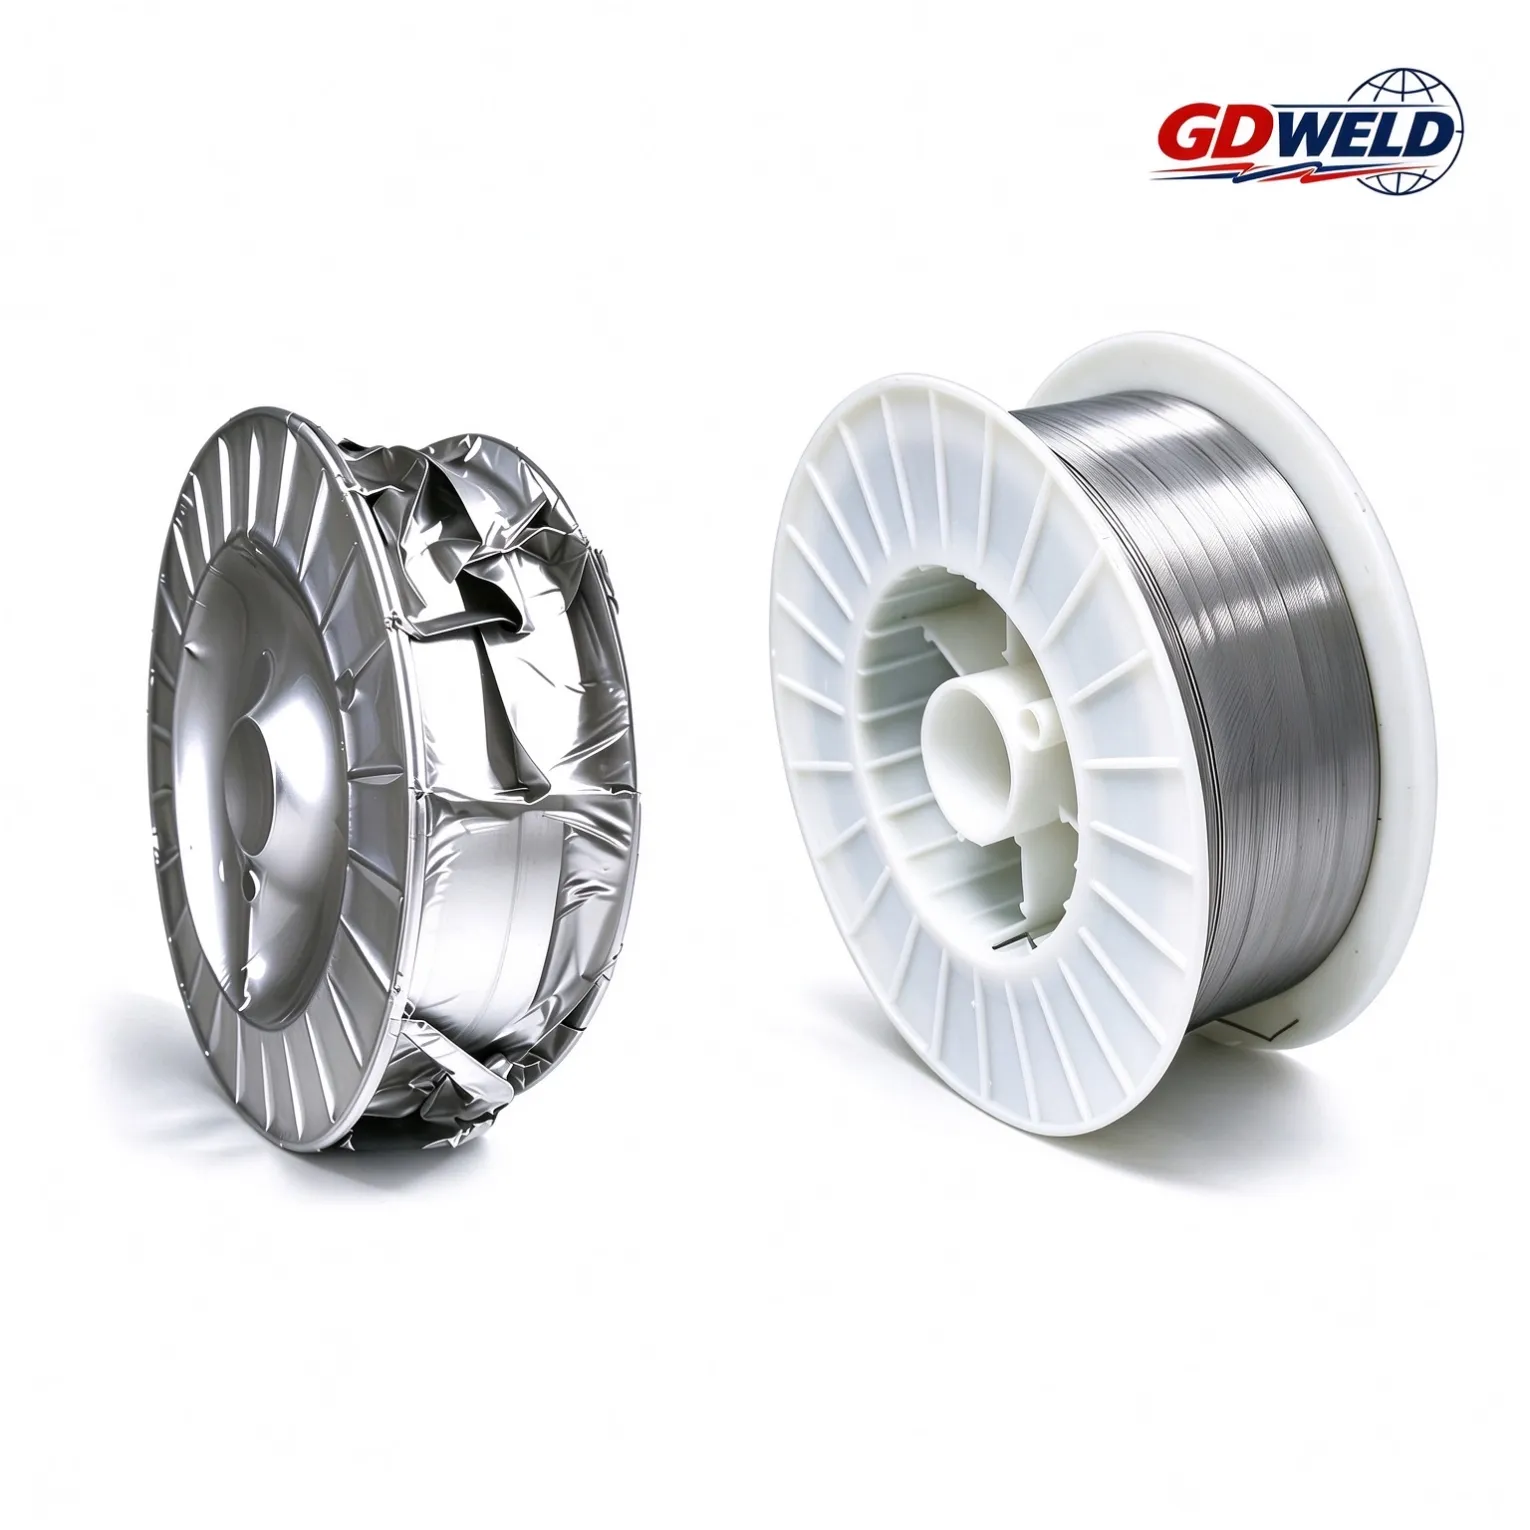
If E2209 flux-cored wire is unavailable, can you use ER2209 solid wire to weld Duplex 2205 stainless steel?
Not automatically. ER2209 may be a suitable alternative in some applications, but switching from flux-cored wire to solid wire can involve changing the welding process. You must check the consumable classification, qualified welding procedure, and project requirements before making the switch.
ER2209 vs E2209 Flux-Cored Wire: Key Differences
Factor | ER2209 Solid Wire | E2209 Flux-Cored Wire |
|---|---|---|
Product form | Solid wire | Tubular wire containing flux |
Typical process | GMAW (MIG); some products may suit GTAW | FCAW |
Common AWS specification | AWS A5.9 | AWS A5.22 |
Slag | No flux-derived slag from the wire itself | Slag may require removal between passes |
Main consideration | Process and shielding requirements | Full classification, shielding gas, and welding position |
Both consumables are used for duplex stainless steel applications, but the shared “2209” designation does not make them interchangeable. Their complete AWS classifications and technical data must be verified.
When Can ER2209 Replace E2209?
ER2209 solid wire may be worth evaluating when your specified E2209 flux-cored wire is unavailable, your facility has suitable solid-wire equipment, and the project permits the proposed process and consumable.
However, changing from FCAW to GMAW is a process change, not simply a wire substitution. Depending on the governing code and qualification requirements, a revised Welding Procedure Specification (WPS), additional procedure qualification, or customer approval may be necessary.
Before ordering, review the product details:
Confirm the exact AWS classification, wire diameter, shielding gas, and approved operating conditions for the specific product.
What Should You Check Before Switching?
1. Welding procedure and code requirements
Check whether the proposed welding process and consumable are permitted by the qualified WPS and applicable code. Do not assume an FCAW-qualified procedure automatically covers GMAW.
2. Weld properties
Duplex 2205 applications may require specified tensile strength, impact toughness, corrosion resistance, or ferrite limits. Verify these requirements against the project specification and product documentation rather than relying on the 2209 designation alone.
3. Heat input and welding parameters
Review shielding conditions, heat input, interpass temperature, and other applicable procedure limits. These factors influence duplex stainless steel weld-metal performance.
4. Total welding cost
Compare deposition rate, productivity, cleanup, equipment requirements, and labor—not just consumable price per kilogram. If availability is the only problem, first check whether the specified E2209 classification can be sourced from another qualified supplier.
Which Welding Wire Should You Choose for Duplex 2205?
Choose ER2209 solid wire when the proposed process is permitted, the consumable meets the project specification, and the applicable welding procedure supports its use.
Choose E2209 flux-cored wire when the qualified procedure requires the relevant FCAW classification or its operating characteristics better suit the application.
For a broader comparison of solid wire, flux-cored wire, and stick electrodes, read ER2209 vs E2209 for Duplex 2205: Solid Wire, Flux-Cored Wire, or Stick Electrode?.
Need Help Selecting Duplex 2205 Welding Consumables?
Send GD WELD your base material grade, required AWS classification, welding process, wire diameter, shielding gas, applicable standard, and estimated quantity. We can help you identify relevant products and provide technical information for evaluation.
Important: Any consumable substitution must comply with the applicable code, qualified welding procedure, and project approval requirements.