Sep 4, 2026
Welding Consumables for P11 Steel: Wire and Electrode Selection Guide
Learn which welding consumables are used for P11 steel, including ER80S-B2 wire and E8018-B2 electrodes, with selection and procurement tips.
Welding Consumables for P11 Steel: Wire and Electrode Selection Guide
Choosing the right welding consumable for P11 steel requires more than simply selecting a filler metal with sufficient tensile strength.
ASTM A335 P11 is a 1.25Cr-0.5Mo low-alloy steel commonly used in high-temperature piping and pressure-service applications. Because of its Cr-Mo chemistry and service conditions, the welding consumable should be compatible with the base metal and qualified welding procedure.
For buyers, one of the most common questions is:
What welding wire and electrode should be used for P11 steel?
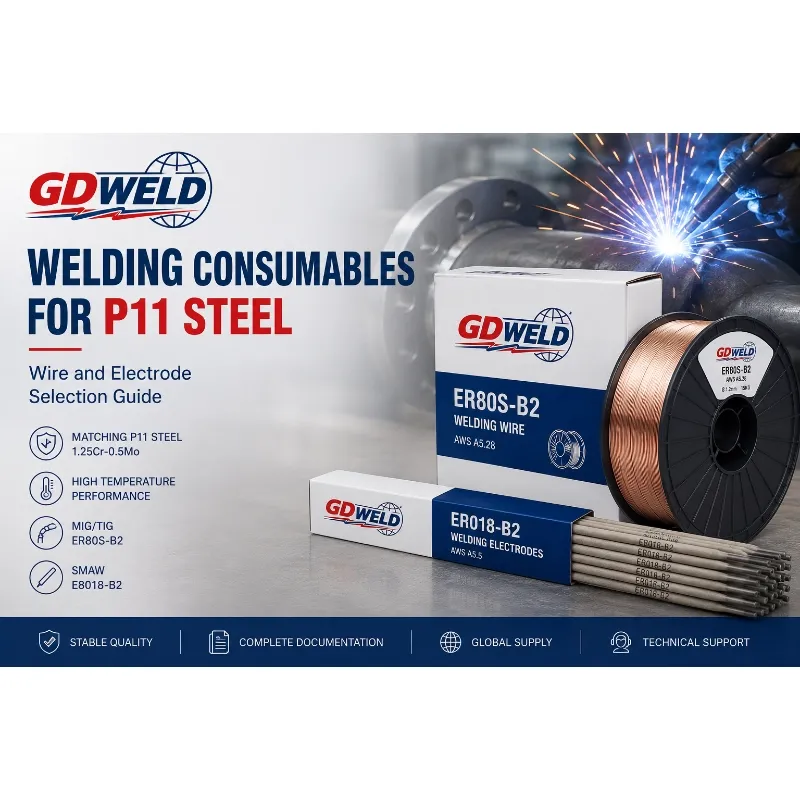
For typical matching applications, ER80S-B2 is commonly used for GMAW/GTAW, while E8018-B2 is commonly selected for SMAW. The final selection should always follow the applicable code and qualified WPS/PQR.
What Is P11 Steel?
P11 is a 1.25% chromium–0.5% molybdenum (1.25Cr-0.5Mo) alloy steel.
It is commonly used for:
- High-temperature piping
- Boiler components
- Steam systems
- Pressure vessels
- Heat exchangers
- Power generation equipment
- Petrochemical equipment
The Cr-Mo alloy system gives P11 better high-temperature performance than conventional carbon steel, which is why its welding consumables must be selected carefully.
What Welding Wire Is Used for P11 Steel?
For matching P11 steel applications, ER80S-B2 welding wire is a common choice for GMAW/MIG and GTAW/TIG welding.
ER80S-B2 is an AWS A5.28 low-alloy solid welding wire associated with the 1.25Cr-0.5Mo alloy system. It is commonly specified for P11/P12 and similar Cr-Mo steels.
For buyers searching for P11 steel welding wire, ER80S-B2 is therefore one of the key filler-metal classifications to consider.
Typical applications include:
- P11 pipe welding
- Boiler piping
- Heat-resistant steel fabrication
- Petrochemical equipment
- Power plant maintenance
GD WELD supplies copper-coated ER80S-B2 welding wire for MIG/TIG welding of P11 and compatible Cr-Mo steels.
What Welding Electrode Is Used for P11 Steel?
For SMAW, E8018-B2 is commonly used for P11 and other 1.25Cr-0.5Mo steels.
It is classified under AWS A5.5 and is a low-hydrogen Cr-Mo electrode designed for high-temperature and pressure-service applications.
The low-hydrogen design is particularly important when welding higher-hardenability Cr-Mo steels, where hydrogen and welding stresses can contribute to cracking.
ER80S-B2 vs E8018-B2: Which One Should You Choose?
The main difference is the welding process.
Consumable | AWS Specification | Welding Process | Typical P11 Application |
ER80S-B2 | A5.28 | GMAW / GTAW | MIG/TIG welding |
E8018-B2 | A5.5 | SMAW | Stick electrode welding |
Both are associated with the 1.25Cr-0.5Mo alloy system, but they are designed for different welding processes.
Therefore, the question is not simply:
“Which one is better?”
It is:
“Which welding process and qualified procedure are being used?”
Why Is ER80S-B2 Suitable for P11 Steel?
P11 is a Cr-Mo steel, so the filler metal needs to provide appropriate weld-metal chemistry and properties.
ER80S-B2 contains chromium and molybdenum corresponding to the 1.25Cr-0.5Mo alloy system. This makes it suitable for matching P11/P12-type materials when specified by the welding procedure.
This is also why a conventional carbon-steel wire such as ER70S-6 should not automatically be substituted for ER80S-B2 simply because it is cheaper or more readily available.
For critical Cr-Mo applications, material compatibility is more important than wire price.
What Should Buyers Check Before Purchasing P11 Welding Consumables?
A supplier may offer a product labeled “P11 welding wire,” but buyers should verify whether it actually meets the required specification.
Before ordering, check:
- AWS classification
- Chemical composition
- Mechanical properties
- Base-metal compatibility
- MTC / CoA
- Batch traceability
- Wire or electrode diameter
- Packaging
- WPS/PQR requirements
For electrodes, moisture control and proper storage are particularly important because low-hydrogen consumables are sensitive to handling and storage conditions.
P11 Welding Consumable Selection at a Glance
Requirement | Recommended Direction |
Base metal | ASTM A335 P11 / 1.25Cr-0.5Mo |
MIG / GMAW | ER80S-B2 |
TIG / GTAW | ER80S-B2 |
SMAW | E8018-B2 |
Main alloy system | 1.25Cr-0.5Mo |
Key consideration | Qualified WPS/PQR |
Important documents | TDS, MTC/CoA, batch traceability |
The exact consumable and welding parameters should always be confirmed against the project specification and qualified welding procedure.
What About Preheat and PWHT for P11 Steel?
P11 has relatively high hardenability compared with ordinary carbon steel, so welding procedures commonly require controlled preheat, interpass temperature and post-weld heat treatment (PWHT).
However, these values should not be copied directly from a product page and used as a project welding procedure.
The applicable WPS, construction code, material thickness, joint design and project requirements must determine the actual welding parameters.
Why Choose GD WELD for P11 Steel Welding Consumables?
GD WELD focuses on special AWS-standard welding consumables for industrial applications.
For P11 steel welding, GD WELD supplies ER80S-B2 welding wire and supports buyers with:
- Product technical specifications
- Chemical and mechanical data
- Batch traceability
- Export packaging
- OEM supply
- Sample support
For buyers sourcing P11 welding consumables, the focus is not simply on finding the lowest price. Stable quality, correct AWS classification and reliable documentation are essential for industrial projects.
Frequently Asked Questions
What welding wire is used for P11 steel?
ER80S-B2 is commonly used for matching P11 / 1.25Cr-0.5Mo steel in GMAW and GTAW applications, subject to the qualified welding procedure.
What electrode is used for P11 steel?
E8018-B2 is commonly used for SMAW welding of P11 and similar 1.25Cr-0.5Mo steels.
Can ER70S-6 be used for P11 steel?
It should not be treated as a direct replacement for ER80S-B2. P11 is a Cr-Mo steel, and filler-metal selection should consider alloy compatibility and the qualified WPS/PQR.
What is the difference between ER80S-B2 and E8018-B2?
ER80S-B2 is a solid wire/rod used mainly for GMAW/GTAW, while E8018-B2 is a coated electrode for SMAW. Both are associated with the 1.25Cr-0.5Mo alloy system.
Conclusion
For P11 steel welding, consumable selection should be based on the base-metal chemistry, welding process and qualified welding procedure.
For common matching applications:
GMAW / GTAW → ER80S-B2
SMAW → E8018-B2
Both are associated with the 1.25Cr-0.5Mo Cr-Mo steel system used by P11 materials.
For industrial procurement, always verify the AWS classification, chemical composition, technical documentation, traceability and WPS/PQR requirements before ordering.
If you are sourcing P11 welding wire or electrodes, GD WELD can provide technical specifications, documentation and sample support.