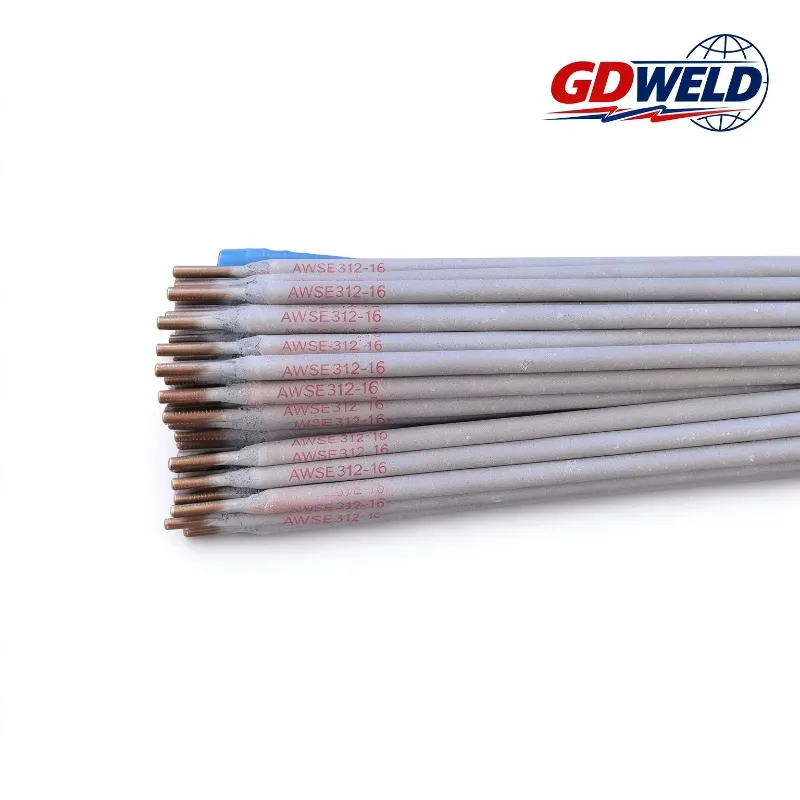
Welding Electrode
E312-16 Stainless Steel Welding Electrode
E312-16 is a high-alloy stainless steel covered electrode classified under AWS A5.4. Its chromium-rich weld metal, typically around 29% Cr and 9–10% Ni, offers good resistance to weld cracking in challenging applications. It is commonly selected for dissimilar-metal joints, difficult-to-weld steels, tool steel repairs and buffer layers before hardfacing. Confirm suitability against the base materials and qualified welding procedure.
Key Features
- High crack resistance: Suitable for selected dissimilar-metal joints and difficult-to-weld steels.
- High-alloy weld metal: Approximately 29% chromium and 9–10% nickel in typical deposits.
- Versatile repair applications: Used for selected tool steels, hardenable steels and stainless-clad components.
- SMAW process: A covered electrode for manual shielded metal arc welding.
Applications of E312-16 Welding Electrode
E312-16 is often chosen when weld-metal cracking is a concern because of base-metal composition, dilution or the combination of different steels.
Typical applications include:
- Welding stainless steel to carbon steel or suitable low-alloy steel
- Joining selected difficult-to-weld and hardenable steels
- Repairing tool steels, shafts, springs and industrial machinery
- Welding stainless-clad steel
- Depositing buffer layers before hardfacing or buildup welding
- Maintenance of heavy industrial equipment
The correct electrode depends on the base materials, service conditions and welding procedure. E312-16 is not a universal solution for every dissimilar-metal joint.
Chemical Composition of Deposited Weld Metal (wt.%)
Element | AWS E312-16 Classification Limit |
|---|---|
Carbon (C) | 0.15 max |
Manganese (Mn) | 0.50–2.50 |
Silicon (Si) | 1.00 max |
Chromium (Cr) | 28.0–32.0 |
Nickel (Ni) | 8.0–10.5 |
Molybdenum (Mo) | 0.75 max |
Phosphorus (P) | 0.04 max |
Sulfur (S) | 0.03 max |
Copper (Cu) | 0.75 max |
Note: These are AWS classification limits, not actual batch results. Verify the values against the applicable AWS A5.4 edition and GD WELD's current technical data sheet.
Technical Specifications
Item | Details |
|---|---|
AWS classification | E312-16 |
Standard | AWS A5.4 / ASME SFA-5.4, where applicable |
Welding process | Shielded Metal Arc Welding (SMAW) |
Product type | Covered stainless steel electrode |
Current and polarity | Follow the product TDS |
Available diameters | Confirm current supply range |
Packaging | Confirm current options |
Welding Recommendations
Use the recommended current range for the electrode diameter and keep the arc length controlled. Follow the manufacturer's instructions for electrode storage, redrying and exposure limits.
For highly hardenable steels, preheating and interpass temperature control may be required. Determine these conditions through the qualified welding procedure rather than applying one temperature to all base materials.
Related Welding Products
E309L-16 Stainless Steel Welding Electrode
E309L-16 is a low-carbon Cr-Ni electrode commonly used for specified stainless steel-to-carbon steel joints and selected cladding applications. It offers a different weld-metal composition from E312-16.
ER312 Stainless Steel Welding Wire
ER312 is a solid filler wire in the 29Cr-9Ni alloy family for compatible GMAW and GTAW applications. It is an alternative product form when a solid wire or TIG filler rod is required instead of a covered electrode.
Choose the product according to the welding process, base materials and specified weld-metal properties.
Ordering Information
For a quotation, please provide the required diameter, quantity, base-metal grades, applicable specification, packaging requirements and destination country.
Contact GD WELD for current availability, technical documentation and export pricing.