
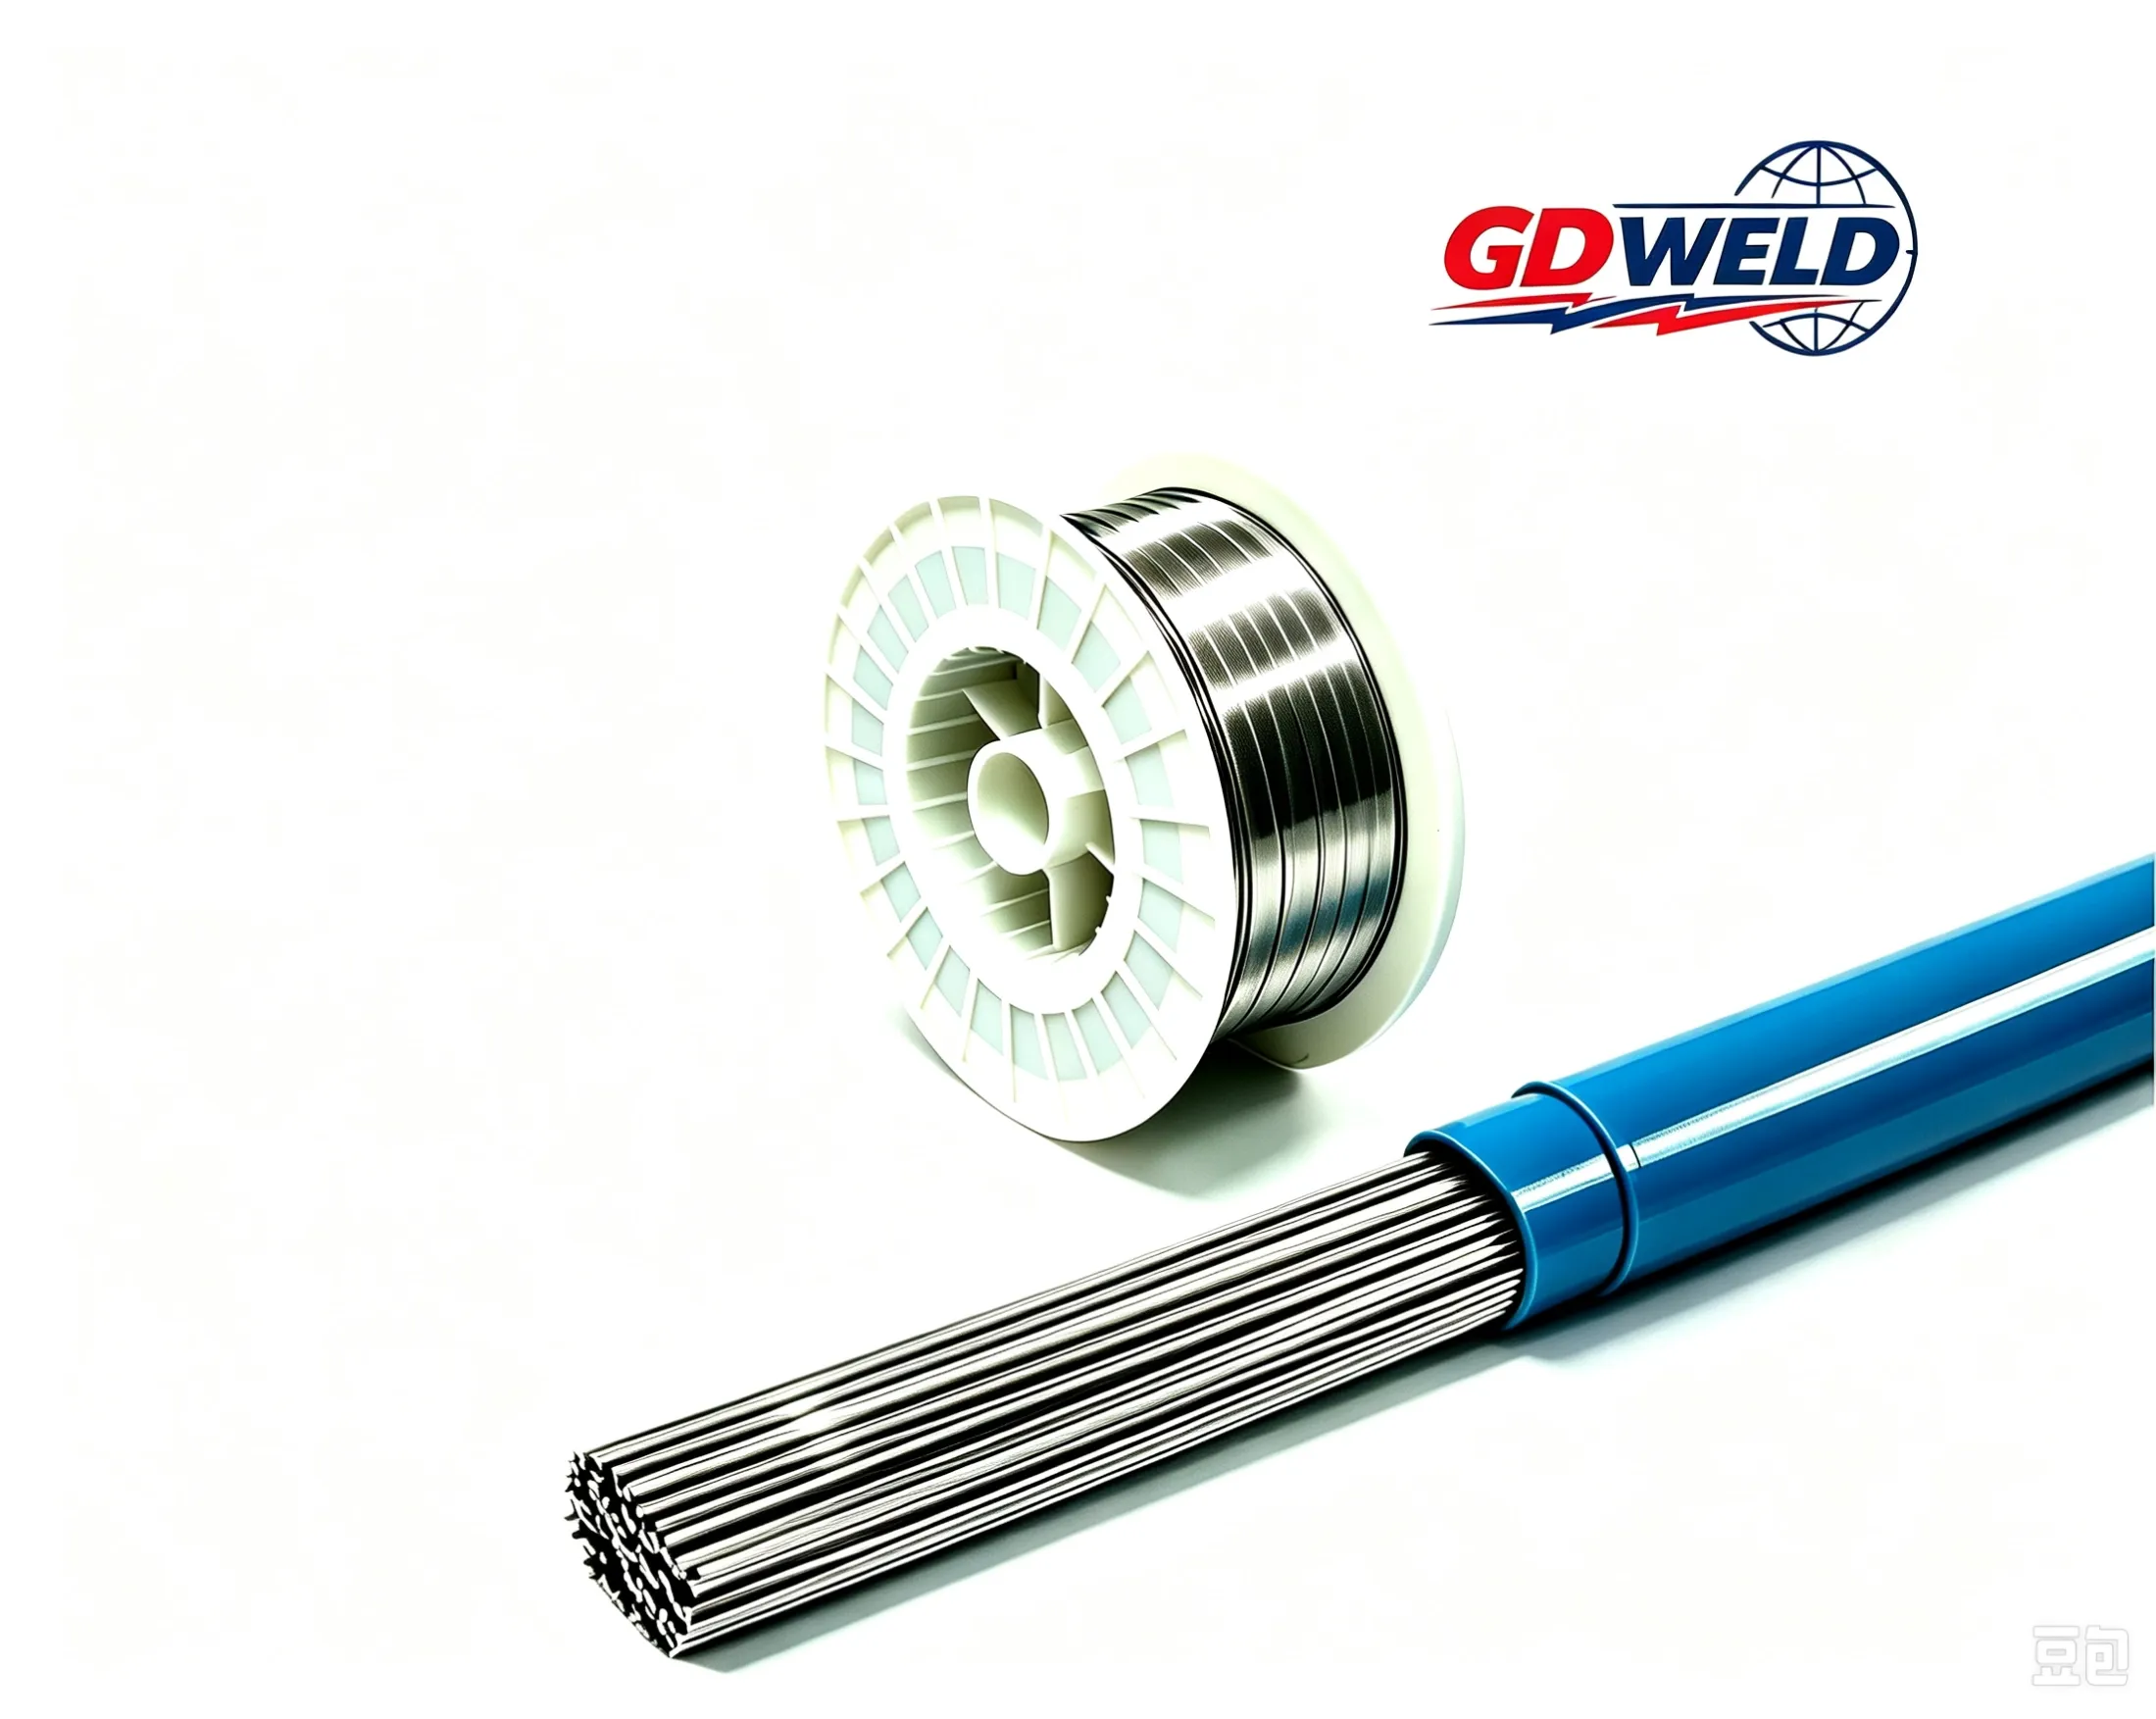
Welding Wire
ER312
ER312 is copper-coated high-alloy 29Cr-9Ni austenitic stainless steel solid wire, suitable for GMAW (MIG/MAG) and GTAW (TIG) welding.
ER312
ER312 is copper-coated high-alloy 29Cr-9Ni austenitic stainless steel solid wire, suitable for GMAW (MIG/MAG) and GTAW (TIG) welding.
Features
• Ultra-high ferrite content (25–40 FN), top-tier anti-hot-crack performance among stainless steel wires
• High chromium content provides good high-temperature oxidation resistance
• Weld deposit has high tensile strength and slight work hardening, certain wear resistance
• Stable arc, good molten pool spreadability, smooth forming for hard-to-weld steels
• Continuous service temperature: ≤420°C
Diameter & Packaging
MIG:0.8 / 1.0 / 1.2 / 1.6 mm 1KG Spool/5KG Spool / 15KG Spool
TIG:2.0 / 2.4 / 3.2 mm /4.0mm 5kg plastic tube
Welding Parameters
Polarity: DC+ (DCRP, Direct Current Reverse Polarity)
MIG / MAG
Shielding Gas: 98%Ar + 2%O₂
Gas Flow Rate: 20~25 L/min
Reference Current for common sizes:
Φ0.8mm:80–160 A
Φ1.0mm:110–220 A
Φ1.2mm:150–240 A
TIG (GTAW)
Shielding Gas: 99.99% High Purity Argon Gas Flow Rate: 10–16 L/min. Back purging is recommended for thick plates.
Base Metal Matching
For unknown composition steels, high-carbon steel, manganese steel, martensitic stainless steel & austenitic stainless steel dissimilar joints; transition buffer layer before hard surfacing.
Applications
Hard-to-weld alloy repair, armor plate, furnace high-temperature parts, dissimilar steel transition layer, tool steel repair, boiler pipe cladding.
⚠️ Not used for welding pure 304/316 stainless steel (excessive alloy, poor cost performance)
Welding Precautions
• Thoroughly remove oil, rust, scale and moisture from grooves before welding to avoid porosity. Use stainless steel-specific grinding wheels/wire brushes to prevent carbon steel contamination.
• Strictly control interpass temperature below 100°C to avoid brittle phases.
• Wind protection is required for outdoor welding if wind speed exceeds 1.0 m/s to avoid weld oxidation.
• Mainly used as transition buffer layer, not for final corrosion-resistant working layer.
ER312 vs ER309L
✅ ER312 (29Cr-9Ni): Ultimate anti-crack filler for unknown steel, high-carbon steel, difficult dissimilar joints
✅ ER309L (23Cr-13Ni): Conventional stainless-carbon steel dissimilar welding, routine surfacing cladding
Important Cautions
• Do not use pure CO₂ shielding gas; carbon pickup will reduce high-temperature oxidation resistance.
• Not applicable for long-term service under strong chloride corrosion.