Welding Electrode
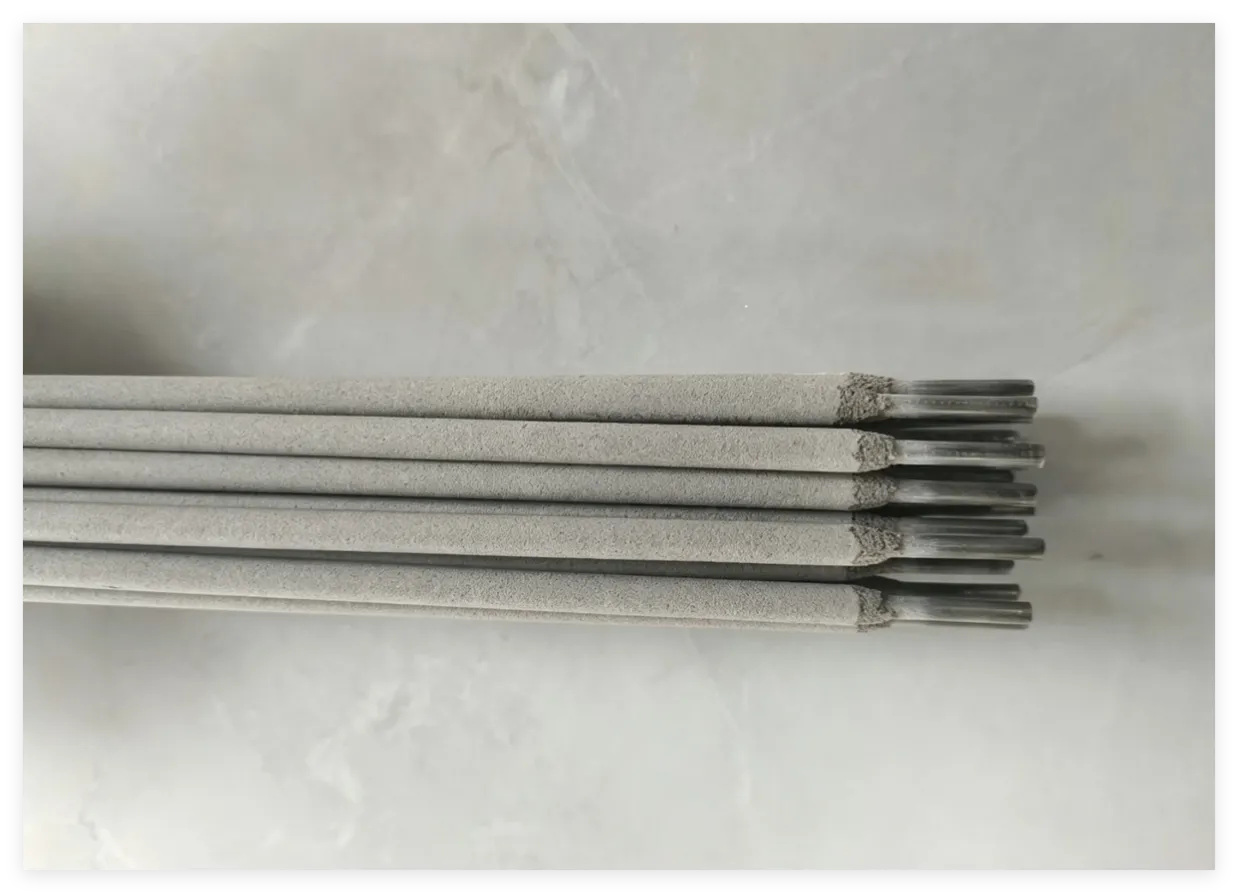
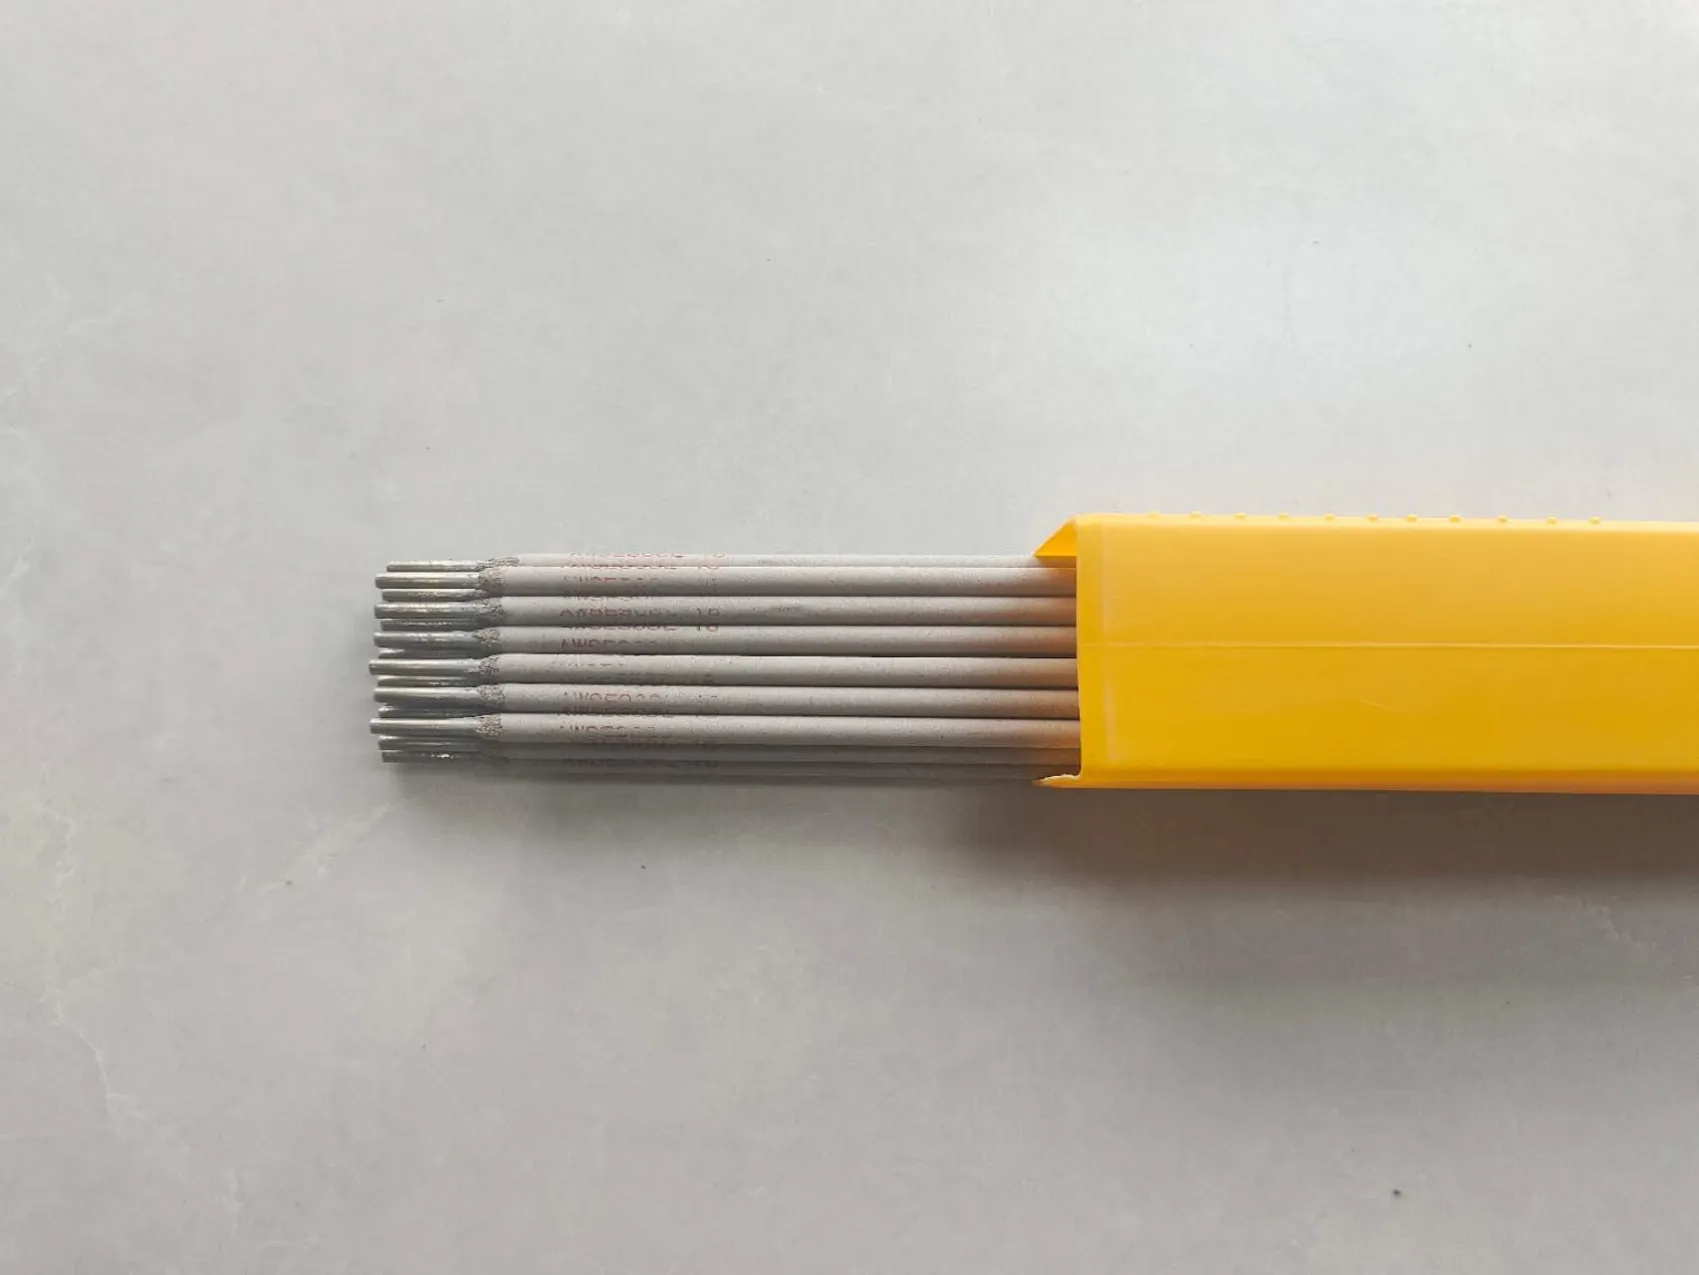
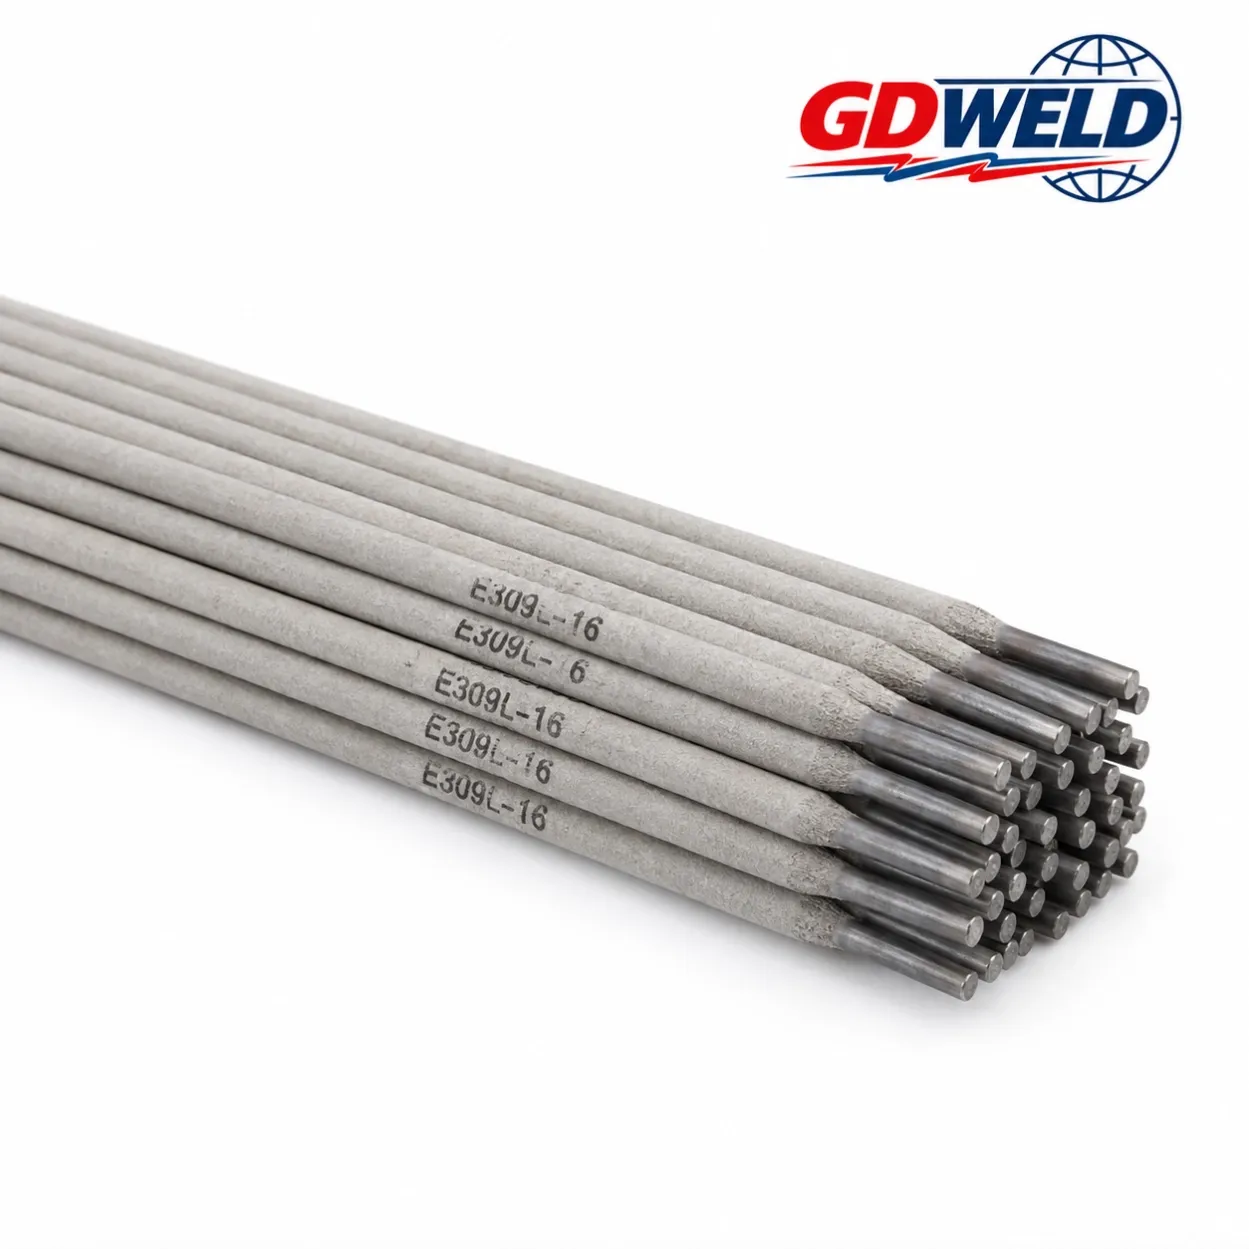
E309L-16 Stainless Steel Welding Electrode
E309L-16 is a low-carbon stainless steel welding electrode with a nominal 23% Cr–12% Ni weld-metal composition. It is commonly used for joining stainless steel to carbon steel and suitable low-alloy steel, as well as specified 309L-type welding and cladding applications.
Applications of E309L-16 Welding Electrode
E309L-16 is commonly selected when a low-carbon Cr-Ni weld deposit is specified for dissimilar-metal welding.
Typical applications include:
- Stainless steel to carbon steel welding: Joining 304/304L stainless steel to suitable carbon steel components.
- Stainless steel to low-alloy steel: Welding compatible dissimilar-metal joints under an approved welding procedure.
- 309L stainless steel fabrication: Welding components where E309L-16 is specified.
- Stainless steel cladding and buffer layers: Applying a stainless weld-metal layer over carbon or low-alloy steel.
- Industrial maintenance and repair: Repairing suitable dissimilar-metal joints in fabricated equipment and process systems.
For applications that require molybdenum-bearing weld metal, compare the specified chemistry with our E309MoL-16 Stainless Steel Welding Electrode. The two classifications are not interchangeable in every application.
For cladding and overlay welding, base-metal dilution can affect the final weld-metal chemistry. Confirm the required number of layers, corrosion performance, service conditions, and qualified welding procedure before selecting the electrode.
Chemical Composition
The following table lists commonly referenced AWS A5.4 E309L-16 classification limits. Confirm the applicable standard edition and the supplied product's TDS or material test certificate (MTC).
Element | Classification Limit (wt.%) |
|---|---|
Carbon (C) | ≤0.04 |
Manganese (Mn) | 0.5–2.5 |
Silicon (Si) | ≤1.00 |
Chromium (Cr) | 22.0–25.0 |
Nickel (Ni) | 12.0–14.0 |
Molybdenum (Mo) | ≤0.75 |
Copper (Cu) | ≤0.75 |
Phosphorus (P) | ≤0.04 |
Sulfur (S) | ≤0.03 |
These are classification limits, not guaranteed batch analysis values. Actual chemical composition should be confirmed against the manufacturer's documentation.
Mechanical Properties
Property | AWS Classification Minimum |
|---|---|
Tensile Strength | ≥520 MPa |
Elongation | ≥30% |
These figures represent classification requirements, not actual batch test results. Refer to the applicable product documentation for certified results.
Welding Characteristics
E309L-16 is a covered electrode for shielded metal arc welding (SMAW). Its low-carbon deposit helps limit carbide precipitation, but corrosion resistance depends on the final weld-metal chemistry and service environment.
- Current: AC or DCEP, subject to the manufacturer's instructions.
- Common diameters: 2.5 mm, 3.2 mm, 4.0 mm, and 5.0 mm, depending on availability.
- Welding parameters: Follow the manufacturer's TDS and the qualified welding procedure.
- Before welding: Check base-metal grades, dilution, operating temperature, corrosion requirements, and applicable fabrication codes.
E309L-16 vs. E309-16 vs. E309MoL-16
Electrode | Main Difference | Selection Consideration |
|---|---|---|
E309L-16 | Low-carbon Cr-Ni weld metal | Specified dissimilar-metal joints and selected cladding applications |
E309-16 | Standard-carbon Cr-Ni weld metal | Applications where the standard-carbon classification is specified and suitable |
E309MoL-16 | Low-carbon Cr-Ni-Mo weld metal | Applications requiring molybdenum-bearing weld metal |
For higher-chromium stainless steel applications, E310-16 Stainless Steel Welding Electrode is a different alloy option and should only be selected when its composition meets the application requirements.
Choose the electrode according to the specified weld-metal chemistry, corrosion requirements, service conditions, and qualified welding procedure—not by classification name alone.
Classification and Supply
- AWS classification: A5.4 E309L-16
- ASME classification: SFA-5.4 E309L-16, where applicable certification is provided
- EN ISO classification: EN ISO 3581-A; confirm the complete designation and suffix against the product certificate
- Welding process: SMAW
- Product type: Low-carbon Cr-Ni stainless steel covered electrode
- Available diameters: Subject to the current product range
GD WELD supplies stainless steel welding consumables for industrial fabrication, maintenance, and dissimilar-metal welding. For a quotation, provide the required AWS classification, diameter, base materials, application, quantity, and certification requirements.
Tags
E309L-16 welding electrode, E309L-16 electrode, E309L-16 welding rod, AWS A5.4 E309L-16, low carbon stainless steel electrode, 309L stainless steel welding electrode, stainless steel to carbon steel welding electrode, dissimilar metal welding electrode, 23Cr 12Ni welding electrode, stainless steel cladding electrode, buffer layer welding electrode, E309L-16 supplier