Welding Electrode
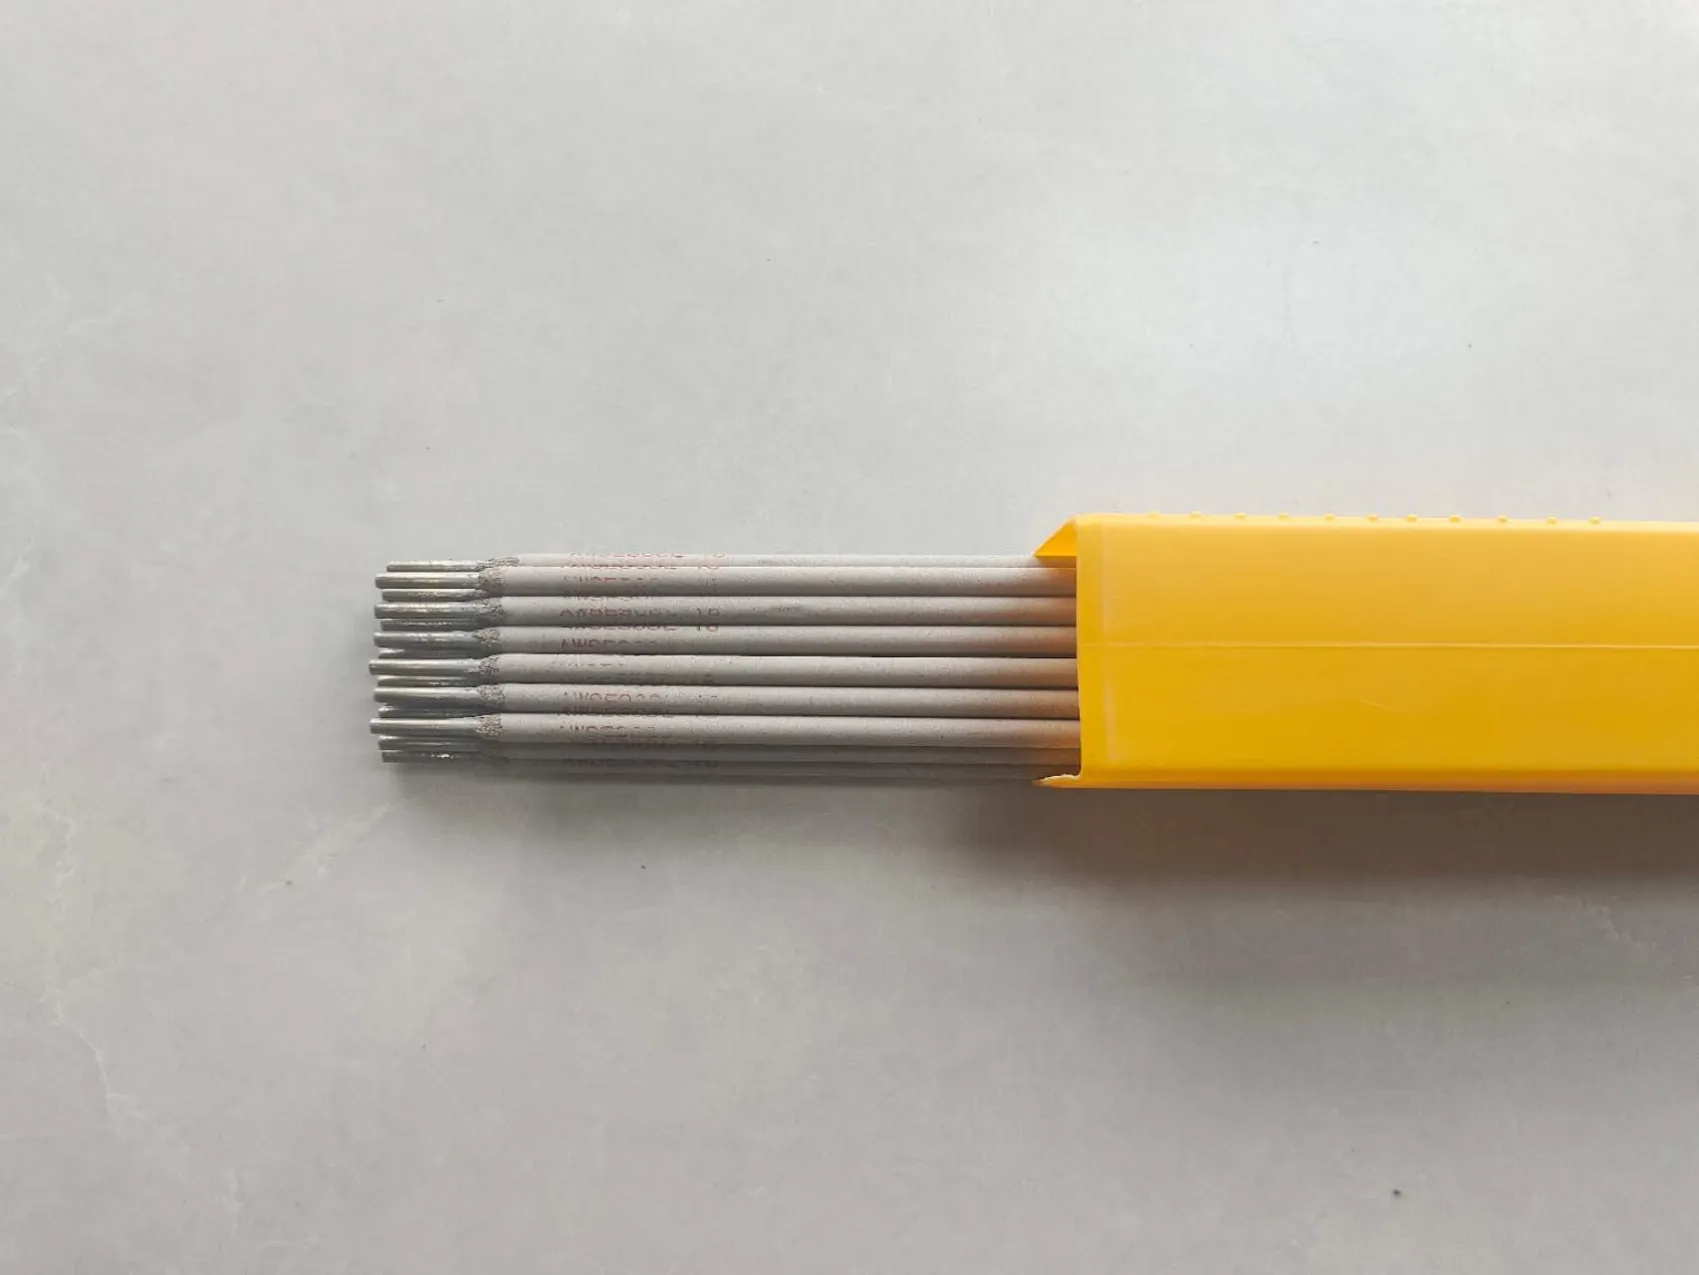
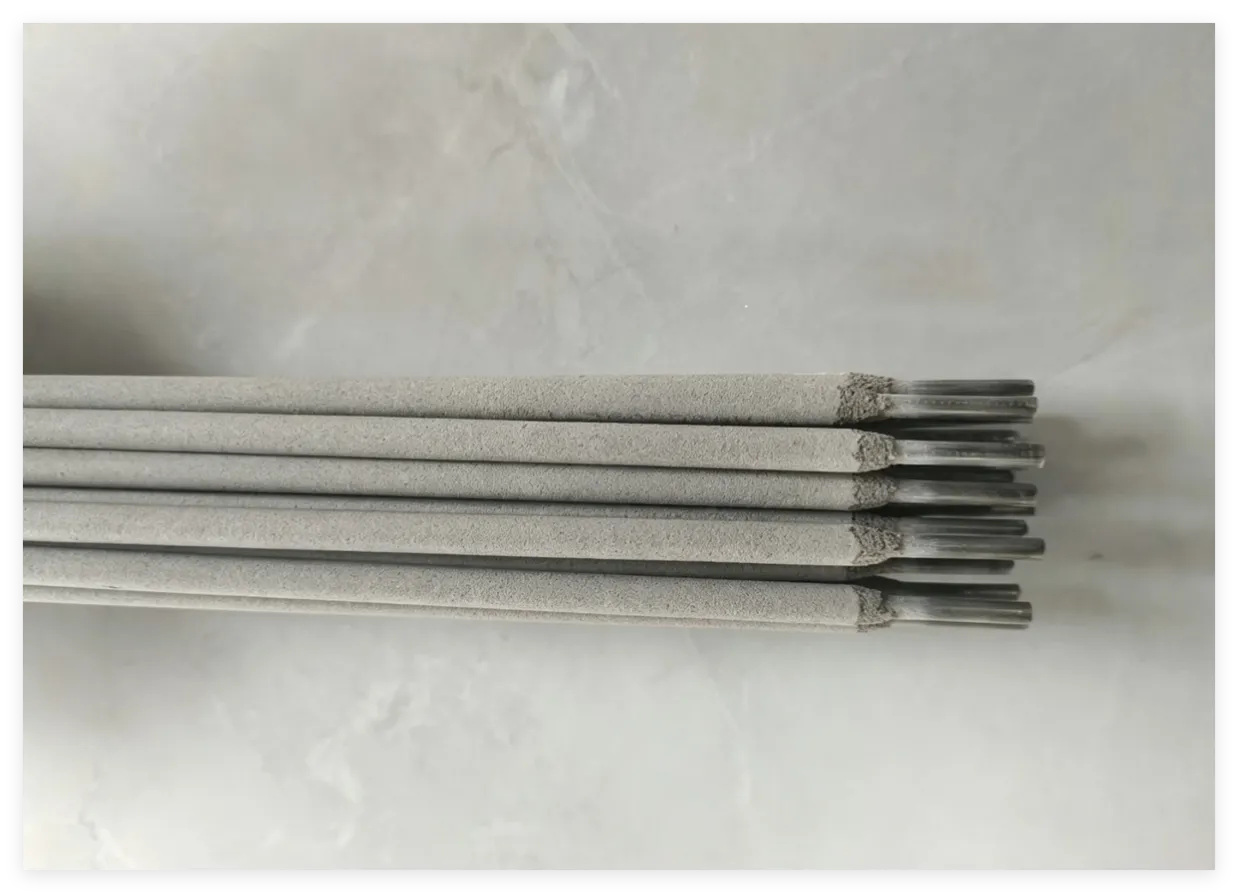
E385-16 904L Stainless Steel Welding Electrode
E385-16 is a high-alloy austenitic stainless steel welding electrode designed primarily for 904L stainless steel (UNS N08904 / EN 1.4539). Its low-carbon Cr-Ni-Mo-Cu weld metal provides high corrosion resistance in sulfuric acid, phosphoric acid, chloride-containing and other aggressive environments. It is commonly used in chemical processing, acid handling, process piping, tanks, heat exchangers and other corrosion-resistant industrial applications.
E385-16 for 904L Stainless Steel
E385-16 is formulated for 904L and similar high-alloy Cr-Ni-Mo-Cu stainless steels.
Base Material | Identification |
|---|---|
904L stainless steel | UNS N08904 |
904L stainless steel | EN 1.4539 |
Similar high-alloy stainless steels | Subject to qualified WPS |
The fully austenitic weld metal provides good corrosion resistance and compatibility with 904L-type materials.
Typical Applications
E385-16 is selected when conventional 304L, 316L or 309L electrodes may not provide sufficient corrosion resistance.
- Sulfuric and phosphoric acid equipment
- Chemical processing vessels and piping
- Acid storage and handling systems
- Heat exchangers, pumps and valves
- Chloride-containing service environments
- Selected stainless steel cladding and repair welding
Why Choose E385-16?
The weld metal has a nominal composition of approximately 20Cr–25Ni–5Mo–1.5Cu. The combination of chromium, nickel, molybdenum and copper provides high corrosion resistance for demanding chemical service.
Key features include:
- Designed for 904L stainless steel
- Fully austenitic weld metal
- Low-carbon Cr-Ni-Mo-Cu composition
- High resistance to sulfuric and phosphoric acid environments
- Improved resistance to pitting and crevice corrosion
Chemical Composition
Reference composition for E385-16:
Element | Reference Range |
|---|---|
C | ≤0.03% |
Mn | 1.0–2.5% |
Si | ≤0.90% |
Cr | 19.5–21.5% |
Ni | 24.0–26.0% |
Mo | 4.2–5.2% |
Cu | 1.2–2.0% |
P | ≤0.03% |
S | ≤0.02% |
Actual chemistry may vary by manufacturer and batch. The applicable TDS and MTC should be checked for project-specific requirements.
Mechanical Properties & Welding
Property | Reference Requirement |
|---|---|
Tensile Strength | ≥520 MPa |
Elongation | ≥30% |
Weld Metal Structure | Fully austenitic |
E385-16 is a coated SMAW electrode suitable for AC or DCEP.
Electrode Diameter | Typical Current |
|---|---|
2.5–2.6 mm | 55–85 A |
3.2 mm | 70–120 A |
4.0 mm | 100–150 A |
5.0 mm | 140–180 A |
These are typical commercial ranges, not AWS requirements. Follow the manufacturer's TDS and qualified WPS. Preheating is generally not required for 904L; heat input and interpass temperature should be controlled during welding.
E385-16 Classification
- AWS A5.4: E385-16
- ASME SFA-5.4: E385-16
- EN ISO 3581-A: E 20 25 5 Cu N L R
- Process: SMAW
- Polarity: AC / DCEP
- Weld Metal: Fully austenitic Cr-Ni-Mo-Cu
E385-16 vs E383-16
Electrode | Primary Material Focus |
|---|---|
E385-16 | 904L / UNS N08904 / EN 1.4539 |
E383-16 | Alloy 825 / Alloy 28-type materials |
For 904L welding, E385-16 is the more directly targeted electrode. E383-16 is more closely associated with Alloy 825 and Alloy 28 applications.
Supply from GD WELD
GD WELD supplies E385-16 904L stainless steel welding electrodes for international industrial procurement, with different diameters, packaging and technical documentation available according to project requirements.
Tags
E385-16, E385-16 welding electrode, E385-16 electrode, AWS E385-16, 904L welding electrode, 904L stainless steel electrode, UNS N08904 welding electrode, EN 1.4539 welding electrode, high alloy stainless steel electrode, super austenitic stainless steel electrode, sulfuric acid welding electrode, phosphoric acid welding electrode, acid resistant welding electrode, Cr-Ni-Mo-Cu welding electrode
Internal Links
👉 Internal Link 1: Anchor text: E383-16 nickel-based welding electrode
👉 Internal Link 2: Anchor text: E320-16 stainless steel welding electrode
👉 Internal Link 3: Anchor text: E309MoL-16 stainless steel welding electrode