General Welding Consumables
E7014
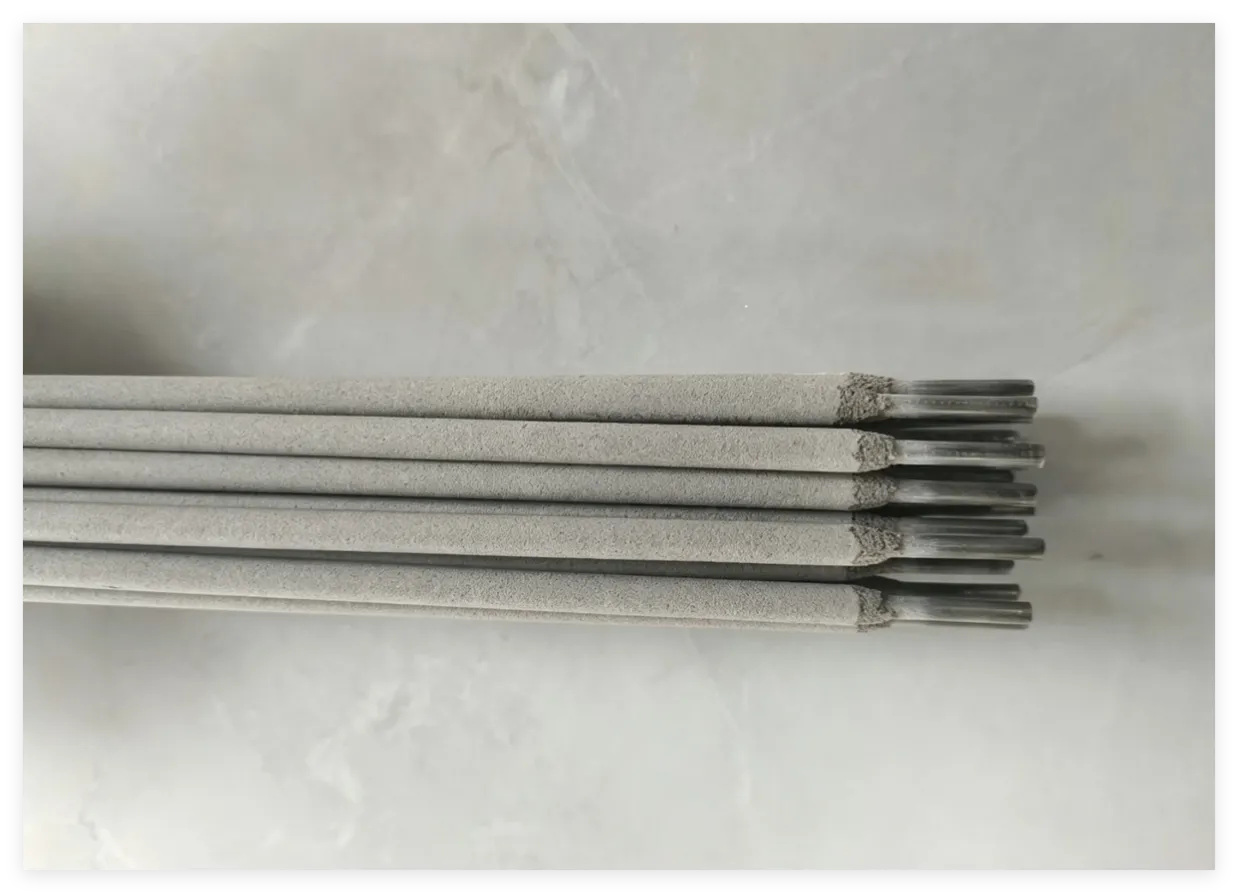
E7014 is a carbon steel SMAW electrode with rutile iron powder coating. Iron powder in the coating delivers higher deposition efficiency than E6013 for improved welding productivity. Rated at 70ksi tensile strength, it works with both AC and DC and is easy to operate, ideal for efficient welding of medium-thick carbon steel.
E7014 is a carbon steel SMAW electrode with rutile iron powder coating. Iron powder in the coating delivers higher deposition efficiency than E6013 for improved welding productivity. Rated at 70ksi tensile strength, it works with both AC and DC and is easy to operate, ideal for efficient welding of medium-thick carbon steel.
Coating Type: Rutile iron powder type
Current Polarity: AC / DC+ / DC- available
Welding Process: SMAW, all-position welding
Comparison: E6013 vs E7014
E6013: Rutile high-titania potassium type, no iron powder, 60ksi strength, average deposition efficiency. Suitable for thin plates, cosmetic welding and light structures.
E7014: Rutile iron powder type, 70ksi strength, high deposition efficiency. Suitable for medium-thick plates, high-efficiency fillet welds and load-bearing steel structures.
E7014 Features
· Stable soft arc with low spatter, easy ignition and re-ignition.
· Iron powder coated for higher deposition efficiency, ideal for mass fillet welds.
· Slag easy to remove with attractive weld beads.
· Compatible with AC and DC power sources for all-position welding.
· Higher strength grade than E6013 for load-bearing steel structures.
· Note: Moderate penetration, not suitable for vertical-down pipeline root welding; poor tolerance to heavy rust and oil contamination.
E7014 Welding Tips
· Usable with AC, DC+ or DC-.
· Keep short arc; long arc may cause porosity and slag inclusion.
· Remove oil, moisture and heavy rust on groove area.
Common Defects
· Porosity: damp electrode, excessive arc length, surface contaminants
· Slag inclusion: improper travel technique, insufficient inter-pass cleaning
· Lack of fusion: insufficient current, fast travel speed
Applicable Base Metals
Low carbon steel and mild low alloy steel: Q235, Q355, S235JR, S275JR, A106 Gr.B
Typical Applications
Building steel structures, machinery frames, vehicle parts, storage tanks, mass production fillet welds and equipment maintenance.