General Welding Consumables
E7015
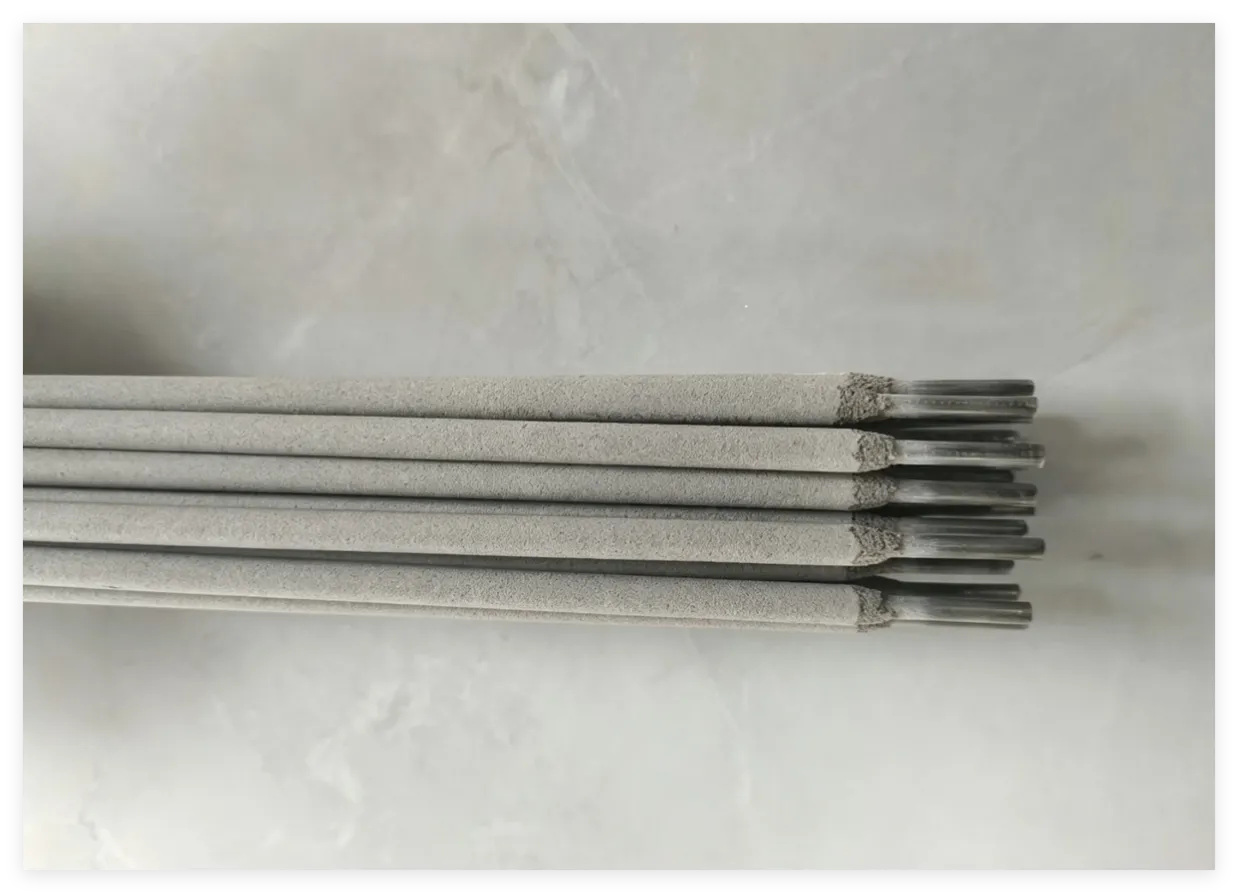
E7015 is a carbon steel SMAW electrode with low-hydrogen sodium coating (basic low-hydrogen type). The weld metal has low diffusible hydrogen, outstanding ductility and low-temperature toughness with strong resistance to cold cracking. It is ideal for critical restrained thick-plate load-bearing structures.
E7015 is a carbon steel SMAW electrode with low-hydrogen sodium coating (basic low-hydrogen type).
The weld metal has low diffusible hydrogen, outstanding ductility and low-temperature toughness with strong resistance to cold cracking. It is ideal for critical restrained thick-plate load-bearing structures.
Coating Type: Low-hydrogen sodium type
Current Polarity: DC+ (DC reverse polarity) Only
Welding Process: SMAW, all-position welding
Comparison E7014 / E7015 / E7018
E7014: Rutile iron powder type, AC/DC compatible. Good operating performance & nice weld appearance. Medium strength for general steel structures and fillet welds. Acid coating, poor crack resistance.
E7015: Low-hydrogen sodium type, DC+ only. Low hydrogen, high toughness and superior crack resistance. For critical pressure vessels, bridges and shipworks. No iron powder, average deposition efficiency; AC unavailable.
E7018: Low-hydrogen potassium iron powder type, AC/DC+ compatible. Low hydrogen plus iron powder for higher efficiency. Suitable for heavy-duty structures and general low-hydrogen applications. Works with both AC and DC power.
E7015 Features
· Stiff & stable arc with low spatter, good resistance to magnetic arc blow. Slag easy to remove and uniform weld bead.
· Low-hydrogen coating provides excellent crack resistance and low-temperature toughness.
⚠ Only DC+ available, incompatible with AC welders. Sensitive to surface contaminants; electrodes require high-temperature baking. Not recommended for thin plate & cosmetic welding.
E7015 Welding Tips
· Only DC+ reverse polarity can be adopted.
· Use short arc & narrow bead technique.
· Fully clean oil, moisture and rust on groove area.
E7015 Common Defects
Porosity: damp electrode, insufficient baking, long arc, surface impurities
Cold cracking: moisture absorption, inadequate preheat, fast cooling rate
Slag inclusion: improper travel speed, insufficient inter-pass cleaning
E7015 Baking Instruction
Bake electrodes at 350~380℃ for 60 mins before use. Keep warm at 100~150℃ after baking. Rebaking ≤2 times.
E7015 Applicable Base Metals
Low carbon steel & mild low alloy steel: Q235, Q355 (16Mn), S235JR, S275JR, A106 Gr.B, Ship Grade A/B/D steel plates
Typical Applications
Pressure vessels, bridges, heavy machinery, ship components, thick load-bearing steel structures, critical high-stress welds