General Welding Consumables
E7018
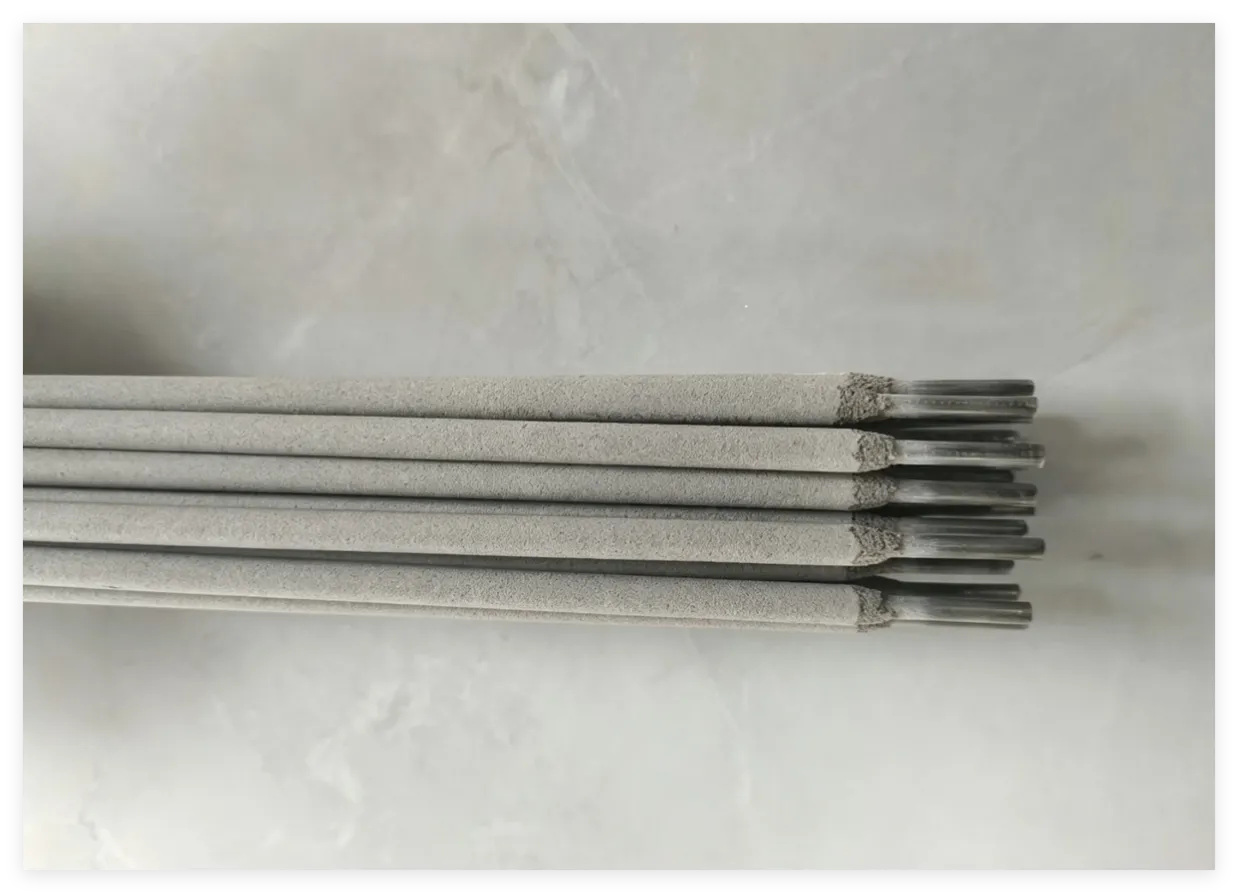
E7018 is a carbon steel SMAW electrode with low-hydrogen potassium iron powder coating (basic low-hydrogen type). Compatible with AC and DC+.
E7018 is a carbon steel SMAW electrode with low-hydrogen potassium iron powder coating (basic low-hydrogen type). Compatible with AC and DC+.
Iron powder in coating offers higher deposition efficiency than E7016. Weld metal features low diffusible hydrogen, excellent low-temperature toughness and strong cold crack resistance. It balances productivity and weld quality for various critical load-bearing steel structures.
Coating Type: Low-hydrogen potassium iron powder type
Current Polarity: AC / DC+ (DC reverse polarity) available
Welding Process: SMAW, all-position welding
Comparison: E7015 / E7016 / E7018
E7015: Low-hydrogen sodium type, DC+ only. Excellent toughness, no iron powder, average efficiency, AC unavailable.
E7016: Low-hydrogen potassium type, AC/DC+ compatible. Low-hydrogen without iron powder, medium efficiency for field AC welding.
E7018: Low-hydrogen potassium iron powder type, AC/DC+ compatible. With iron powder for highest deposition efficiency, combining low-hydrogen toughness and high productivity.
E7018 Features
· Stable soft arc with moderate spatter and good slag removability.
· Basic low-hydrogen formula provides excellent crack resistance and high impact toughness.
· Iron powder added for higher deposition efficiency than E7015 & E7016. AC/DC+ compatible for all-position welding, convenient for field AC welding sites.
· Note: High-temperature baking is required. Sensitive to oil and rust contaminants.
E7018 Welding Tips
· Compatible with AC or DC+.
· Adopt short arc and narrow bead welding.
· Thoroughly clean oil, moisture and heavy rust on welding groove.
E7018 Common Defects
Porosity: damp electrode, insufficient baking, long arc, surface contaminants
Cold cracking: electrode moisture absorption, inadequate preheat, fast cooling rate
Slag inclusion: excessive weaving width, incomplete inter-pass cleaning
E7018 Applicable Base Metals
Low carbon steel & mild low alloy steel: Q235, Q355 (16Mn), S235JR, S275JR, A106 Gr.B, Ship Grade A/B/D steel plates
Typical Applications
Pressure vessels, bridges, heavy machinery, storage tanks, lifting equipment, critical thick-plate welds and field construction.