Heat Resistant & Cr-Mo
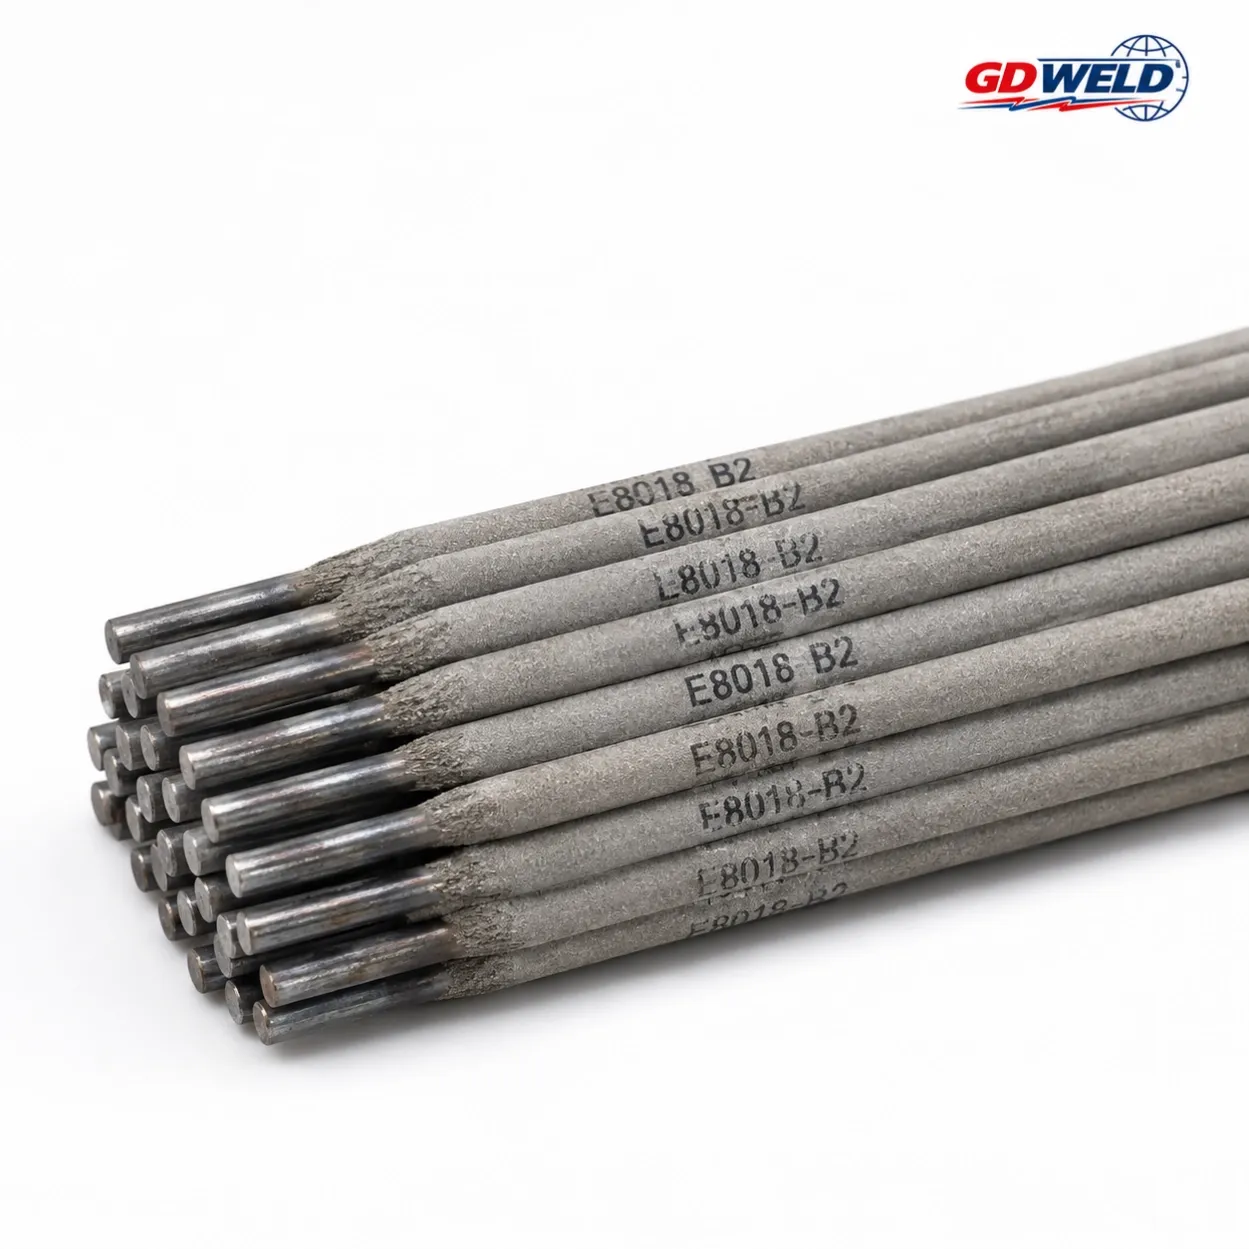
E8018-B2 Cr-Mo Welding Electrode
E8018-B2 is a low-hydrogen Cr-Mo welding electrode classified under AWS A5.5 for 1.25Cr-0.5Mo heat-resistant low-alloy steels. It is commonly selected for P11, P12, T11 and T12 materials used in boilers, steam piping, pressure vessels and petrochemical equipment. For P11/P12 applications requiring a low-hydrogen SMAW electrode, E8018-B2 provides a matching 1.25Cr-0.5Mo weld deposit for elevated-temperature service.
E8018-B2 for P11 & P12 Steel
The primary application range is 1.25Cr-0.5Mo Cr-Mo steel, including:
- ASTM A335 P11 / P12
- ASTM A213 T11 / T12
- ASTM A387 Grade 11 / 12
- ASTM A182 F11 / F12
- Similar 1.25Cr-0.5Mo steels
For P22, P91 or P92 materials, select the corresponding Cr-Mo electrode according to the base-metal specification and qualified WPS.
Technical Data
Chemical Composition
Typical AWS classification limits for deposited weld metal:
Element | Requirement |
|---|---|
C | 0.05–0.12% |
Mn | ≤0.90% |
Si | ≤0.80% |
Cr | 1.00–1.50% |
Mo | 0.40–0.65% |
P | ≤0.030% |
S | ≤0.030% |
Actual chemistry may vary by manufacturer and production batch. Refer to the supplied TDS/MTC for project-specific values.
Mechanical Properties
Property | AWS Minimum |
|---|---|
Tensile Strength | ≥550 MPa |
Yield Strength | ≥460 MPa |
Elongation | ≥19% |
Charpy impact toughness is not specified as a universal minimum requirement for the basic E8018-B2 classification. Additional impact requirements may apply to specific products or projects.
Applications
E8018-B2 welding electrodes are used for:
- P11/P12 steam and process piping
- Boiler tubes and headers
- Pressure vessels and heat exchangers
- Power plant Cr-Mo components
- Refinery and petrochemical equipment
- High-temperature Cr-Mo steel fabrication and repair
When to Choose E8018-B2
Choose E8018-B2 when the base material is a 1.25Cr-0.5Mo Cr-Mo steel such as P11 or P12 and the welding procedure requires SMAW.
For higher-alloy Cr-Mo steels such as P22, P91 or P92, use the electrode specified for the applicable material and qualified WPS.
Welding Information
Process: SMAW
Polarity: AC or DCEP
Coating: Low-hydrogen iron-powder type
Electrode Diameter | Typical Current |
|---|---|
2.5 mm | 60–110 A |
3.2 mm | 85–160 A |
4.0 mm | 110–210 A |
5.0 mm | 160–240 A |
Preheat, interpass temperature, heat input and PWHT should follow the base material, thickness, applicable code and qualified WPS.
E8018-B2 vs ER80S-B2
Both consumables are used for 1.25Cr-0.5Mo / P11-P12 steel, but they are designed for different welding processes:
| E8018-B2 | ER80S-B2 |
|---|---|---|
Product Type | Welding Electrode | Solid Welding Wire |
Process | SMAW | GTAW / GMAW |
Typical Application | P11/P12 | P11/P12 |
Choose E8018-B2 when manual stick welding is required; ER80S-B2 is intended for GTAW or GMAW applications.
Classification
- AWS A5.5: E8018-B2
- ASME SFA-5.5: E8018-B2
- Process: SMAW
- Electrode Type: Low-hydrogen iron-powder coated
- Typical Weld Metal: 1.25Cr-0.5Mo
- Polarity: AC / DCEP
E8018-B2 H4R should only be stated when the supplied product is certified to the H4R designation.
GD WELD Supply
GD WELD supplies E8018-B2 Cr-Mo welding electrodes for P11/P12 piping, boilers, pressure equipment, power generation and petrochemical applications. Different diameters, packaging and technical documentation are available for industrial procurement.
Tags
E8018-B2, E8018-B2 welding electrode, P11 welding electrode, P12 welding electrode, 1.25Cr-0.5Mo welding electrode, Cr-Mo welding electrode, low hydrogen welding electrode, heat resistant steel electrode
Internal Links
👉 Internal Link: Anchor text: ER80S-B2 Cr-Mo welding wire