Heat Resistant & Cr-Mo
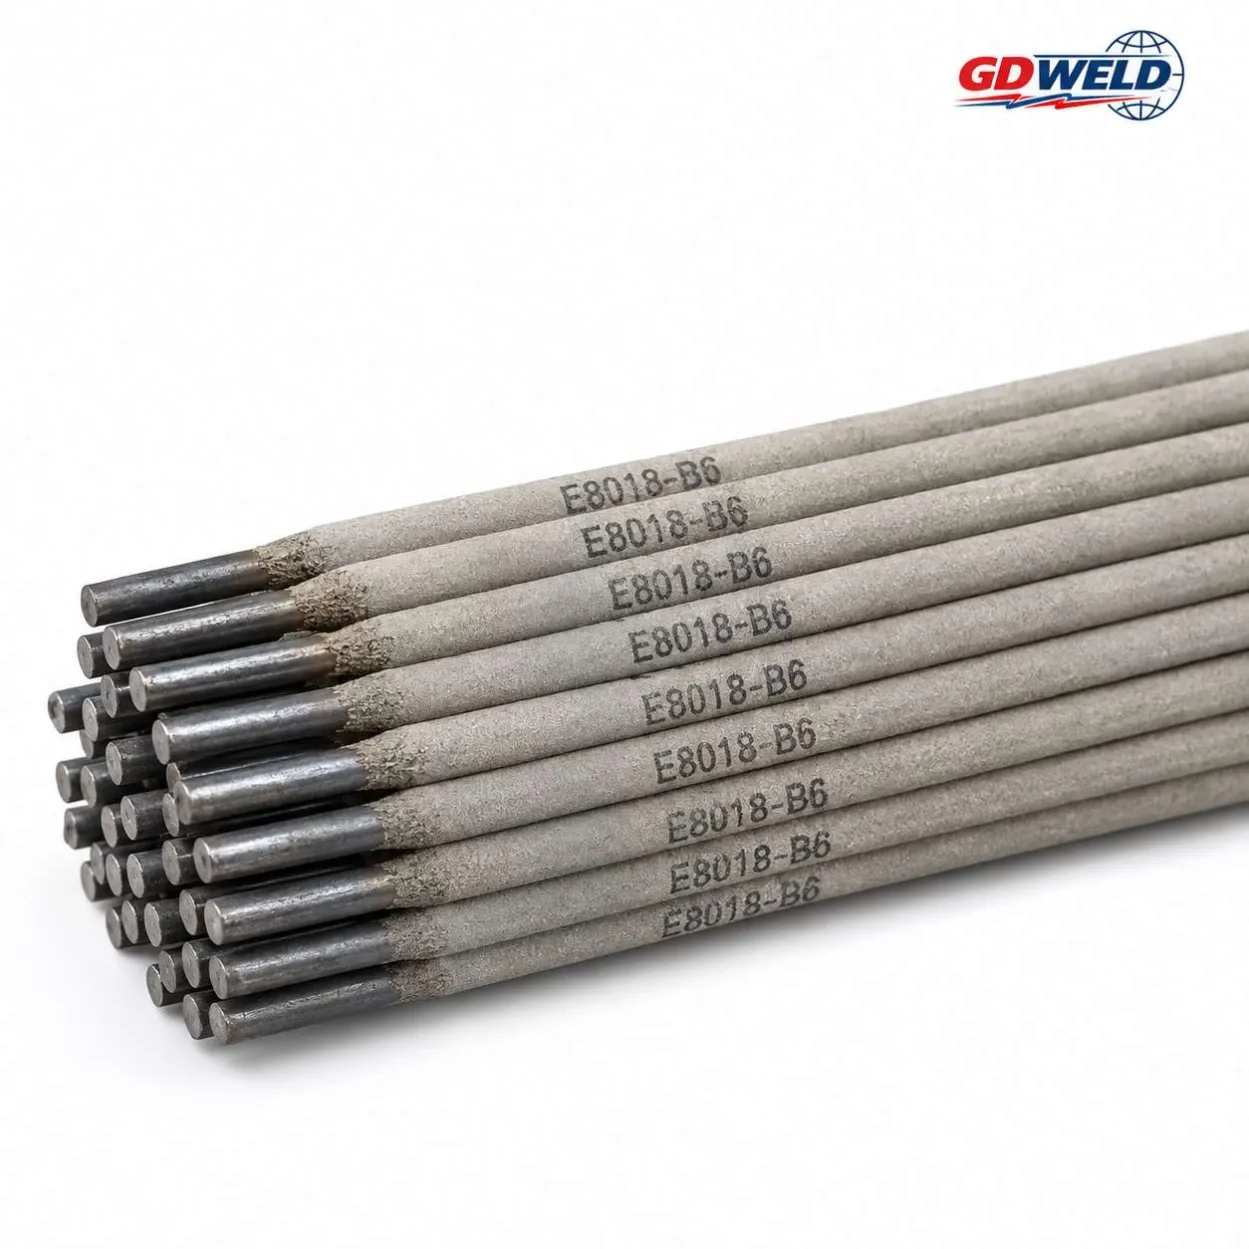
E8018-B6 Cr-Mo Welding Electrode for P5 and T5 Steel
E8018-B6 is a low-hydrogen Cr-Mo welding electrode for 5Cr-0.5Mo heat-resistant steel. It is mainly used for ASTM A335 P5, A213 T5 and similar Cr-Mo steels in refinery piping, petrochemical equipment, boilers, pressure vessels and high-temperature process systems. Classified under AWS A5.5/A5.5M E8018-B6, the electrode produces weld metal with a controlled chromium-molybdenum alloy system for matching 5Cr-0.5Mo steel. E502 is an older classification designation associated with this electrode ty
E8018-B6 for P5 and T5 Steel
E8018-B6 welding electrode is commonly selected for:
- ASTM A335 P5/P5b pipe
- ASTM A213 T5/T5b tube
- ASTM A387 Grade 5 plate
- ASTM A182 F5/F5a forgings
- ASTM A217 C5 castings
- Similar 5Cr-0.5Mo creep-resistant steels
The P5 welding electrode and T5 welding electrode search terms are closely related to E8018-B6 because the consumable is designed for steels with a matching Cr-Mo alloy system.
Typical applications include oil refineries, petrochemical plants, boilers, heat exchangers, pressure vessels and high-temperature piping. Commercial E8018-B6 products are also used where resistance to hydrogen attack, sulfidation and elevated-temperature service is required.
E8018-B6 Chemical Composition
AWS classification requirements for undiluted weld metal include:
Element | AWS Requirement, wt.% |
|---|---|
C | 0.05–0.10 |
Mn | ≤1.00 |
Si | ≤0.90 |
P | ≤0.03 |
S | ≤0.03 |
Ni | ≤0.40 |
Cr | 4.00–6.00 |
Mo | 0.45–0.65 |
The 4–6% Cr and 0.45–0.65% Mo alloy system is the defining chemistry of E8018-B6. These are classification limits, not a guaranteed analysis for every commercial electrode. Actual deposited chemistry should be confirmed by the manufacturer's TDS/MTC.
Mechanical Properties of E8018-B6
AWS A5.5/A5.5M minimum requirements include:
Property | Minimum Requirement |
|---|---|
Tensile Strength | ≥550 MPa (80 ksi) |
Yield Strength | ≥460 MPa (67 ksi) |
Elongation | ≥19% |
Actual weld-metal results can be higher depending on electrode formulation, welding conditions and PWHT. Commercial E8018-B6 products commonly report values above these classification minimums.
Welding P5/T5 Steel with E8018-B6
E8018-B6 is a basic low-hydrogen SMAW electrode. AC or DCEP/DC+ may be specified depending on the product design.
Typical Welding Current
Electrode Diameter | Typical Current |
|---|---|
2.5 mm | 60–100 A |
3.2 mm | 80–140 A |
4.0 mm | 120–190 A |
5.0 mm | 150–240 A |
These are commercial reference ranges rather than AWS mandatory welding parameters. Manufacturer recommendations vary by electrode size and formulation.
Preheat and PWHT
P5/T5 welding requires controlled preheat, interpass temperature and post-weld heat treatment (PWHT) to manage hydrogen cracking and weld-metal/HAZ properties.
Commercial procedures may use approximately 200–300°C preheat/interpass temperature and PWHT around 740–750°C, depending on material thickness, applicable code and qualified WPS. For example, commercial E8018-B6 products specify preheat around 250°C and PWHT around 740–750°C.
These are procedure or manufacturer references, not universal AWS requirements.
E8018-B6 vs E8018-B2 and E9018-B3
Choosing a Cr-Mo electrode by strength class alone is not enough. The consumable should also match the base-metal alloy system.
| E8018-B2 | E8018-B6 | E9018-B3 |
|---|---|---|---|
Typical steel | P11 / T11 | P5 / T5 | P22 / T22 |
Main alloy system | Cr-Mo | 5Cr-0.5Mo | 2.25Cr-1Mo |
Strength class | 80 ksi | 80 ksi | 90 ksi |
Main application | 1.25Cr-0.5Mo steel | 5Cr-0.5Mo steel | 2.25Cr-1Mo steel |
E8018-B6 should be selected when the specified base material requires a 5Cr-0.5Mo consumable. E8018-B2 and E9018-B3 should not be treated as automatic substitutes. Industry product lineups likewise distinguish E8018-B6 specifically for Grade 5 / 5Cr steel.
Applications and Supply
E8018-B6 welding electrodes are commonly used for:
- P5 and T5 Cr-Mo pipe welding
- Oil refinery piping
- Petrochemical process equipment
- Boilers and heat exchangers
- Pressure vessels
- High-temperature Cr-Mo fabrication and repair
AWS: A5.5/A5.5M E8018-B6
ASME: SFA-5.5 E8018-B6, when certified
Process: SMAW
Electrode Type: Basic low-hydrogen covered electrode
Typical Sizes: 2.5, 3.2, 4.0 and 5.0 mm
GD WELD supplies E8018-B6 Cr-Mo welding electrodes for P5/T5 and similar 5Cr-0.5Mo steels. TDS, MTC, electrode sizes, packaging and project-specific certification can be confirmed according to customer requirements.
Tags
E8018-B6 welding electrode, E8018-B6 electrode, P5 welding electrode, T5 welding electrode, 5Cr-0.5Mo welding electrode, Cr-Mo welding electrode, P5 welding consumable, T5 welding consumable, A335 P5 welding electrode, A213 T5 welding electrode, A387 Grade 5 welding electrode, E502 welding electrode
Internal Links
👉 Internal Link 1: Anchor text: E8018-B2 welding electrode for P11 steel
👉 Internal Link 2: Anchor text: E9018-B3 welding electrode for P22 steel