Heat Resistant & Cr-Mo
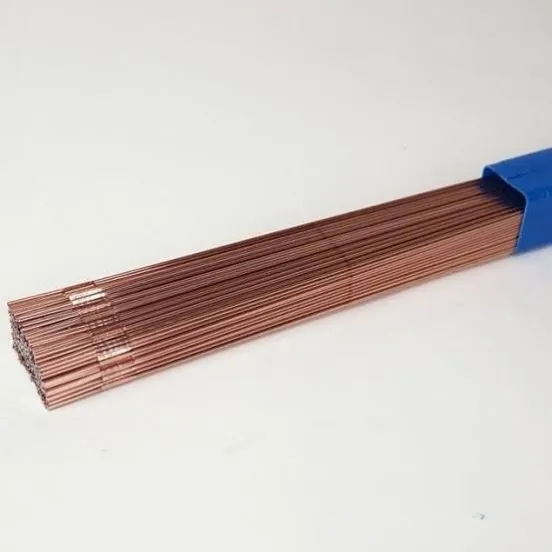
R31 TIG Welding Wire for 12Cr1MoV Steel
R31 TIG welding wire is used for welding specified low-alloy heat-resistant steels, including 12Cr1MoV when supported by the applicable welding procedure. It is intended for applications such as boiler piping and power-generation equipment where weld-metal properties and service conditions must be carefully controlled. GD WELD can help buyers confirm the applicable standard, available diameter, chemical composition and technical documentation before ordering.
Product Specifications
Item | Description |
|---|---|
Product grade | R31 |
Welding process | TIG / GTAW |
Product type | Solid TIG filler wire |
Diameter | 2.4 mm, subject to availability |
Material application | Specified 12Cr1MoV heat-resistant steel, subject to verification |
Product category | Heat Resistant & Cr-Mo |
Applicable standard | To be confirmed against the manufacturer's technical documentation |
Applications
R31 TIG welding wire may be considered for qualified welding procedures involving:
- Boiler tubes and piping: Welding specified heat-resistant steel components in boiler systems.
- Power-generation equipment: Fabrication and maintenance of compatible piping and equipment.
- High-temperature service components: Selected applications requiring suitable low-alloy filler metal.
- TIG root passes: Root welding where GTAW is specified by the approved welding procedure.
For a broader overview of the materials and grades used in this field, see our guide to Cr-Mo welding consumables, grades, materials and applications.
Actual suitability depends on the base-metal grade, operating temperature, joint design and project requirements. Confirm compatibility before selecting the filler wire.
Material Compatibility and Welding Requirements
R31 is associated with welding certain Cr-Mo-V heat-resistant steels. Before ordering, confirm whether the required base material is 12CrMoV, 12Cr1MoV, 12Cr1MoVG or another grade. Similar steel designations should not be treated as interchangeable without technical verification.
Preheating, interpass temperature control and post-weld heat treatment may be required depending on the material, thickness and approved welding procedure. Follow the qualified WPS and applicable engineering specification for welding parameters and heat treatment.
For additional context on filler-metal selection for high-temperature service, read Why Are Cr-Mo Welding Consumables Used in High-Temperature Applications.
Chemical Composition and Technical Data
Chemical composition and mechanical properties should be confirmed using the manufacturer's current technical data sheet and, where required, the batch inspection certificate. Do not rely on an assumed AWS equivalent or generic composition range when selecting welding consumables for pressure equipment or high-temperature service.
Contact GD WELD to request available technical documentation and confirm whether the supplied R31 wire meets your project requirements.
Request a Quote
For an R31 TIG welding wire quotation, please provide:
- Required diameter and quantity
- Exact base-metal grade
- Applicable standard or specification
- Application and service conditions
- Inspection, certification and packaging requirements
GD WELD can review your requirements and confirm available supply details before order placement.
Tags
R31 TIG welding wire, R31 welding wire, 12Cr1MoV welding wire, TIG filler wire, heat-resistant steel welding wire, Cr-Mo-V welding consumables, boiler tube welding, high-temperature piping welding, power plant welding consumables, GTAW filler wire, specialty welding consumables