Heat Resistant & Cr-Mo
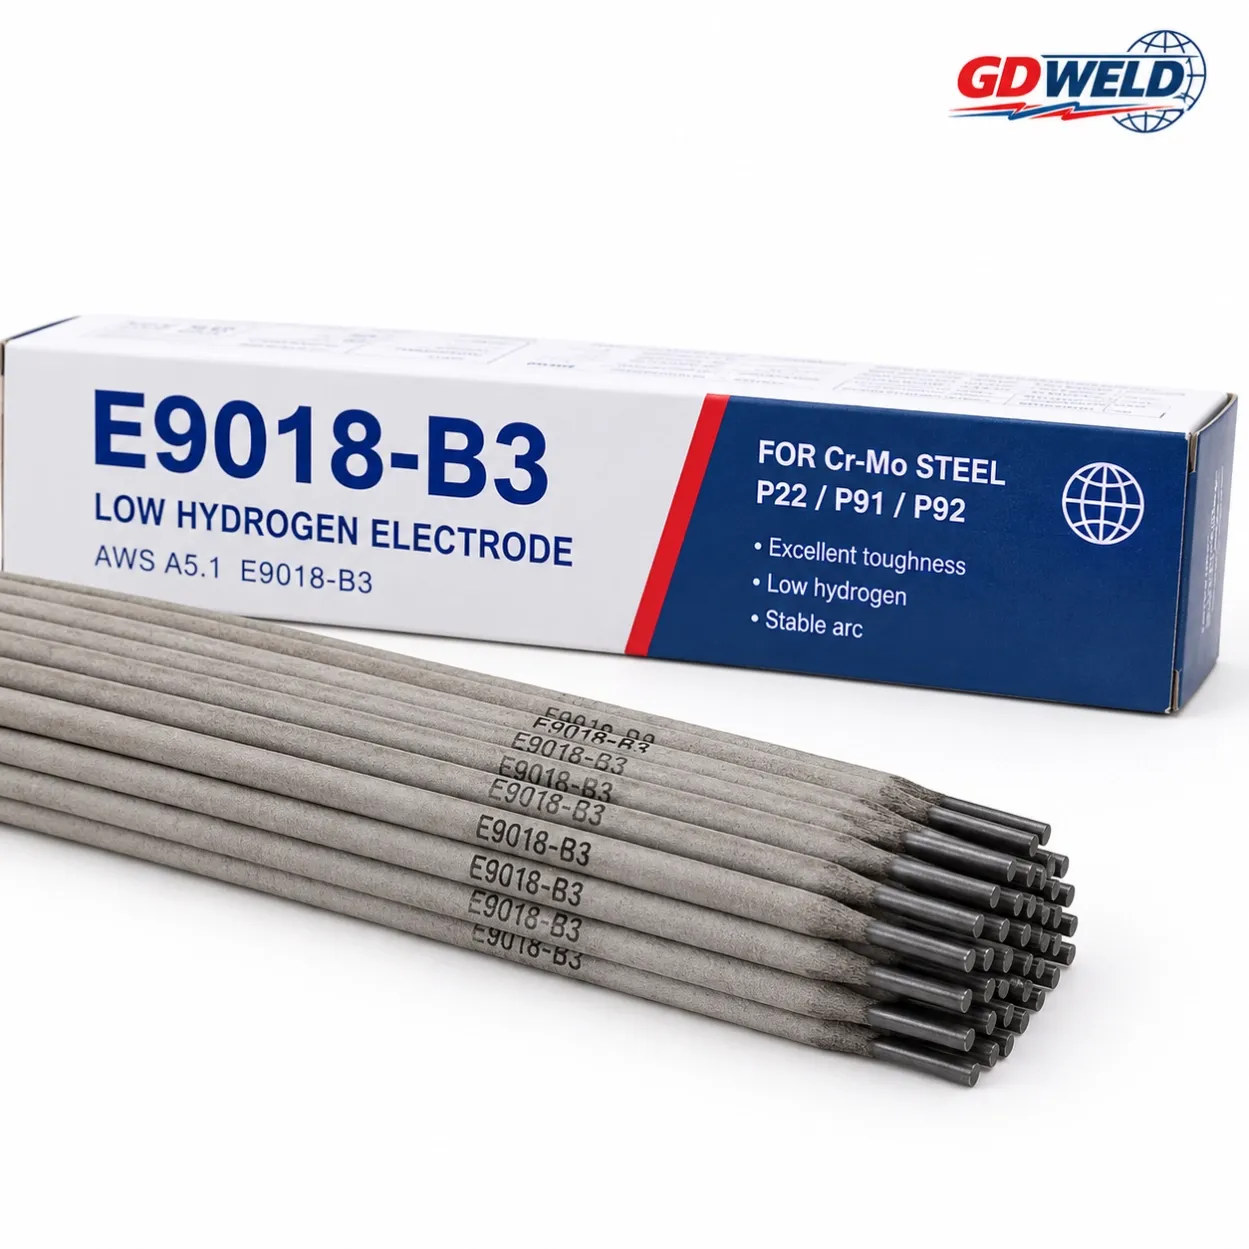
E9018-B3 Cr-Mo Welding Electrode
E9018-B3 is a low-hydrogen Cr-Mo welding electrode classified under AWS A5.5 for 2.25Cr-1Mo creep-resistant steels. It is commonly selected for P22, T22 and related Cr-Mo materials used in high-temperature piping, boilers, pressure vessels, power generation and petrochemical equipment. For P22/T22 applications requiring SMAW, E9018-B3 provides a 2.25Cr-1Mo weld deposit for elevated-temperature service.
E9018-B3 for P22 and T22 Steel
Typical base materials include:
- ASTM A335 P22
- ASTM A213 T22
- ASTM A387 Grade 22
- ASTM A182 F22
- ASTM A217 WC9
- Similar 2.25Cr-1Mo steels
E9018-B3 is also associated with 10CrMo9-10 and other equivalent Cr-Mo steels, depending on the applicable material standard and welding procedure.
For P11/P12, P91 or P92 materials, select the consumable specified for the applicable base-metal grade and qualified WPS.
Technical Data
Deposited Weld Metal Chemistry
Typical AWS classification limits:
Element | Requirement |
|---|---|
C | 0.05–0.12% |
Mn | ≤0.90% |
Si | ≤0.80% |
Cr | 2.00–2.50% |
Mo | 0.90–1.20% |
P | ≤0.030% |
S | ≤0.030% |
These are weld-deposit classification values, not base-metal composition. Actual deposited chemistry varies by product and welding conditions; the manufacturer's TDS and MTC should control project-specific requirements.
Mechanical Properties
Property | AWS Minimum |
|---|---|
Tensile Strength | ≥620 MPa (90 ksi) |
Yield Strength | ≥530 MPa (77 ksi) |
Elongation | ≥17% |
Actual commercial values can be higher after the specified heat treatment. For example, individual manufacturers report higher yield and tensile values after PWHT, so such values should be presented as product-specific data rather than universal E9018-B3 requirements.
High-Temperature Applications
E9018-B3 is used where 2.25Cr-1Mo weld metal is required for elevated-temperature and creep-resistant service, including:
- Steam and process piping
- Boiler and superheater components
- Pressure vessels
- Heat exchangers
- Power generation equipment
- Refinery and petrochemical equipment
Commercial E9018-B3 products are commonly specified for creep-resistant Cr-Mo steels in high-temperature service.
Welding & PWHT
Process: SMAW
Electrode: Basic, low-hydrogen iron-powder coated
Polarity: AC or DCEP
Typical commercial current ranges:
Diameter | Typical Current |
|---|---|
2.5 mm | 60–100 A |
3.2 mm | 80–140 A |
4.0 mm | 120–190 A |
5.0 mm | 180–250 A |
Actual current depends on electrode diameter, welding position and manufacturer. For example, published manufacturer data shows different recommended ranges for flat and out-of-position welding.
For P22/T22 welding, preheat, interpass temperature, hydrogen control and PWHT should follow the qualified WPS and applicable code. Commercial procedures may specify approximately 200–350°C preheat and 680–730°C PWHT, depending on the material and procedure.
E9018-B3 vs E8018-B2
| E8018-B2 | E9018-B3 |
|---|---|---|
Weld metal | 1.25Cr-0.5Mo | 2.25Cr-1Mo |
Typical steel | P11 / P12 | P22 / T22 |
Tensile class | 80 ksi | 90 ksi |
Process | SMAW | SMAW |
The key selection difference is the Cr-Mo alloy level and corresponding base-metal grade. E9018-B3 is the B3-class option when a 2.25Cr-1Mo consumable is required by the welding procedure.
Classification
- AWS A5.5: E9018-B3
- ASME SFA-5.5: E9018-B3
- EN ISO 3580-A: E CrMo2 B 42 H5, when certified
- Process: SMAW
- Typical Weld Metal: 2.25Cr-1Mo
Some commercial products carry an additional E9018-B3 H4/H4R designation. This suffix should only be used when the supplied electrode has the corresponding certification.
GD WELD Supply
GD WELD supplies E9018-B3 Cr-Mo welding electrodes for P22/T22 piping, boilers, pressure vessels, power generation, refinery and petrochemical applications. Different diameters, packaging and technical documentation are available for industrial procurement.
Tags
E9018-B3, E9018-B3 welding electrode, P22 welding electrode, T22 welding electrode, 2.25Cr-1Mo welding electrode, Cr-Mo welding electrode, low hydrogen Cr-Mo electrode, heat resistant steel electrode
Internal Links
👉 Internal Link 1: Anchor text: E8018-B2 welding electrode for P11 steel
👉 Internal Link 2: Anchor text: ER90S-B3 welding wire for P22 steel