Welding Wire
ER2594 Super Duplex Stainless Steel Welding Wire
For Super Duplex 2507 welding, ER2594 provides a high-alloy filler solution for UNS S32750, S32760 and similar 25% Cr super duplex stainless steels. Its Cr-Ni-Mo-N alloy system supports high strength and resistance to pitting, crevice corrosion and chloride stress corrosion cracking. ER2594 welding wire is available for TIG/GTAW and MIG/GMAW welding in oil & gas, offshore, marine, chemical and pressure equipment applications.
Super Duplex 2507 Filler Wire
ER2594 is a commonly specified filler wire for Super Duplex 2507 and related 25% Cr super duplex grades.
Typical matching materials include:
- UNS S32750 / SAF 2507 / EN 1.4410
- UNS S32760 / EN 1.4501
- S32550 and selected super duplex grades
- Selected super duplex cast materials
The filler metal should be selected according to the base material, applicable specification and qualified welding procedure.
Corrosion-Resistant Welding Applications
ER2594 is designed for demanding environments where resistance to localized and chloride-related corrosion is important. Its high Cr-Mo-N alloy system supports resistance to:
- Pitting corrosion
- Crevice corrosion
- Chloride stress corrosion cracking
- Marine and seawater exposure
Typical applications include:
- Oil and gas piping and equipment
- Offshore structures and FPSO systems
- Chemical and petrochemical equipment
- Seawater and desalination systems
- Pressure piping and vessels
- Pumps, valves and process equipment
TIG & MIG Welding
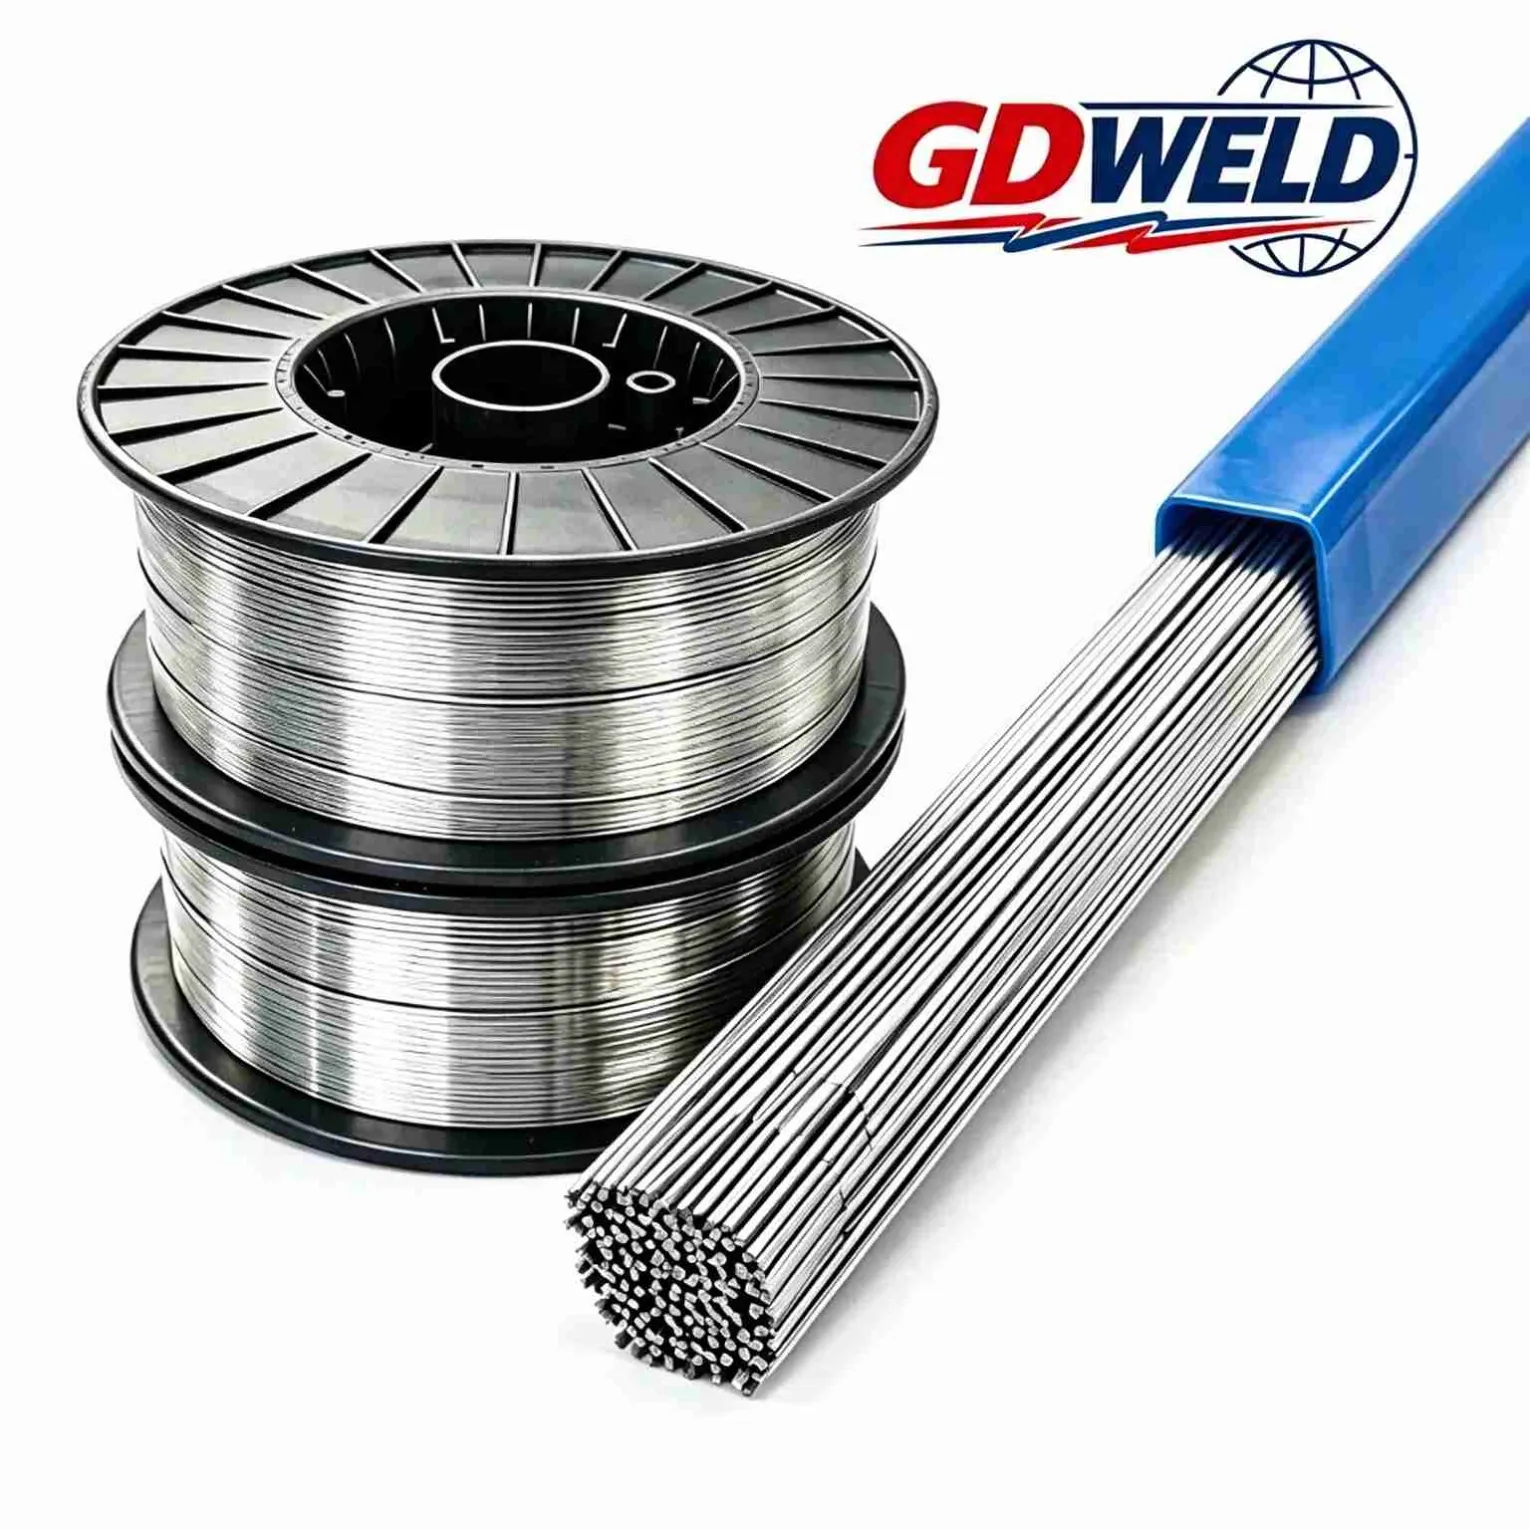
TIG / GTAW: ER2594 straight welding rods are commonly used for precision fabrication, pipe welding and root passes. Argon shielding and DCEN polarity are commonly used according to the qualified WPS.
MIG / GMAW: ER2594 spool wire is used for production welding and higher deposition rates. Suitable argon-based shielding gas and DCEP polarity are commonly applied according to the welding procedure.
For Super Duplex 2507, heat input, interpass temperature, shielding and cooling conditions should be controlled to maintain the required duplex weld-metal structure.
International Classifications
Standard | Classification |
|---|---|
AWS A5.9 / ASME SFA-5.9 | ER2594 |
EN ISO 14343-A, TIG | W 25 9 4 N L |
EN ISO 14343-A, MIG | G 25 9 4 N L |
EN ISO 14343-B | SS2594 |
The required designation should be confirmed according to the welding process and project specification. Manufacturer data confirms ER2594 / W 25 9 4 N L as commonly used designations.
Typical Chemical Composition
Element | Reference Range / Limit (%) |
|---|---|
C | ≤ 0.03 |
Si | ≤ 1.00 |
Mn | ≤ 2.50 |
P | ≤ 0.03 |
S | ≤ 0.02 |
Cr | 24.0–27.0 |
Ni | 8.0–10.5 |
Mo | 2.5–4.5 |
N | 0.20–0.30 |
Cu | ≤ 1.50 |
W | ≤ 1.00 |
These are AWS ER2594 reference classification limits. Actual wire chemistry may vary by manufacturer and production heat; the supplied MTC should be used for batch-specific values.
Typical Mechanical Properties
Typical all-weld-metal properties may include:
- Yield strength: approximately 620–650 MPa or higher
- Tensile strength: approximately 800–850 MPa or higher
- Elongation: approximately 20–30%
Actual properties depend on welding process, shielding gas, heat input, test temperature and applicable specification. Published manufacturer data shows values within this general range.
Wire Sizes
Process | Common Sizes |
|---|---|
TIG / GTAW | 1.2–3.2 mm |
MIG / GMAW | 0.8–1.6 mm |
Other diameters and packaging options can be supplied according to the welding process and project requirements.
ER2594 vs ER2209
ER2594 and ER2209 both belong to the duplex stainless steel welding wire family, but they normally target different base-material groups.
| ER2594 | ER2209 |
|---|---|---|
Material group | Super Duplex | Duplex |
Typical base materials | 2507 / S32750 / S32760 | 2205 / S31803 / S32205 |
Typical Cr level | ~25% | ~22% |
Typical service | Higher-alloy, demanding corrosion environments | Duplex 2205 applications |
For 2205-type materials, ER2209 is generally the relevant filler classification; for 2507-type Super Duplex, ER2594 is the corresponding product family to evaluate against the WPS and project specification.
Supply from GD WELD
GD WELD supplies ER2594 Super Duplex Stainless Steel Welding Wire for TIG and MIG industrial welding applications.
Straight rods and spool wire can be offered in different diameters according to the welding process and project requirements.
For quotation or specification confirmation, provide the base material, welding process, wire diameter, applicable standard and required quantity.
Tags
ER2594, ER2594 welding wire, ER2594 filler wire, ER2594 filler metal, super duplex welding wire, super duplex stainless steel welding wire, 2507 welding wire, Super Duplex 2507 welding wire, S32750 welding wire, S32760 welding wire, EN 1.4410 welding wire, EN 1.4501 welding wire, ER2594 TIG wire, ER2594 MIG wire, AWS A5.9 ER2594, W 25 9 4 N L