Welding Wire
ER430
ER430 is copper-coated 17Cr ferritic stainless steel solid wire, suitable for GMAW (MIG/MAG) and GTAW (TIG) welding.
ER430
ER430 is copper-coated 17Cr ferritic stainless steel solid wire, suitable for GMAW (MIG/MAG) and GTAW (TIG) welding.
Features
• Single-phase ferrite structure, matching 430 stainless steel thermal expansion coefficient
• Good resistance to nitric acid & atmospheric corrosion, low cost
• Smooth wire feeding, bright and clean weld appearance for decorative work
• Continuous service temperature: ≤250°C
Diameter & Packaging
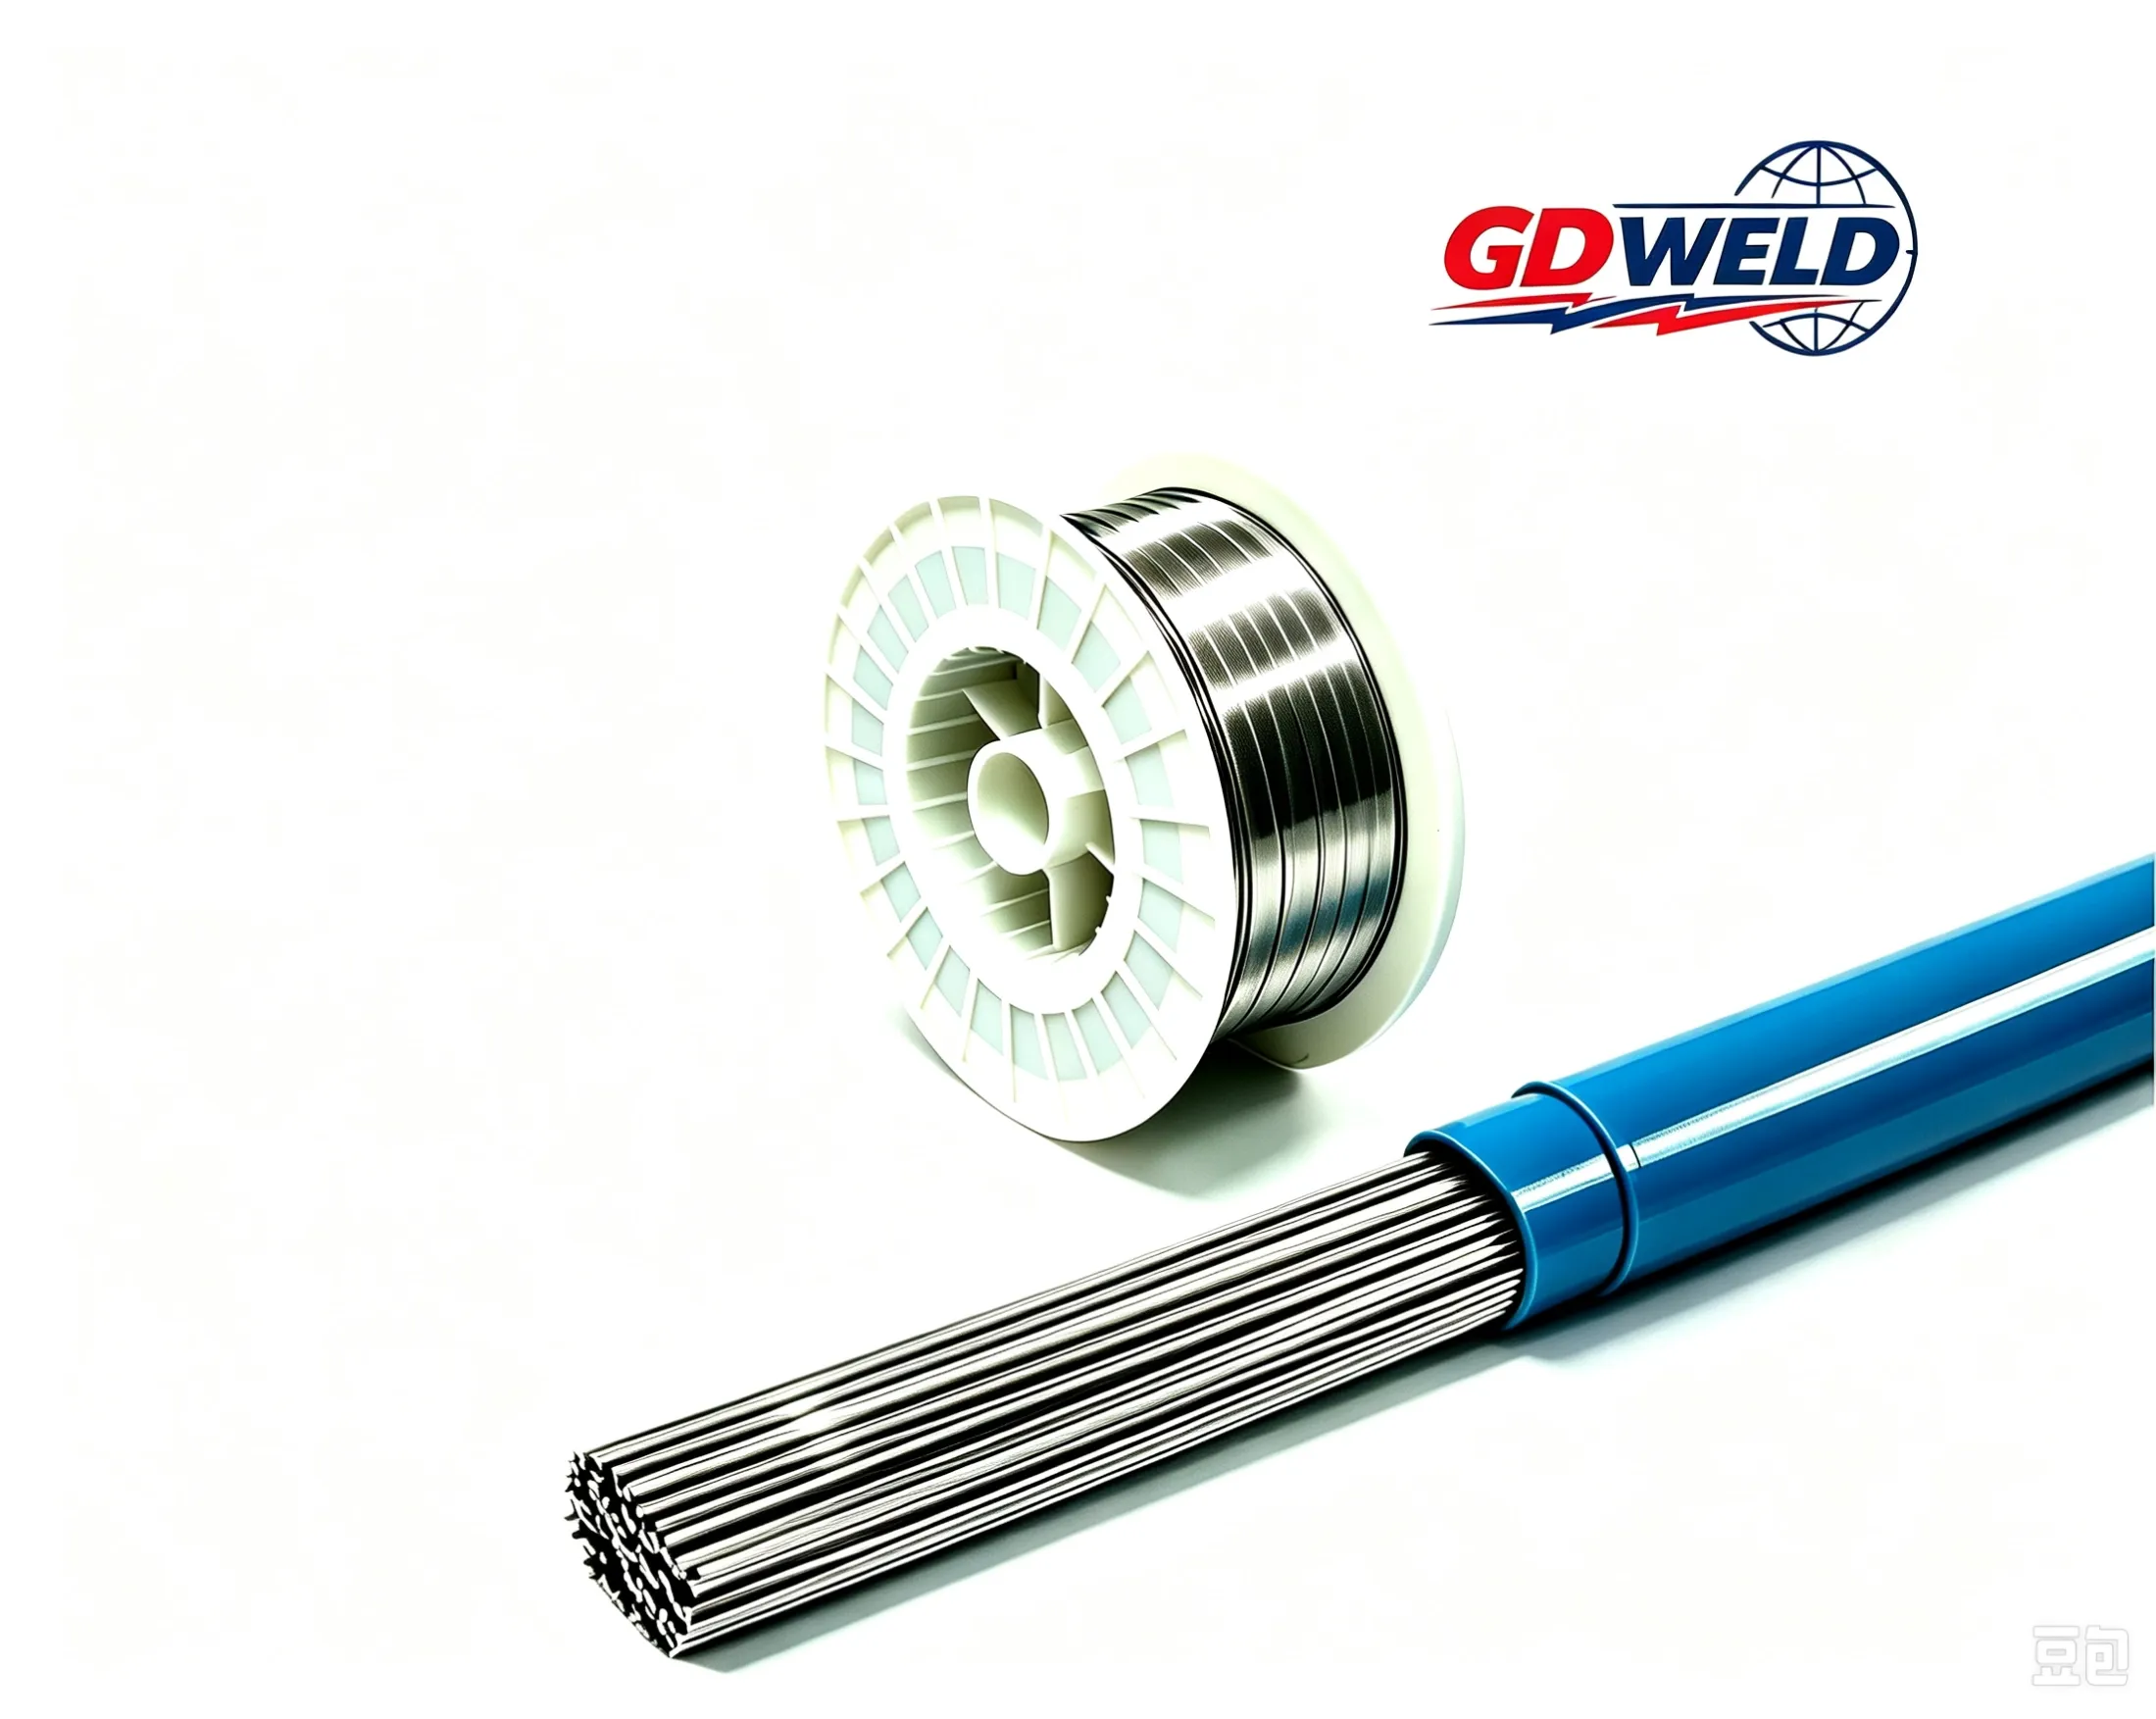
MIG:0.8 / 1.0 / 1.2 / 1.6 mm 1KG Spool/5KG Spool / 15KG Spool
TIG:2.0 / 2.4 / 3.2 mm /4.0mm 5kg plastic tube
Welding Parameters
Polarity: DC+ (DCRP, Direct Current Reverse Polarity)
MIG / MAG
Shielding Gas: 98%Ar + 2%O₂ Gas Flow Rate: 20~25 L/min Reference Current for common sizes: Φ0.8mm:70–150 A Φ1.0mm:100–200 A Φ1.2mm:140–220 A
TIG (GTAW)
Shielding Gas: 99.99% High Purity Argon Gas Flow Rate: 8–15 L/min. Back purging is recommended for thick plates.
Base Metal Matching
Suitable for 430, 430LX ferritic stainless steel welding.
Applications
Stainless steel decorative panels, automobile exhaust pipes, nitric acid storage tanks, household kitchen appliances, low-stress anti-rust frames.
⚠️ Poor low-temperature toughness; not for cryogenic or heavy load structural parts
Welding Precautions
• Thoroughly remove oil, rust, scale and moisture from grooves before welding to avoid porosity.
• Control interpass temperature below 150°C to prevent grain coarsening & embrittlement.
• Reduce heat input, use narrow bead welding.
• Wind protection required for outdoor welding wind speed over 1.0 m/s.
ER430 vs ER308L
✅ ER430 (ferritic 17Cr): Low-cost decorative, nitric acid equipment, no high strength requirement
✅ ER308L (austenitic 18-8): High toughness, food & chemical general corrosion resistant equipment
Important Cautions
• Do not use pure CO₂ shielding gas, will degrade surface finish and corrosion resistance.
• Cannot replace austenitic wires for low-temperature or chloride corrosion working conditions.