Heat Resistant & Cr-Mo
E9018-B9 / E9018-B91 Cr-Mo Welding Electrode
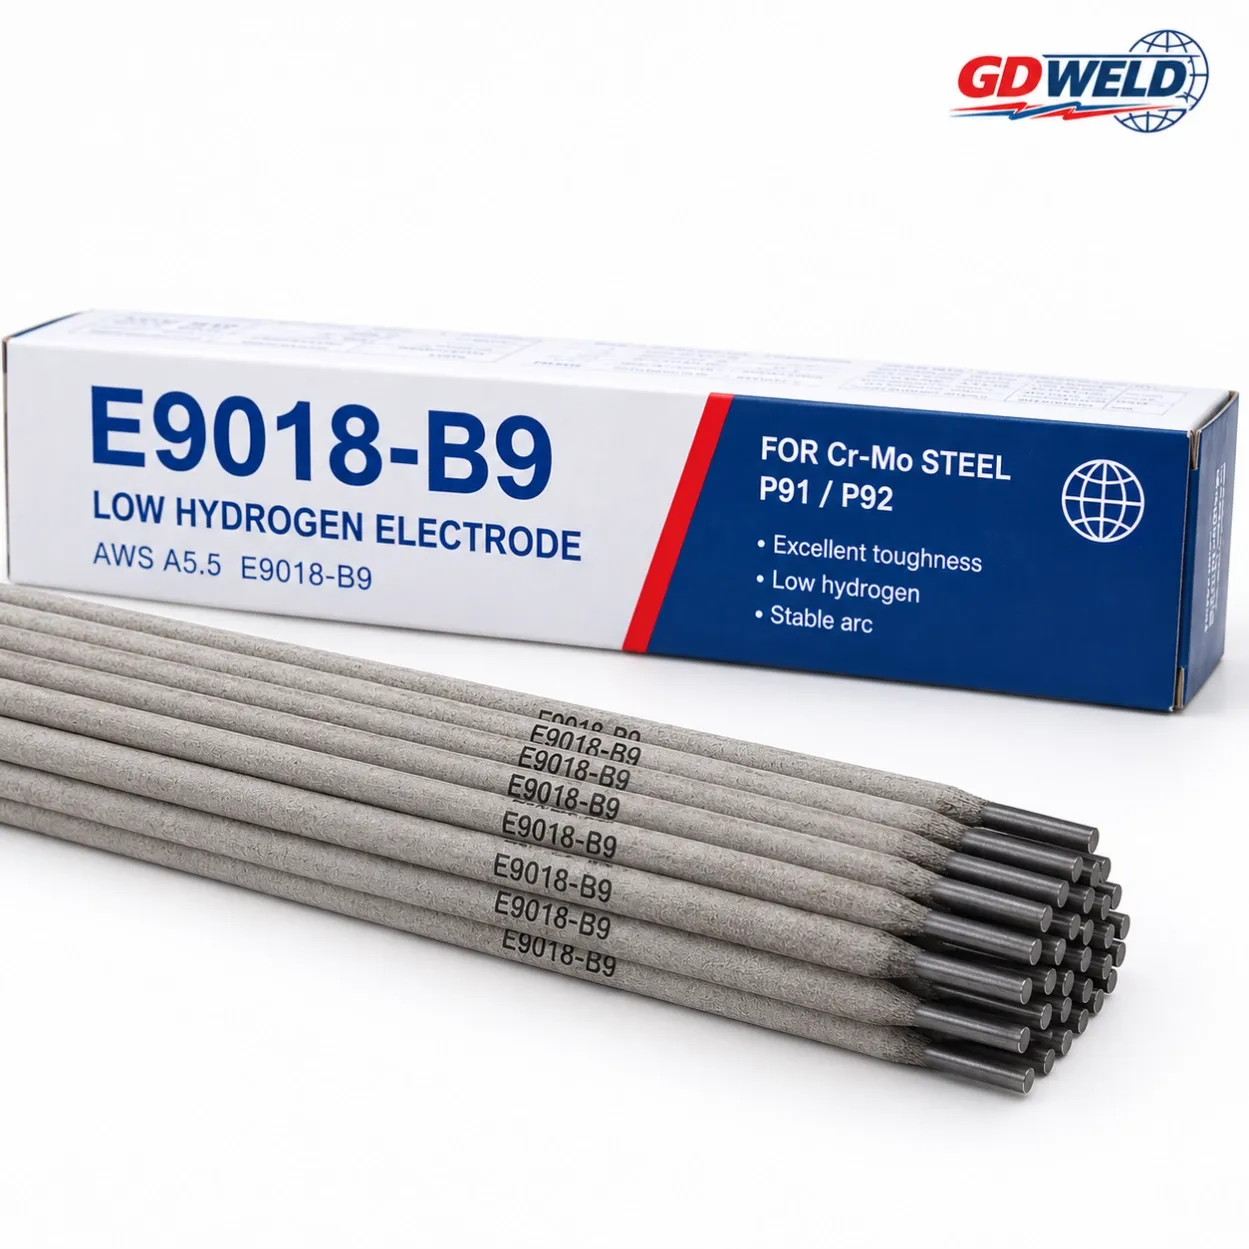
E9018-B9, currently classified as E9018-B91, is a low-hydrogen Cr-Mo welding electrode for P91 and T91 Grade 91 steel. It is designed for high-temperature piping, boilers, pressure components and power generation equipment requiring creep-resistant weld metal and controlled post-weld heat treatment.
E9018-B91 Welding Electrode for P91 and T91
E9018-B91 is the current AWS classification for this Grade 91 welding electrode. E9018-B9 is a former or commonly used market designation that may still appear in purchasing specifications and product catalogs.
It is commonly selected for welding:
- ASTM A335 P91 pipe
- ASTM A213 T91 boiler tube
- ASTM A387 Grade 91 plate
- ASTM A182 F91 forgings
- X10CrMoVNb9-1 and similar Grade 91 steels
For procurement, the electrode classification should match the base material and qualified welding procedure.
Why Choose E9018-B91 for Grade 91 Steel?
P91/T91 steel is a 9Cr-1Mo-V-Nb-N creep-resistant steel developed for elevated-temperature service. Its performance depends on controlled alloy chemistry, welding heat input and post-weld heat treatment.
E9018-B91 provides a compatible weld-metal chemistry for Grade 91 applications, with controlled chromium, molybdenum, vanadium, niobium and nitrogen.
This makes it different from E9018-B3 welding electrode, which is primarily associated with P22/T22 2.25Cr-1Mo steel.
E9018-B91 Chemical Composition
AWS classification requirements for deposited weld metal:
Element | Requirement |
|---|---|
C | 0.08–0.13% |
Mn | ≤1.20% |
Si | ≤0.30% |
P | ≤0.010% |
S | ≤0.010% |
Ni | ≤0.80% |
Cr | 8.00–10.50% |
Mo | 0.85–1.20% |
V | 0.15–0.30% |
Nb | 0.02–0.10% |
N | 0.02–0.07% |
Actual deposited chemistry depends on the manufacturer and production batch. Project-specific requirements should be verified against the product TDS and MTC.
Mechanical Properties
AWS A5.5 classification minimums:
Property | Minimum |
|---|---|
Tensile Strength | ≥620 MPa (90 ksi) |
Yield Strength | ≥530 MPa (77 ksi) |
Elongation | ≥17% |
Actual mechanical properties after PWHT may be higher and should be treated as manufacturer-specific product data.
P91 Welding: Preheat, Interpass and PWHT
P91 welding requires strict control of preheat, interpass temperature, hydrogen, heat input, cooling and PWHT.
Typical commercial guidance includes:
- Preheat: approximately 200–300°C
- Interpass: controlled according to the qualified WPS
- PWHT: commonly around 760°C
- Process: SMAW
- Polarity: AC or DCEP/DC+
PWHT temperature and holding time depend on the applicable code, material thickness and qualified WPS. Controlled cooling before PWHT may also be required to achieve the intended weld-metal transformation and hardness.
For Grade 91 components, electrode storage and low-hydrogen control are also important to reduce hydrogen-related welding risks.
Typical E9018-B91 Welding Current
Electrode Diameter | Typical Current |
|---|---|
2.5 mm | 70–110 A |
3.2 mm | 90–160 A |
4.0 mm | 130–220 A |
5.0 mm | 170–250 A |
These are typical commercial ranges, not AWS requirements. Final welding parameters should follow the electrode manufacturer's TDS and qualified WPS.
E9018-B91 vs E9018-B3
| E9018-B3 | E9018-B91 |
|---|---|---|
Base steel | P22 / T22 | P91 / T91 |
Alloy system | 2.25Cr-1Mo | 9Cr-1Mo-V-Nb-N |
Typical service | High-temperature Cr-Mo equipment | Grade 91 creep-resistant equipment |
Heat treatment | Important | Highly critical |
Do not select B91 or B3 based only on the fact that both are Cr-Mo electrodes. The consumable should be matched to the base steel and qualified welding procedure.
Classification and Industrial Supply
- Current AWS classification: E9018-B91
- Common/former designation: E9018-B9
- AWS: A5.5/A5.5M
- ASME: SFA-5.5
- EN ISO 3580-A: E CrMo91 B 42 H5, when certified
- Welding process: SMAW
- Coating: Basic, low-hydrogen
H4 or H4R hydrogen designations should only be stated when supported by the relevant product certification.
GD WELD supplies E9018-B9 / E9018-B91 welding electrodes for P91/T91 piping, boiler components, power plants, pressure equipment and other high-temperature industrial applications.
Tags
E9018-B91 welding electrode, E9018-B9 welding electrode, E9018-B91, E9018-B9, P91 welding electrode, T91 welding electrode, P91 welding rod, Grade 91 welding electrode, 9Cr-1Mo welding electrode, Cr-Mo welding electrode, low hydrogen welding electrode, P91 welding consumable
Internal Links
👉 Internal Link 1: Anchor text: E9018-B3 welding electrode for P22 steel
👉 Internal Link 2: Anchor text: E8018-B2 welding electrode for P11 steel