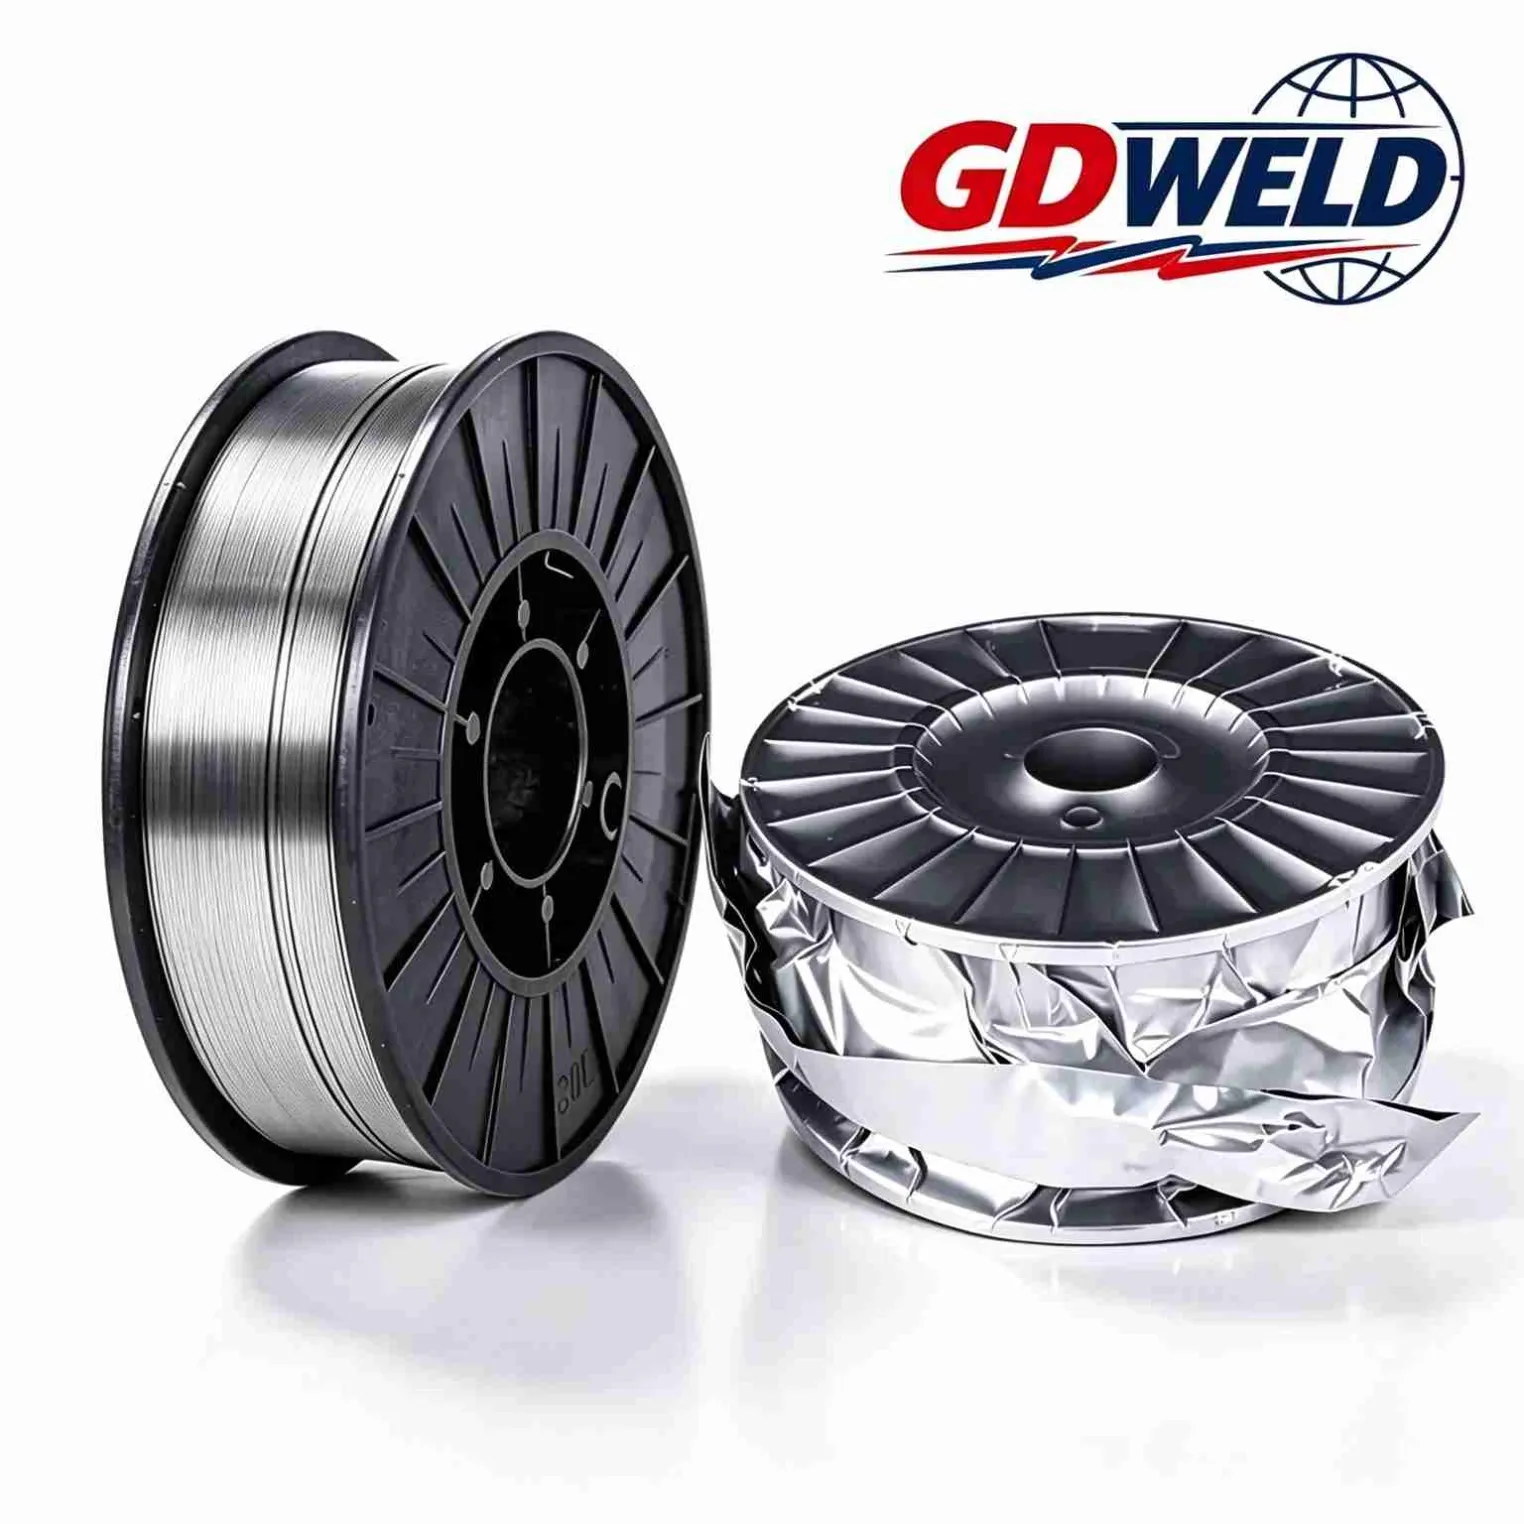
Metal & Flux Cored Wire
E308LT1-1C Stainless Steel Flux Cored Welding Wire
E308LT1-1C stainless steel flux cored welding wire is designed for gas-shielded FCAW of compatible 304 and 304L stainless steels. Using CO₂ shielding gas and DCEP polarity, it supports efficient welding in industrial fabrication. The supplied test report records 0.026% carbon, 611 MPa tensile strength and 42% elongation. Suitable for stainless steel tanks, piping, food processing equipment and general fabrication, subject to application requirements.
Key Features and Benefits
- Low-carbon deposited metal: The reported carbon content is 0.026%, within the ≤0.04% limit shown in the supplied specification.
- Chromium-nickel weld composition: The reported chromium and nickel contents are 19.960% and 9.66%, respectively.
- CO₂ gas shielding: The supplied welding data specifies CO₂ as the shielding gas.
- Documented mechanical properties: The test report records a tensile strength of 611 MPa and elongation of 42%.
- Defined operating parameters: Current, voltage, polarity, interpass temperature and welding speed are provided for process planning.
Typical Applications
E308LT1-1C stainless steel flux cored welding wire may be considered for compatible stainless steel fabrication, including:
- Stainless steel tanks, vessels and piping
- Food processing equipment and commercial kitchen components
- General industrial and chemical equipment fabrication
- Stainless steel sheet metal, frames and fabricated assemblies
- Production welding of compatible 304/304L stainless steel components
For other stainless steel welding applications, explore our E308L-16 Stainless Steel Welding Electrode for compatible 304/304L stainless steel welding requirements. Select the consumable according to the welding process, base material and applicable procedure.
For applications involving corrosive chemicals, elevated temperatures or pressure service, verify the base-metal grade, corrosion requirements, design code and applicable welding procedure before selecting the consumable.
Welding Parameters
The supplied product data gives the following operating range. These values should be treated as reference parameters and adjusted only in accordance with the approved welding procedure and manufacturer's instructions.
Parameter | Supplied Value |
|---|---|
Welding Process | Gas-Shielded Flux Cored Arc Welding (FCAW-G) |
Shielding Gas | CO₂ |
Current Range | 130–230 A |
Voltage Range | 26–31 V |
Polarity | DCEP (DC Electrode Positive) |
Maximum Interpass Temperature | 100°C |
Welding Speed | 300–400 mm/min |
Before production welding, confirm the wire diameter, joint design, material thickness, welding position and gas flow requirements against the applicable technical data sheet. The table does not replace a qualified welding procedure specification (WPS).
Deposited Metal Chemical Composition
The following values are transcribed from the supplied inspection report.
Element | Requirement (%) | Actual Result (%) |
|---|---|---|
Carbon (C) | ≤0.04 | 0.026 |
Manganese (Mn) | 0.5–2.5 | 1.120 |
Silicon (Si) | ≤1.0 | 0.61 |
Sulfur (S) | ≤0.03 | 0.005 |
Phosphorus (P) | ≤0.04 | 0.013 |
Chromium (Cr) | 18.0–21.0 | 19.960 |
Nickel (Ni) | 9.0–11.0 | 9.66 |
Molybdenum (Mo) | ≤0.5 | 0.02 |
Copper (Cu) | ≤0.5 | 0.01 |
The reported composition indicates a low-carbon chromium-nickel weld-metal chemistry within the limits listed in the supplied report. Actual results may vary by production batch and testing method. Confirm the product classification and applicable standard edition against the official certificate before presenting these limits as classification-wide requirements.
Deposited Metal Mechanical Properties
Property | Requirement | Actual Result |
|---|---|---|
Yield Strength | Not specified in supplied table | 471 MPa |
Tensile Strength | ≥520 MPa | 611 MPa |
Elongation | ≥35% | 42% |
Bend Test | As specified | Pass |
Radiographic Test | Grade II requirement shown | Grade I result shown |
The supplied test results show tensile strength and elongation above the stated minimum requirements. The bend test is recorded as passing, and the radiographic result is listed as Grade I against a Grade II requirement in the report. Acceptance criteria depend on the governing standard and inspection procedure, so the original certificate should be retained for technical review and contractual verification.
For additional background on selecting welding consumables, read our article on Cr-Mo welding consumable grades, materials and applications. Although it focuses on Cr-Mo alloys, it explains why filler-metal classification, base-metal compatibility and welding procedure requirements matter when selecting consumables.
Product Selection and Purchasing Information
When selecting E308LT1-1C stainless steel flux cored welding wire, buyers should confirm the required material grade, wire diameter, shielding gas, welding position, mechanical-property requirements and project specification. These details help determine whether the product is appropriate for the intended application.
For quotations and export orders, please provide the required diameter, packaging format, order quantity, destination and any project-specific standards. GD WELD can then confirm product availability and provide the applicable technical documentation for review.
Request a Quotation
Contact GD WELD for E308LT1-1C stainless steel flux cored welding wire availability, technical information and export quotations. Share your application and purchasing requirements to help our team assess the appropriate product specification for your project.