
All products
122 products
Heat Resistant & Cr-Mo
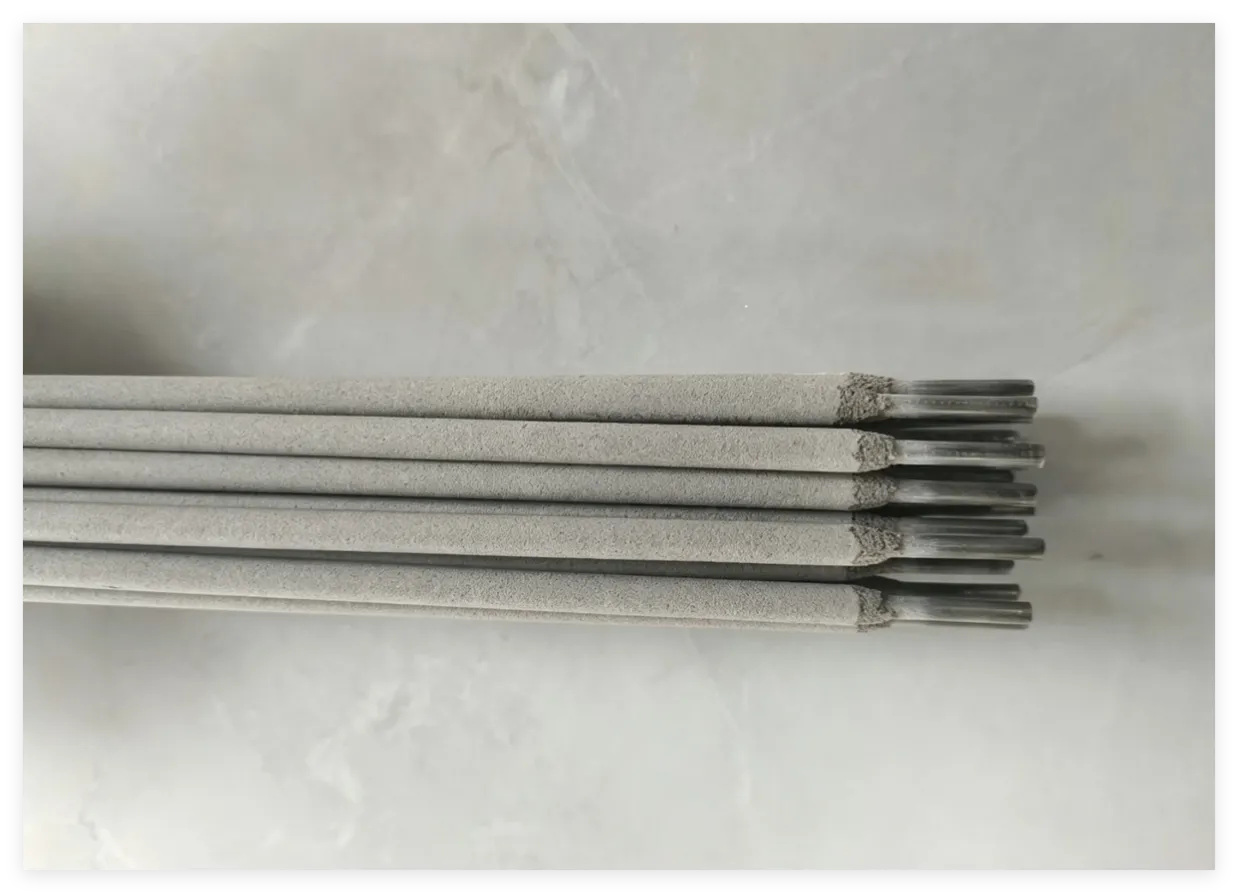
E9018-B92 Cr-Mo Welding Electrode for P92 Steel
E9018-B92 is a low-hydrogen Cr-Mo-W welding electrode for P92 and T92 Grade 92 steels. It is designed for high-temperature and creep-resistant welding in power plants, boilers, steam piping and pressure components. With a controlled 9Cr-2W-Mo-V-Nb alloy system, E9018-B92 provides weld-metal chemistry suited to Grade 92 steel applications. Product selection should be confirmed against the base-metal grade, project specification and qualified WPS.
Low Alloy & High Strength
E9018-G High Strength Low Alloy Welding Electrode
E9018-G is a 90 ksi high-strength low-alloy steel welding electrode classified under AWS A5.5/A5.5M. It is a basic, low-hydrogen SMAW electrode for high-strength steel and demanding low-alloy welding applications. Unlike fixed-alloy classifications such as E9018-B2, E9018-B3 and E9018-B91, the E9018-G classification allows an agreed weld-metal chemistry. The manufacturer's TDS and MTC are therefore important when selecting the electrode for a specific steel grade or application.
Heat Resistant & Cr-Mo
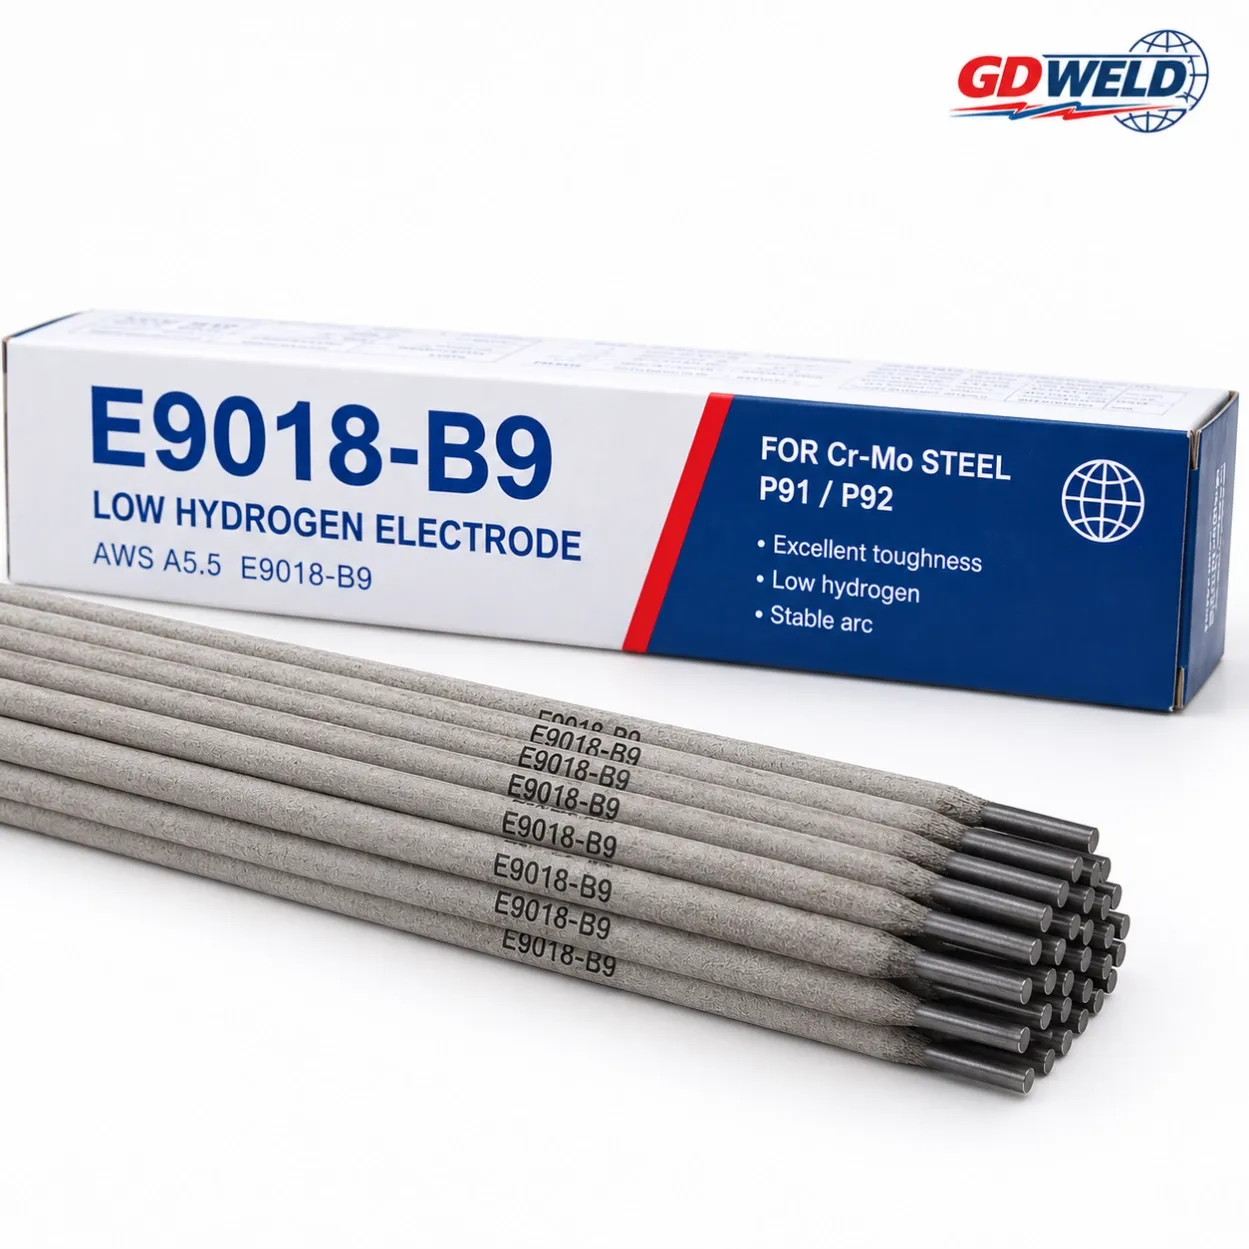
E9018-B9 / E9018-B91 Cr-Mo Welding Electrode
E9018-B9, currently classified as E9018-B91, is a low-hydrogen Cr-Mo welding electrode for P91 and T91 Grade 91 steel. It is designed for high-temperature piping, boilers, pressure components and power generation equipment requiring creep-resistant weld metal and controlled post-weld heat treatment.
Heat Resistant & Cr-Mo
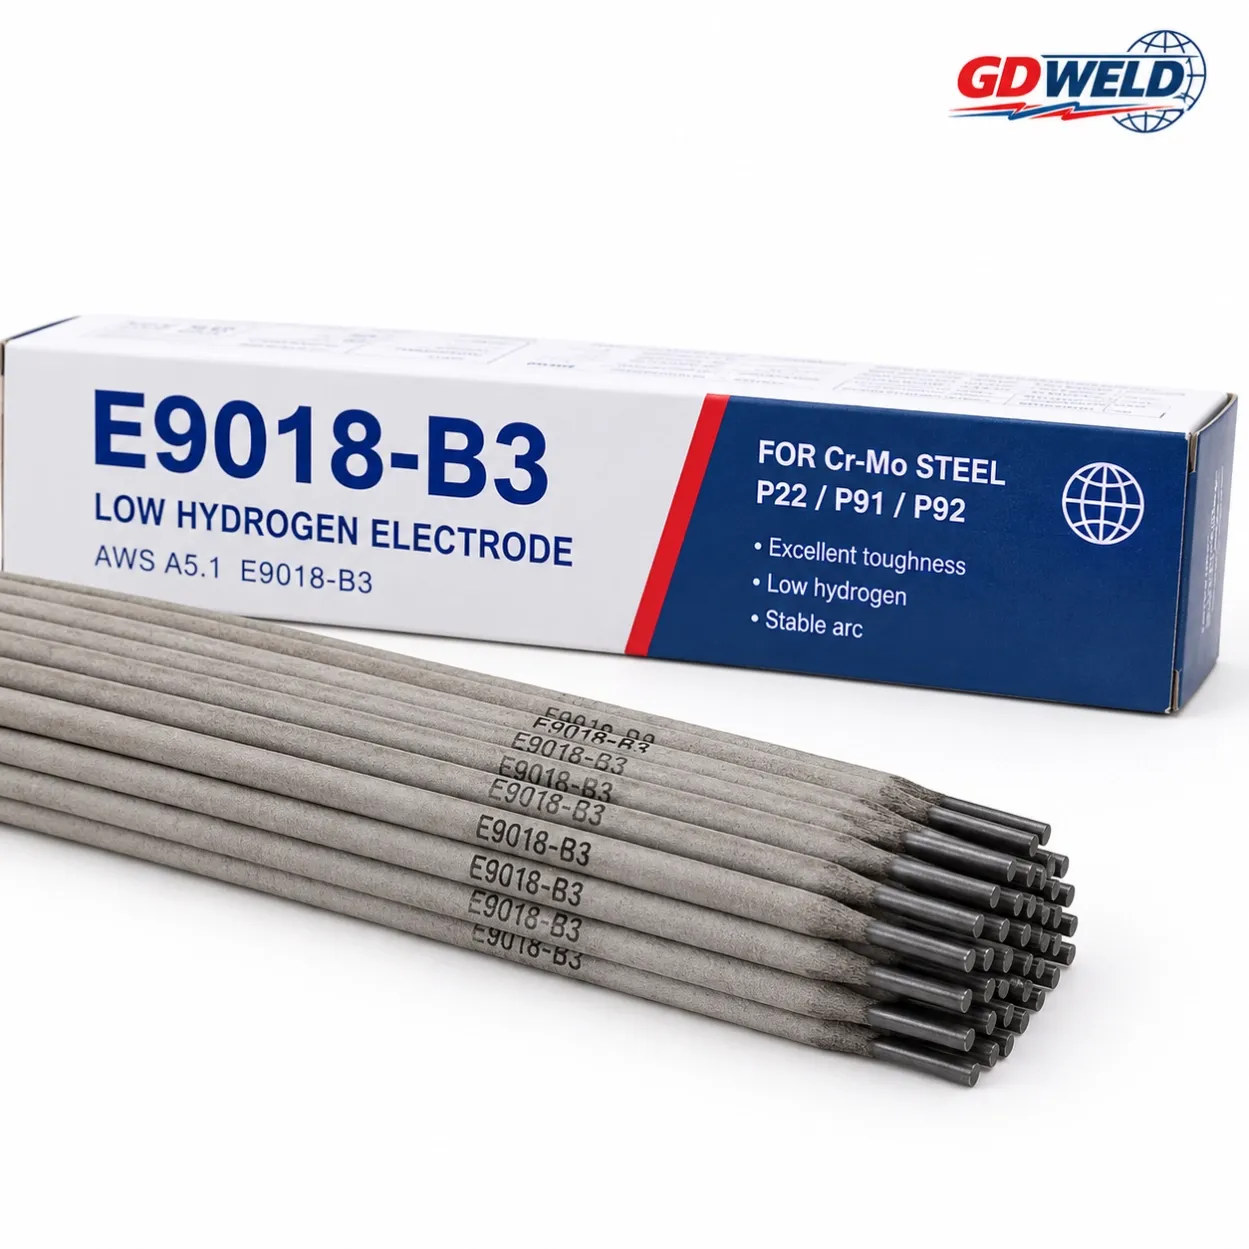
E9018-B3 Cr-Mo Welding Electrode
E9018-B3 is a low-hydrogen Cr-Mo welding electrode classified under AWS A5.5 for 2.25Cr-1Mo creep-resistant steels. It is commonly selected for P22, T22 and related Cr-Mo materials used in high-temperature piping, boilers, pressure vessels, power generation and petrochemical equipment. For P22/T22 applications requiring SMAW, E9018-B3 provides a 2.25Cr-1Mo weld deposit for elevated-temperature service.
Welding Electrode
E385-16 904L Stainless Steel Welding Electrode
E385-16 is a high-alloy austenitic stainless steel welding electrode designed primarily for 904L stainless steel (UNS N08904 / EN 1.4539). Its low-carbon Cr-Ni-Mo-Cu weld metal provides high corrosion resistance in sulfuric acid, phosphoric acid, chloride-containing and other aggressive environments. It is commonly used in chemical processing, acid handling, process piping, tanks, heat exchangers and other corrosion-resistant industrial applications.
Welding Wire
ER16-8-2 High Temperature Stainless Steel Welding Wire
ER16-8-2 is a 16-8-2 high temperature stainless steel welding wire classified under AWS A5.9. Its nominal 16Cr-8Ni-2Mo weld metal is designed for welding selected 3XXH stainless steels where high-temperature stability, hot ductility and resistance to thermal embrittlement are important. ER16-8-2 welding wire is commonly used for 304H, 321H, 347H and 316H stainless steels in high-temperature piping, power generation, petrochemical and chemical processing applications.
Welding Electrode
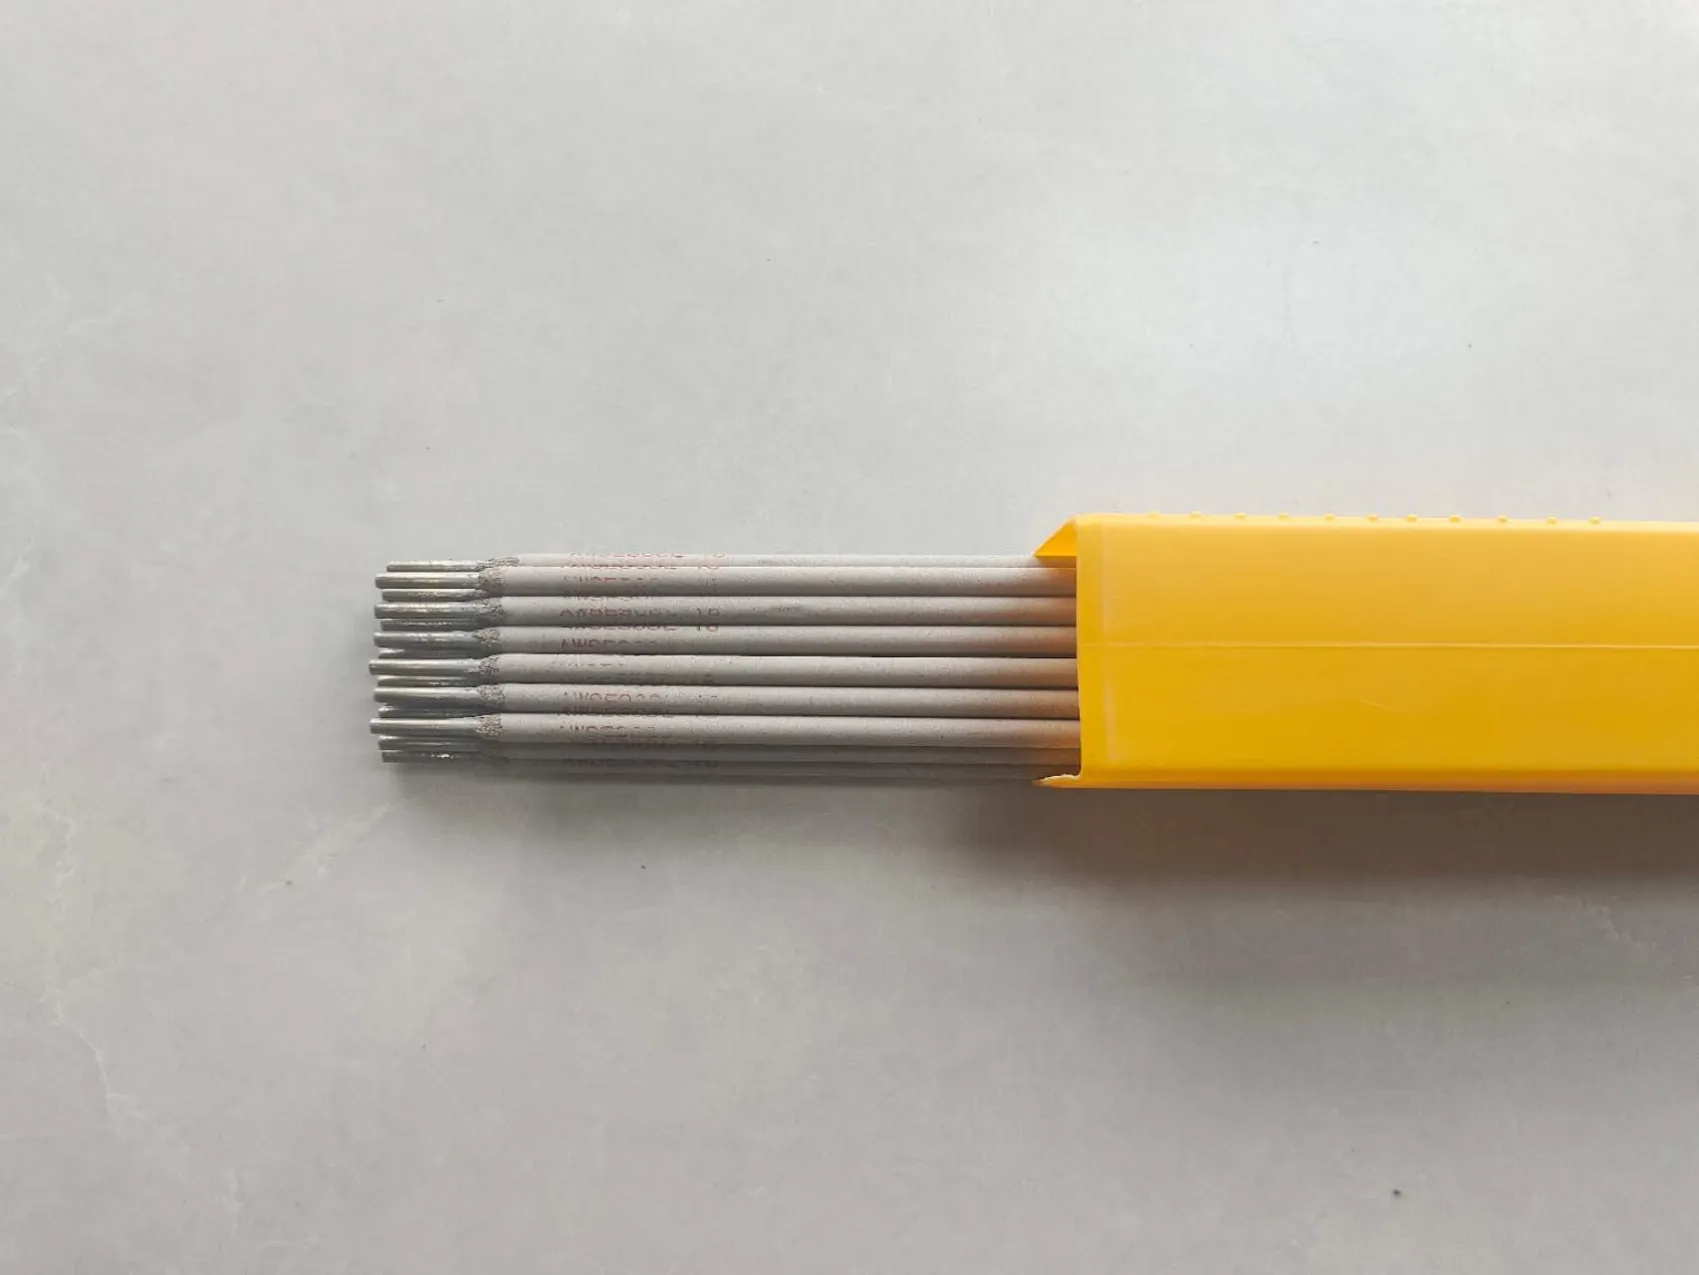
E309MoL-16 Stainless Steel Welding Electrode
E309MoL-16, also classified as E309LMo-16, is a low-carbon Cr-Ni-Mo stainless steel welding electrode conforming to AWS A5.4 / ASME SFA-5.4. With a typical 22Cr-12Ni-2.5Mo weld metal, it is mainly selected for dissimilar metal welding, including stainless steel to carbon steel or low-alloy steel, and for selected clad steel applications.
Metal & Flux Cored Wire
E91T1-B9 Flux Cored Welding Wire
E91T1-B9 is a 9Cr-1Mo-V-Nb flux cored welding wire for welding P91, T91 and Grade 91 creep-resistant steels. Classified under AWS A5.29 / ASME SFA-5.29, it is designed for high-temperature power generation, steam piping, pressure equipment and refinery applications. E91T1-B9 is available in E91T1-B9C and E91T1-B9M shielding-gas classifications for gas-shielded FCAW.
Welding Electrode
A607 E330MoMnWNb-15 High Temperature Stainless Steel Welding Electrode
A607 E330MoMnWNb-15 is a low-hydrogen austenitic stainless steel welding electrode classified under GB/T 983. It is designed for high-temperature stainless steel welding, particularly components operating at approximately 850–900°C. A607 is commonly used for hydrogen reformer furnace collector pipes, expansion pipes, Cr20Ni32 and Cr18Ni37 stainless steel components where high-temperature welding performance is required.
Metal & Flux Cored Wire
E410NiMoT1-1/-4 Stainless Steel Flux Cored Welding Wire
E410NiMoT1-1/-4 is a 410NiMo flux cored welding wire for 13Cr-4Ni martensitic stainless steel and ASTM CA6NM. Its Cr-Ni-Mo weld-metal system is suited to hydro turbine components, pumps, valves and repair welding where high strength and controlled heat treatment are required. It is designed for FCAW-G applications using CO₂ or Ar/CO₂ shielding gas.
Page 10 of 13
Technical Blog
Welding Guides & Technical Resources
Practical guides for selecting welding consumables, understanding AWS classifications and solving material-specific welding challenges.
View all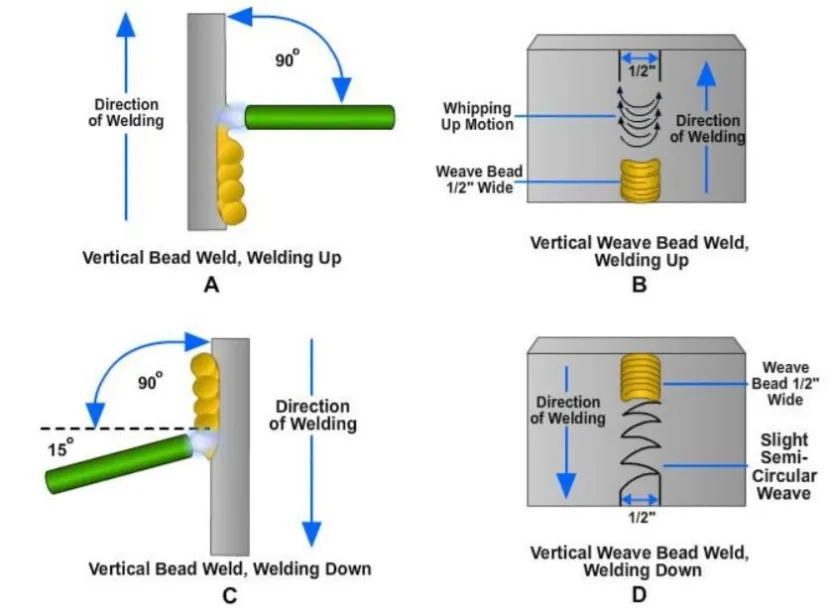
Featured
E6011 Vertical Up vs. Vertical Down Welding: Which Should You Use?
Can E6011 be used for vertical up and vertical down welding? Compare welding directions, applications, and key factors for choosing the right technique.
Latest
Can You Use E6011 Welding Rods with AC or DC?
Can E6011 welding rods run on AC or DC? Learn the correct polarity, compare AC and DC+ welding, and check your electrode specifications before welding.
When Should You Use ER70S-2 Welding Wire? Applications and Selection Guide
When should you use ER70S-2 welding wire? Find out which carbon steel applications suit it and how to select the right wire or TIG filler rod.
About GD WELD
Specialty Welding Consumables
Looking for a specific or hard-to-source welding grade? Send us your AWS classification, base material, diameter and application. We will help you identify a suitable product and supply solution.
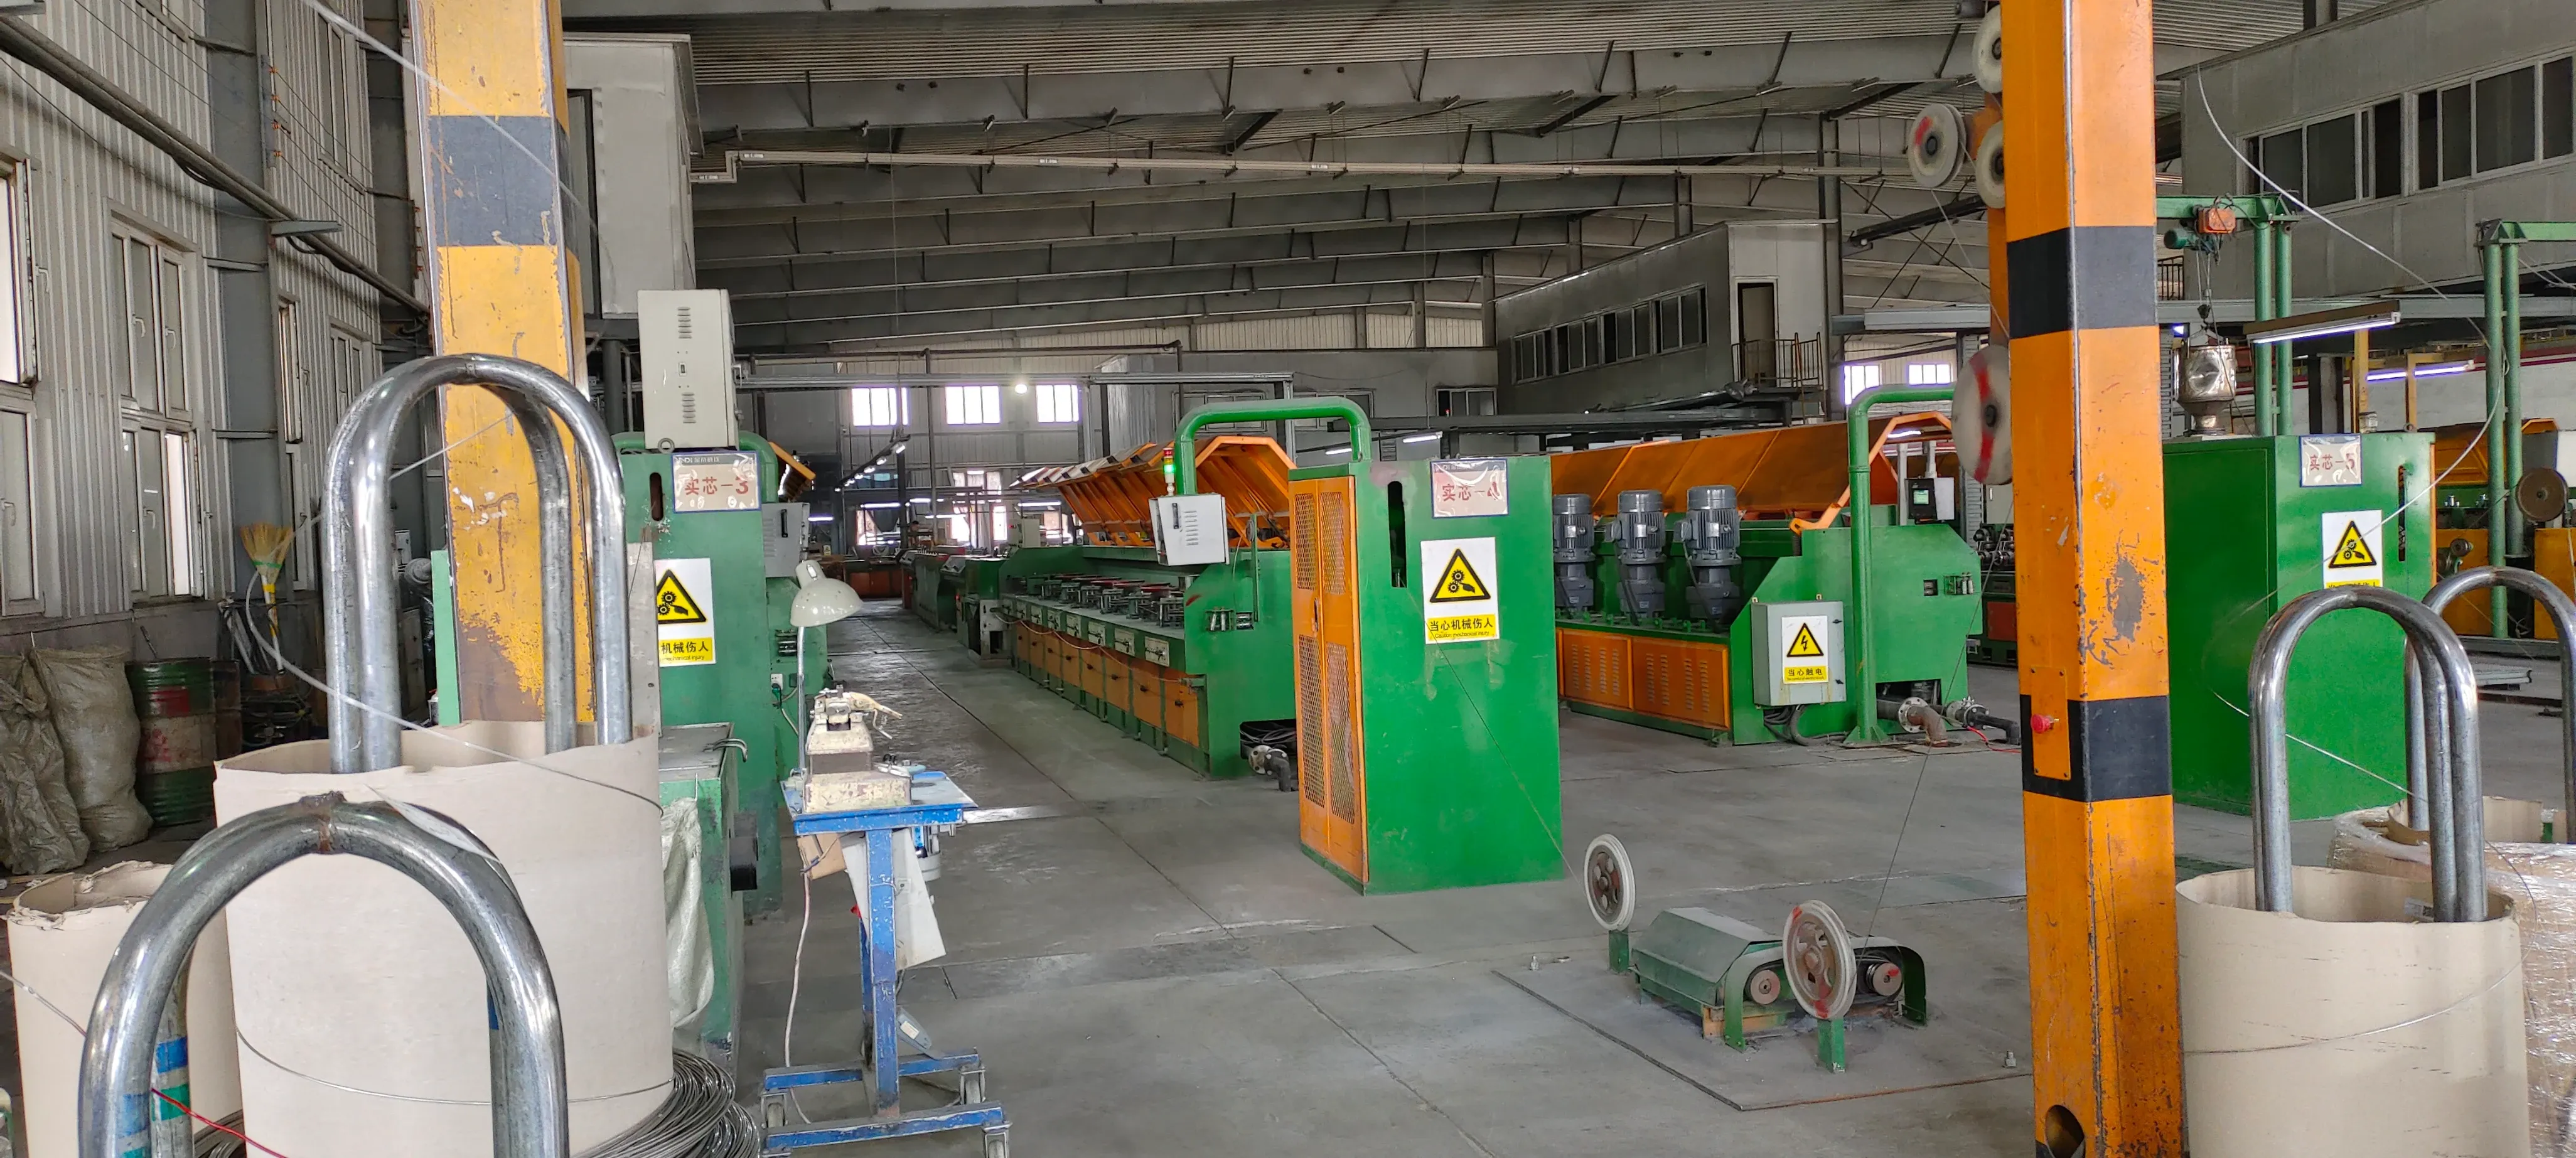
GD WELD is a China-based specialty welding consumables supplier, focused on sourcing and supplying welding wires and electrodes for demanding industrial applications. Specialty Grades · Reliable Sourcing · Technical Matching · Global Supply
Contact
Specialty Welding Consumables
Need a hard-to-source welding consumables? Please contact GD WELD.
Email
info@gdweld.com
WHATSAPP
+86 189 5451 5522
Office
District Lingcheng,City Dezhou,Province Shandong,
China
Working Time
From Monday To Friday
Inquiry
Send the Inquiry
If you are looking for a specific or hard-to-source welding grade...