All products
89 products

Aluminum & Copper Alloys
ER5554
ER5554 is an aluminum filler metal that contains more manganese and zinc with slightly more magnesium than ER5356.

Aluminum & Copper Alloys
ER5556
ER5556 (AlMg5.2Mn) is high-magnesium aluminum-manganese filler wire for welding 5xxx aluminum-magnesium alloys.

Aluminum & Copper Alloys
ERCuSi-A
ERCuSi-A is silicon bronze wire for MIG/TIG welding of copper, brass, silicon bronze and galvanized steel. With ~3% Si and trace Mn, Sn, it offers good corro...
Aluminum & Copper Alloys
ERCuSn-A
ERCuSn-A is copper-tin phosphor bronze solid welding wire. Contains 4.0~6.0% tin and phosphorus as deoxidizer. Suitable for GMAW(MIG/MAG) & GTAW(TIG).

Nickel & Special Alloys
ERTi-2
ERTi-2 is Grade 2 commercially pure titanium filler metal, suitable for GTAW(TIG), GMAW(MIG) and SAW, with outstanding corrosion resistance, moderate strengt...
Nickel & Special Alloys
ERTi-5
ERTi-5 is Ti-6Al-4V titanium alloy solid welding wire. Contains 5.5~6.75% aluminum and 3.5~4.5% vanadium for high strength. Suitable for GMAW(MIG/MAG) & GTAW...
Cast Iron & Hardfacing
ERCoCr-A
ERCoCr-A (Stellite 6) is universal Co-Cr-W hardfacing wire for GTAW and GMAW. It delivers excellent wear & corrosion resistance at high temperature, widely u...
Low Alloy & High Strength
ER80S-Ni1
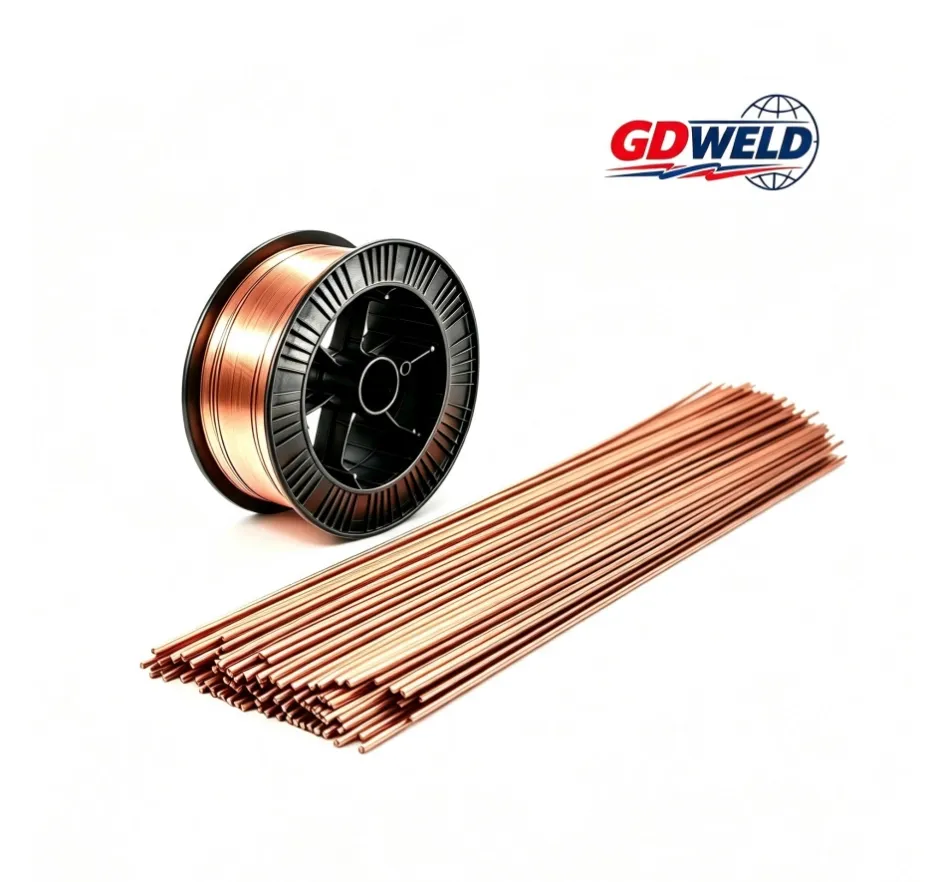
AWS A5.28 ER80S-Ni1 low-alloy welding wire with approximately 1% nickel for low-temperature and high-toughness steel applications, including pipelines, pressure vessels, tanks, offshore structures and oil & gas equipment. ER80S-Ni1 is a 1% Ni solid welding wire designed for compatible low-alloy and fine-grained steels where good weld-metal toughness at sub-zero temperatures is required. ER80S-Ni1 is available for GMAW/MIG and GTAW/TIG applications, subject to product form and specification.

Cast Iron & Hardfacing
ENi-CI Nickel 99
ENi-CI (Nickel 99) welding electrode for thin cast iron sections. All-position electrode with excellent machinability for cast iron repair and joining.

Cast Iron & Hardfacing
ENiFe-CI Nickel 55
ENiFe-CI (Nickel 55) electrode for cast iron, malleable and ductile iron. All-position joining and surfacing, including dissimilar metals to mild/stainless steel.
Page 6 of 9
Technical Blog
Welding Guides & Technical Resources
Practical guides for selecting welding consumables, understanding AWS classifications and solving material-specific welding challenges.
View all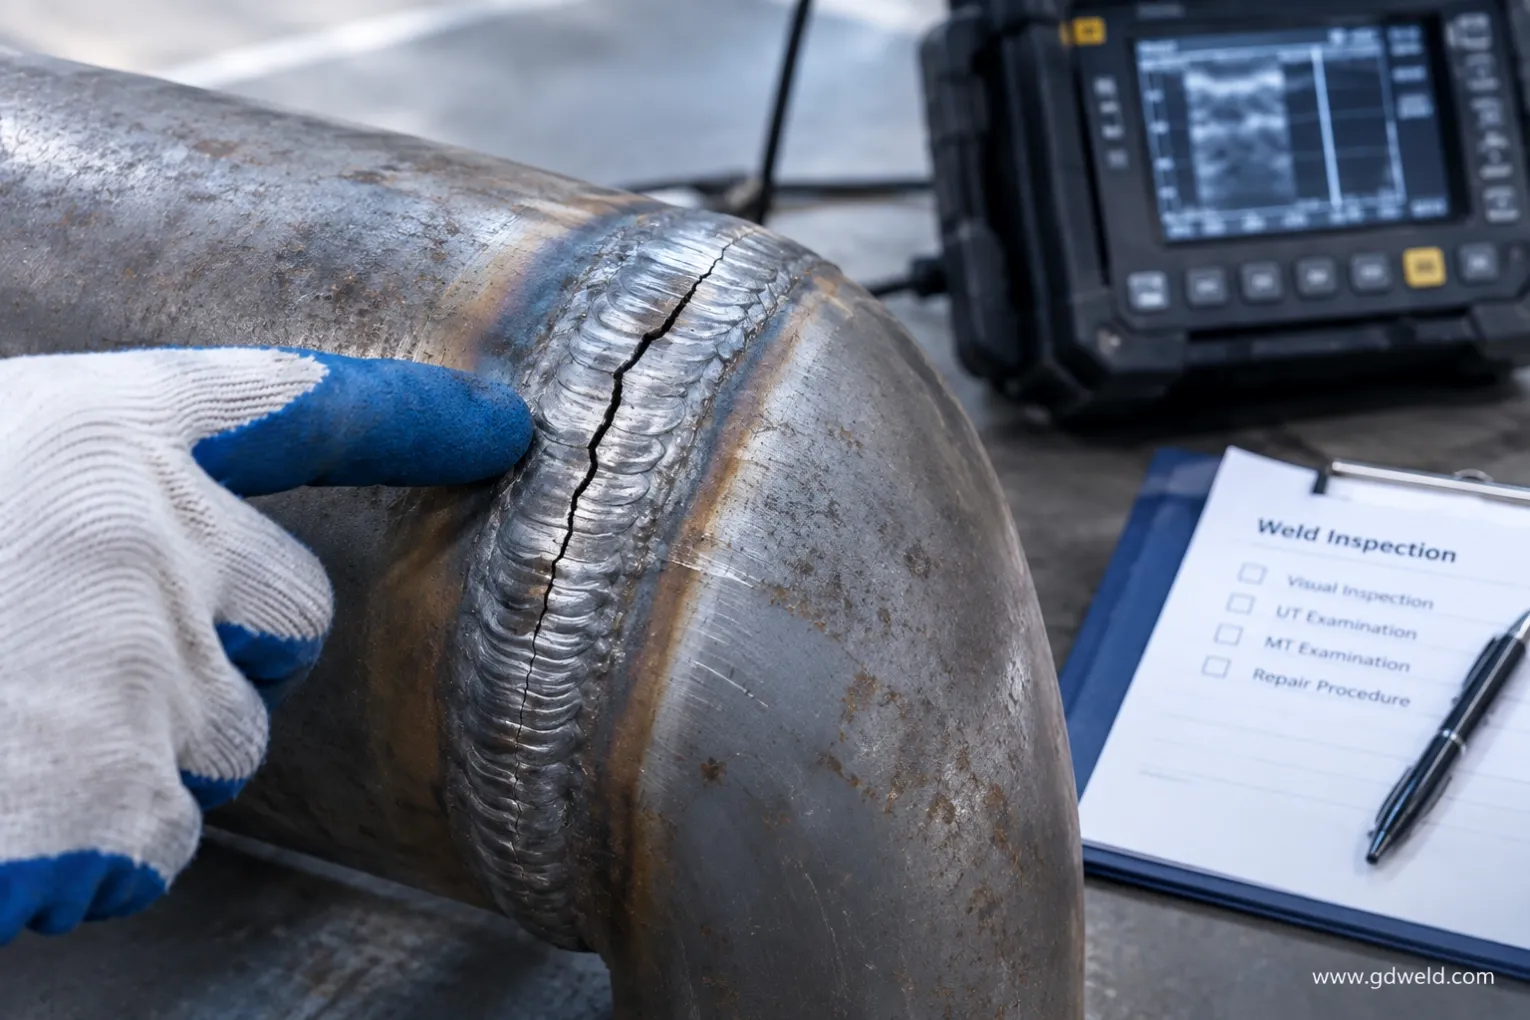
FeaturedOct 4, 2026
Why Does High-Strength Steel Crack After Welding? What Should I Check?
Why does high-strength steel crack after welding? What should you check before repairing the weld—crack location, timing, welding wire, preheat, or the WPS?
Latest
Oct 1, 2026
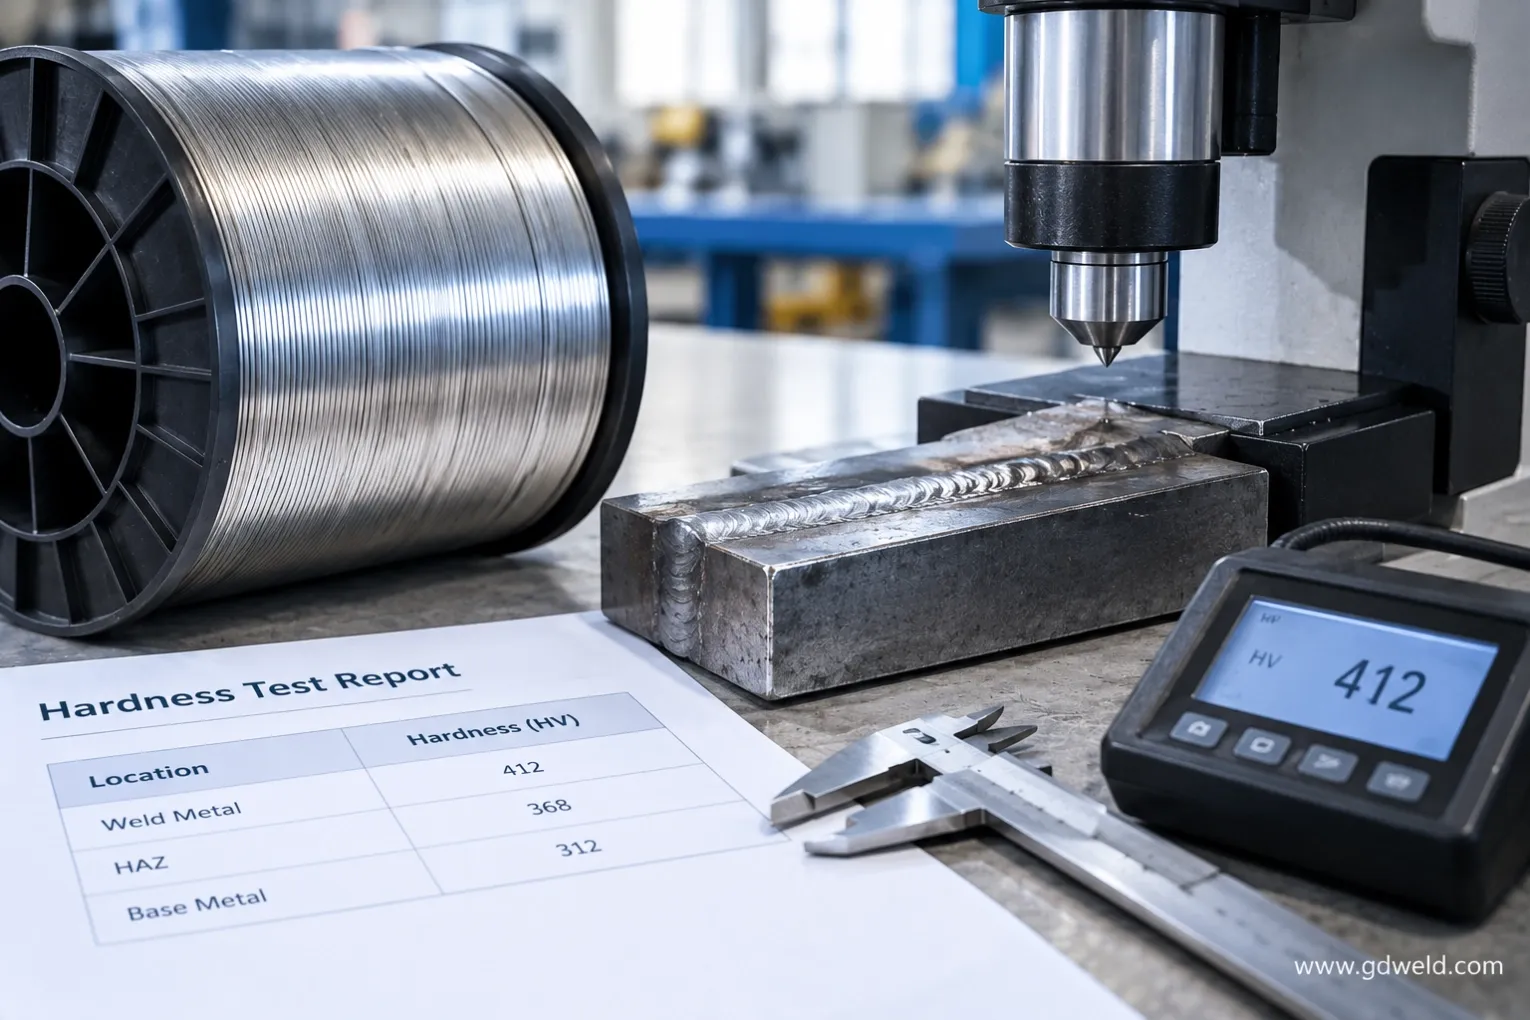
Why Is My High-Strength Weld Too Hard? What Should I Check?
Why is my high-strength weld too hard after welding or PWHT? Is the problem the welding wire, HAZ, cooling rate, heat input, or heat treatment?
Sep 30, 2026
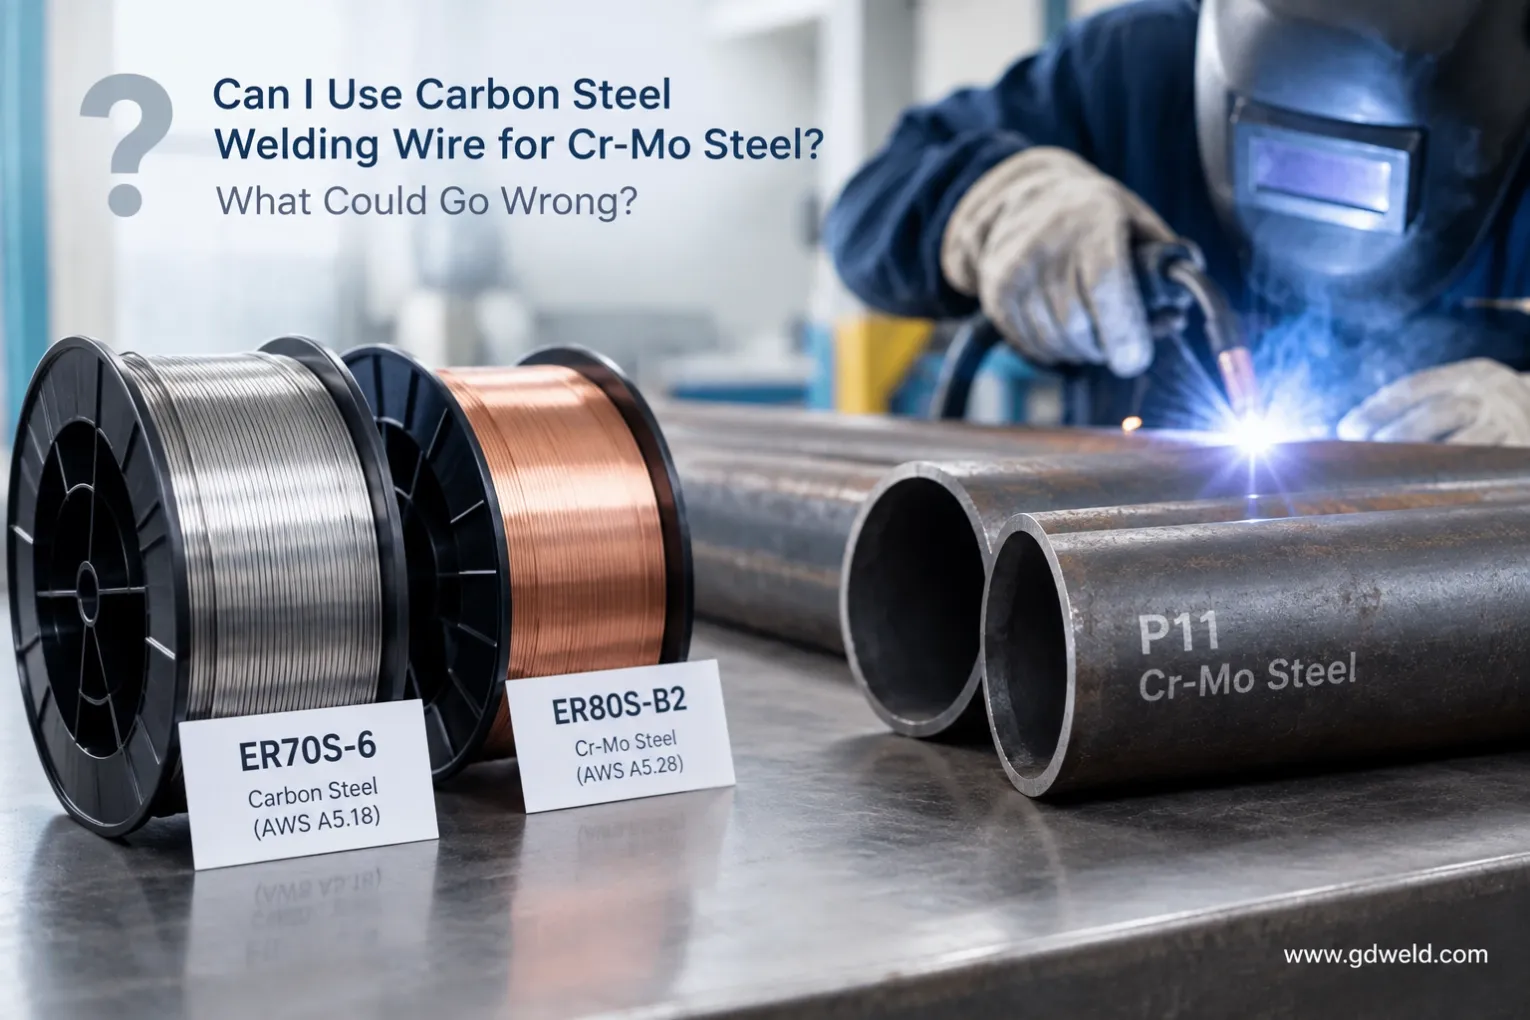
Can I Use Carbon Steel Welding Wire for Cr-Mo Steel? What Could Go Wrong?
Can you use ER70S-6 carbon steel welding wire for Cr-Mo steel? What could go wrong, and when should ER80S-B2 or another Cr-Mo welding wire be used instead?
About GD WELD
Specialty Welding Consumables
Looking for a specific or hard-to-source welding grade? Send us your AWS classification, base material, diameter and application. We will help you identify a suitable product and supply solution.
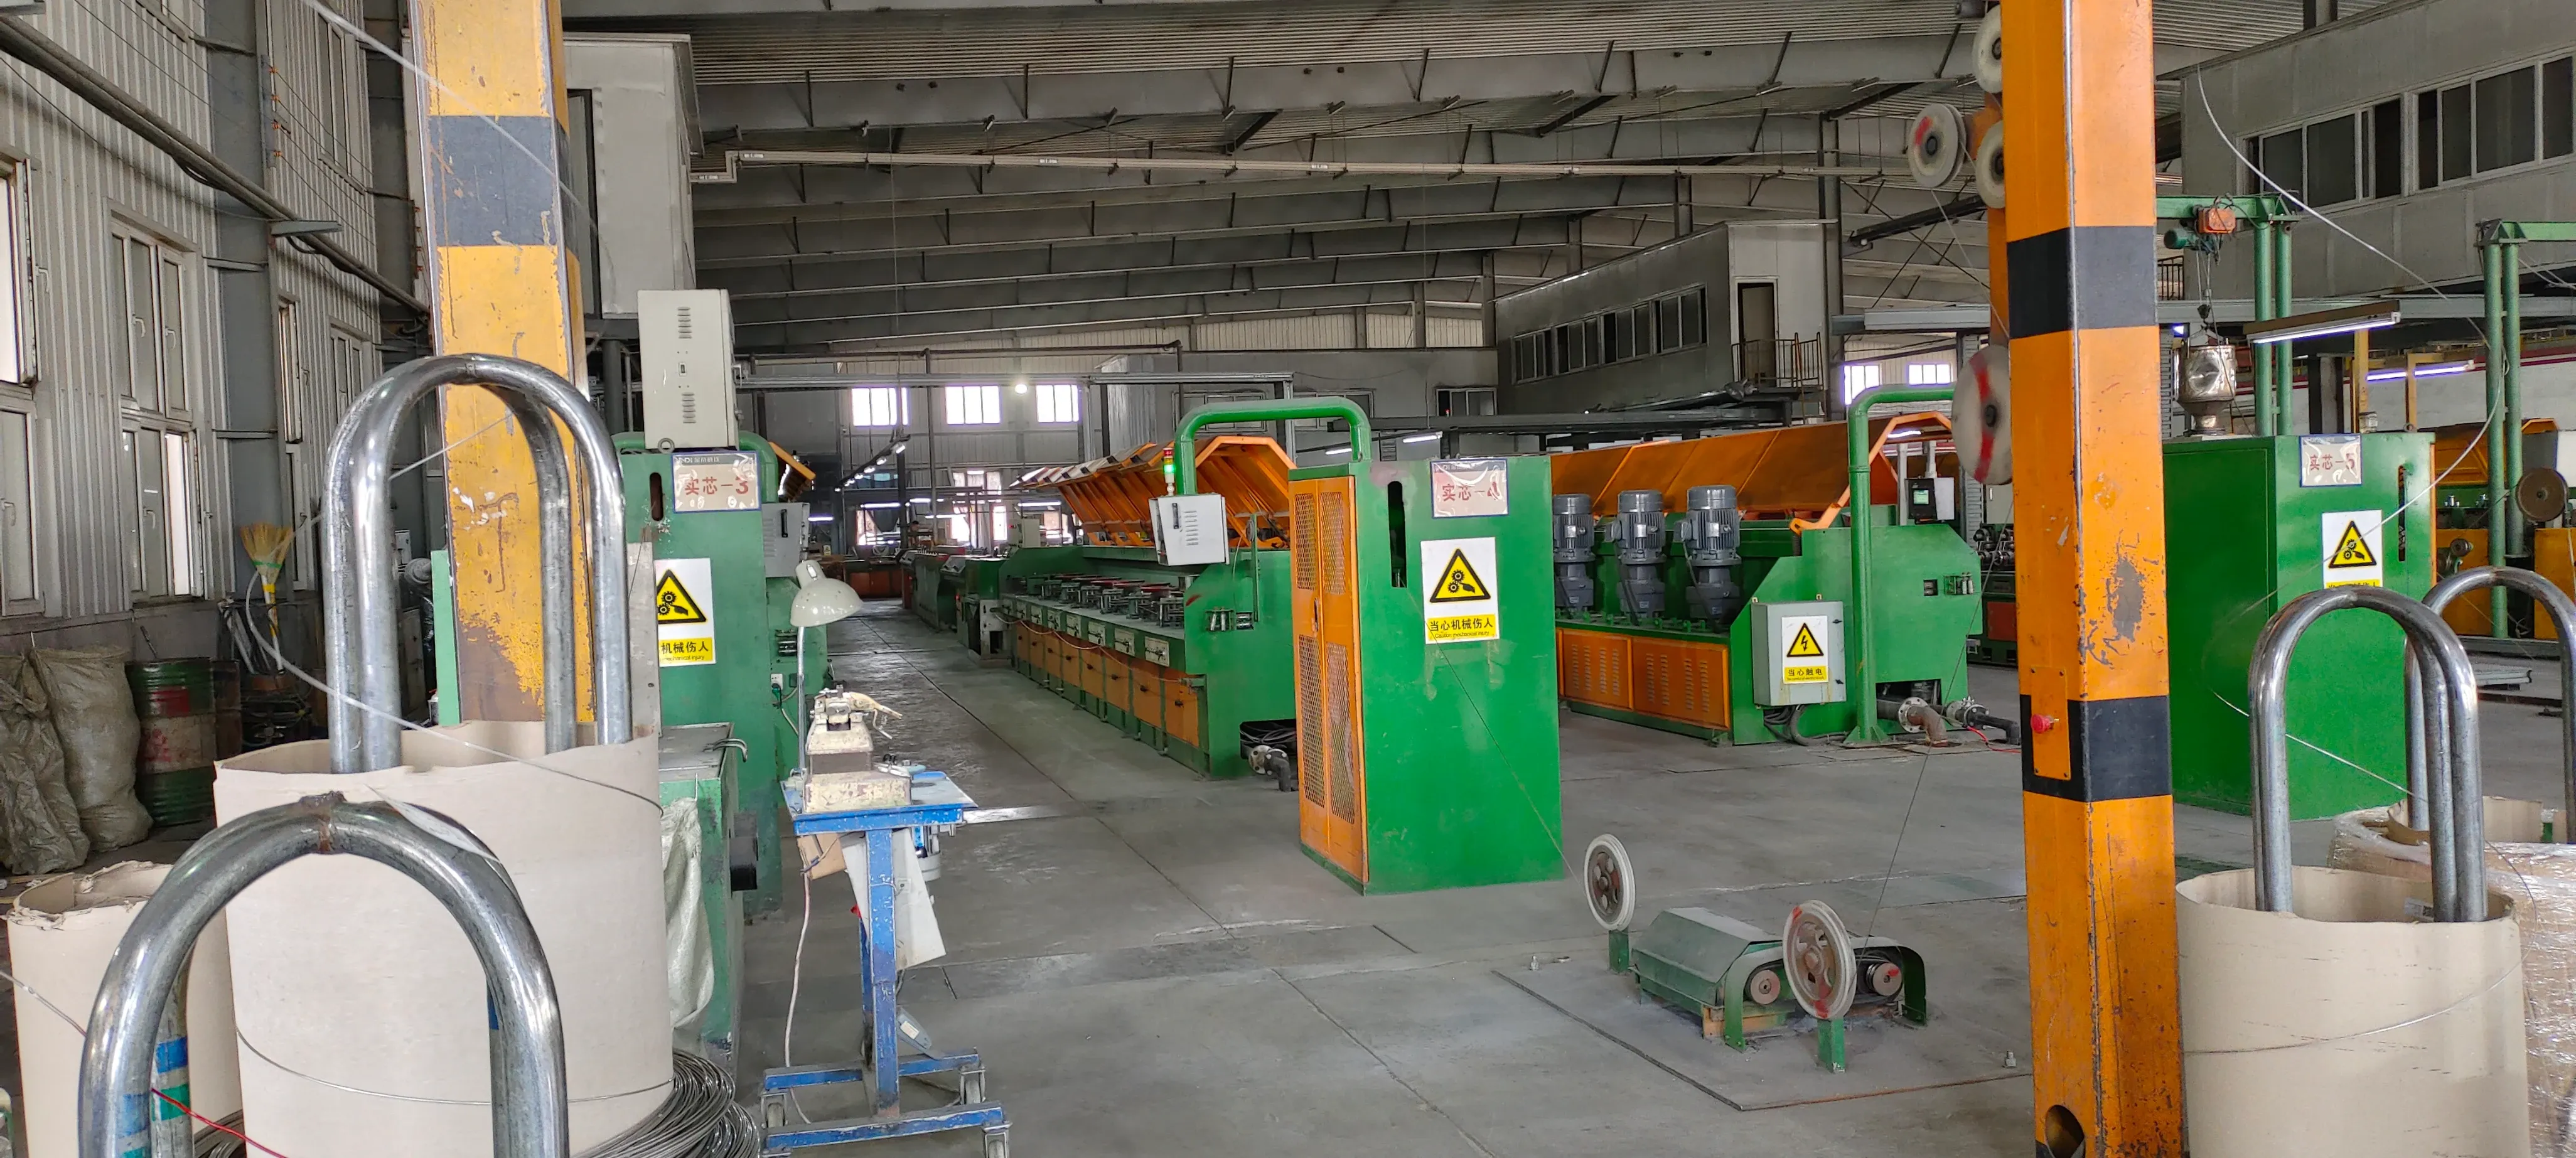
GD WELD is a China-based specialty welding consumables supplier, focused on sourcing and supplying welding wires and electrodes for demanding industrial applications. Specialty Grades · Reliable Sourcing · Technical Matching · Global Supply
Contact
Specialty Welding Consumables
Need a hard-to-source welding consumables? Please contact GD WELD.
Email
info@gdweld.com
WHATSAPP
+86 189 5451 5522
Office
District Lingcheng,City Dezhou,Province Shandong,
China
Working Time
From Monday To Friday
Inquiry
Send the Inquiry
If you are looking for a specific or hard-to-source welding grade...