All products
111 products
Heat Resistant & Cr-Mo
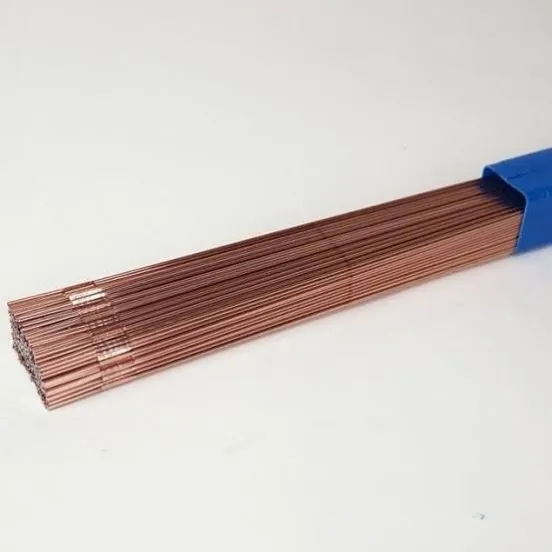
R31 TIG Welding Wire for 12Cr1MoV Steel
R31 TIG welding wire is used for welding specified low-alloy heat-resistant steels, including 12Cr1MoV when supported by the applicable welding procedure. It is intended for applications such as boiler piping and power-generation equipment where weld-metal properties and service conditions must be carefully controlled. GD WELD can help buyers confirm the applicable standard, available diameter, chemical composition and technical documentation before ordering.
Welding Wire
ER308H Stainless Steel Welding Wire
ER308H is a higher-carbon austenitic stainless steel filler metal used for specified welding applications involving 304H stainless steel. Its controlled carbon content of 0.04%–0.08% distinguishes it from low-carbon ER308L and makes it relevant to welding procedures designed for elevated-temperature service.
Welding Wire
ER308LSi Stainless Steel Welding Wire
ER308LSi is a low-carbon austenitic stainless steel filler metal with higher silicon content than ER308L. It offers improved weld-pool wetting and bead formation for suitable stainless steel welding applications. GD WELD supplies ER308LSi as MIG solid wire and TIG filler rods, subject to availability and technical specifications.
Welding Electrode
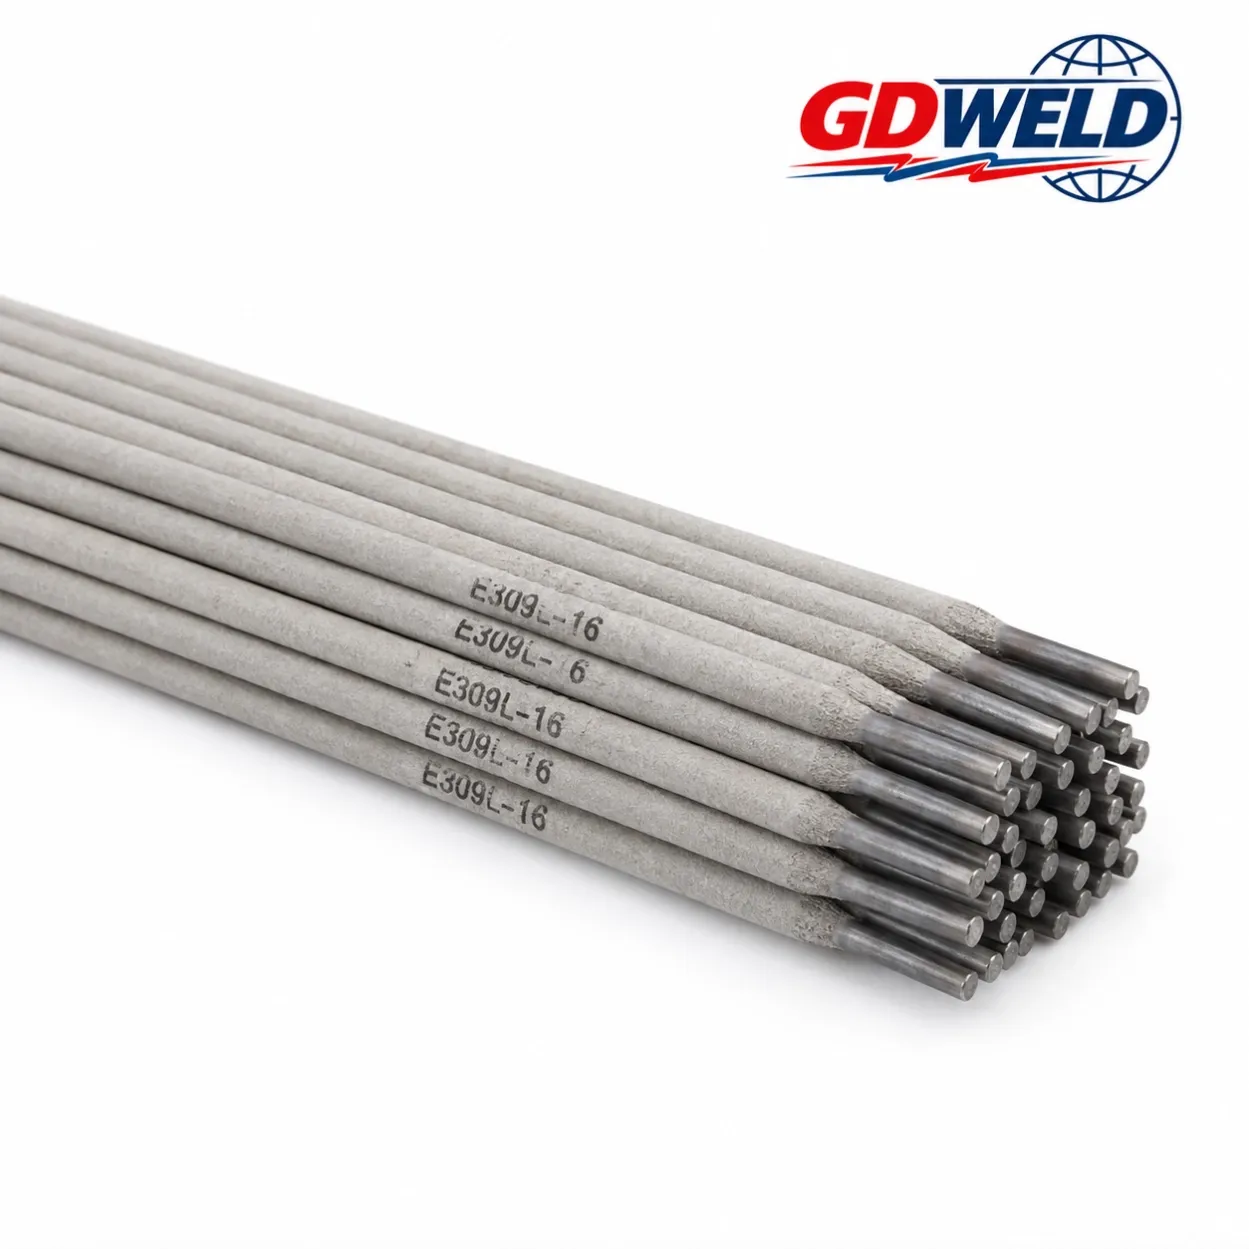
E309L-16 Stainless Steel Welding Electrode
E309L-16 is a low-carbon stainless steel welding electrode with a nominal 23% Cr–12% Ni weld-metal composition. It is commonly used for joining stainless steel to carbon steel and suitable low-alloy steel, as well as specified 309L-type welding and cladding applications.
Low Alloy & High Strength
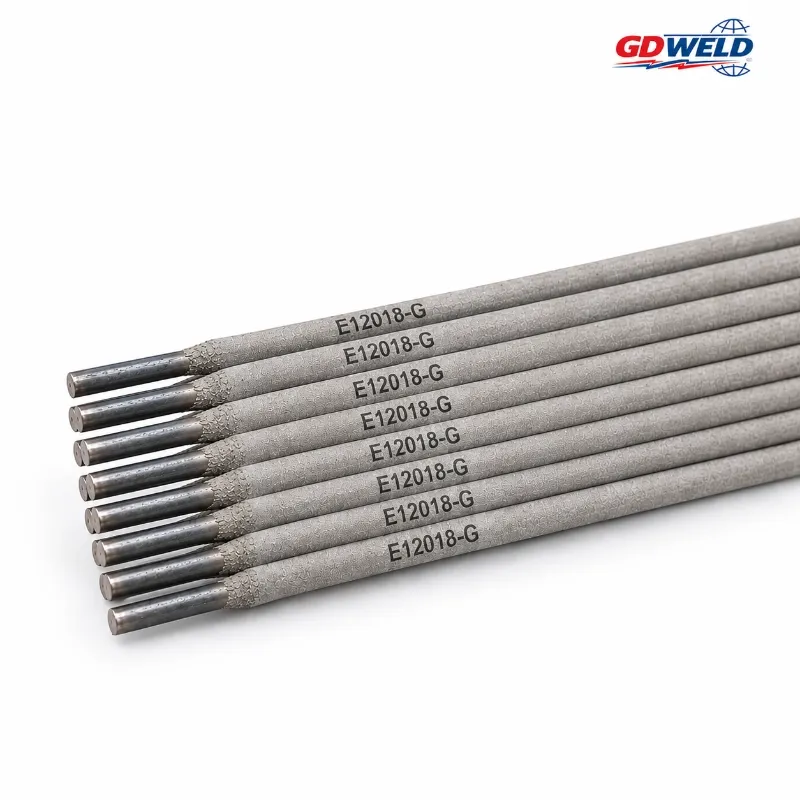
E12018-G 120 ksi High Strength Low Alloy Welding Electrode
E12018-G is a 120 ksi high-strength low-hydrogen welding electrode for SMAW. It is designed for demanding high-strength and low-alloy steels where higher weld-metal strength is required. As a G-type AWS classification, E12018-G does not define one universal weld-metal chemistry. Actual composition, toughness and performance should be confirmed from the product TDS and MTC.
Low Alloy & High Strength
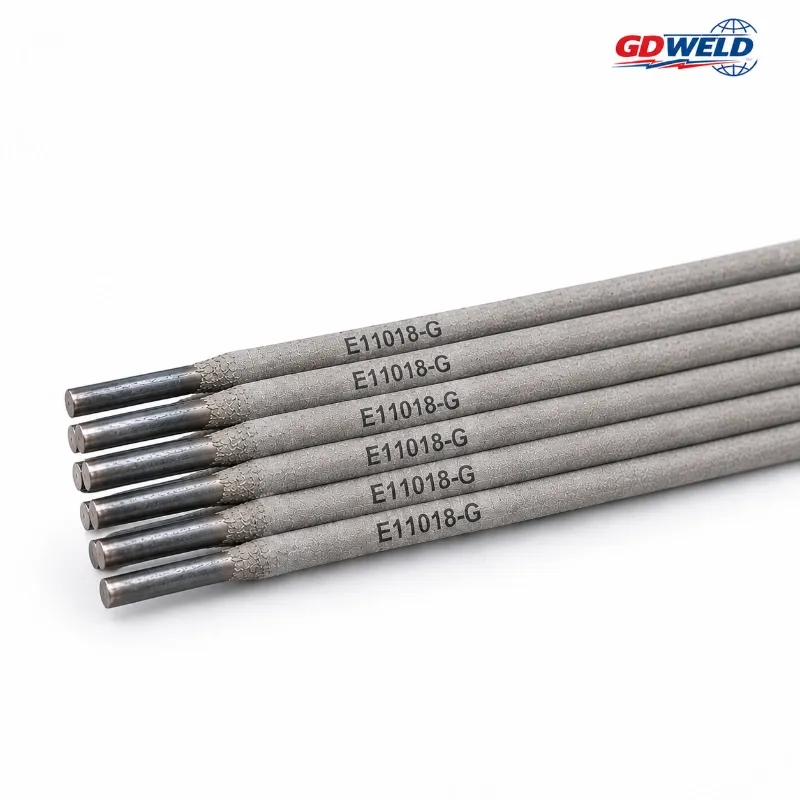
E11018-G High Strength Low Alloy Welding Electrode
E11018-G is a 110 ksi high-strength low-hydrogen welding electrode for SMAW. It is designed for welding high-strength and low-alloy steels where high weld-metal strength, suitable toughness and controlled hydrogen levels are required. Depending on the qualified product formulation, E11018-G can be used for Q&T steels, fine-grained structural steels, T-1-type steels and heavy industrial fabrication.
Low Alloy & High Strength
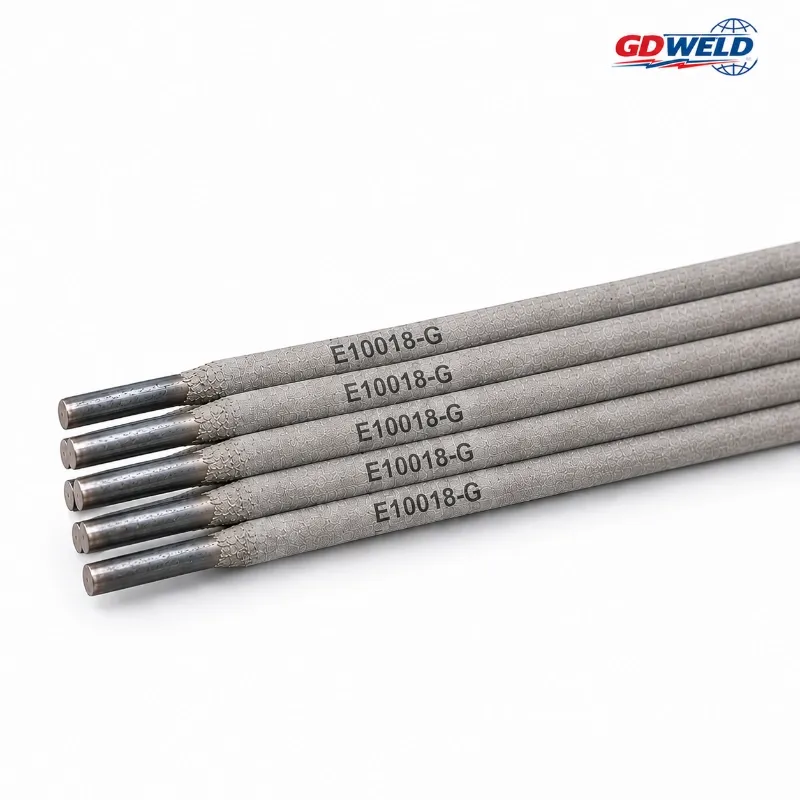
E10018-G High Strength Low Alloy Welding Electrode
E10018-G is a 100 ksi high-strength low-hydrogen SMAW electrode for welding high-strength and low-alloy steels. Depending on the qualified product formulation, it can be used for HSLA structures, X80 pipeline steel, pressure equipment and other demanding industrial applications. As a G-type AWS classification, E10018-G does not represent one fixed weld-metal chemistry. The actual formulation and toughness performance should be confirmed from the product TDS and MTC.
Low Alloy & High Strength
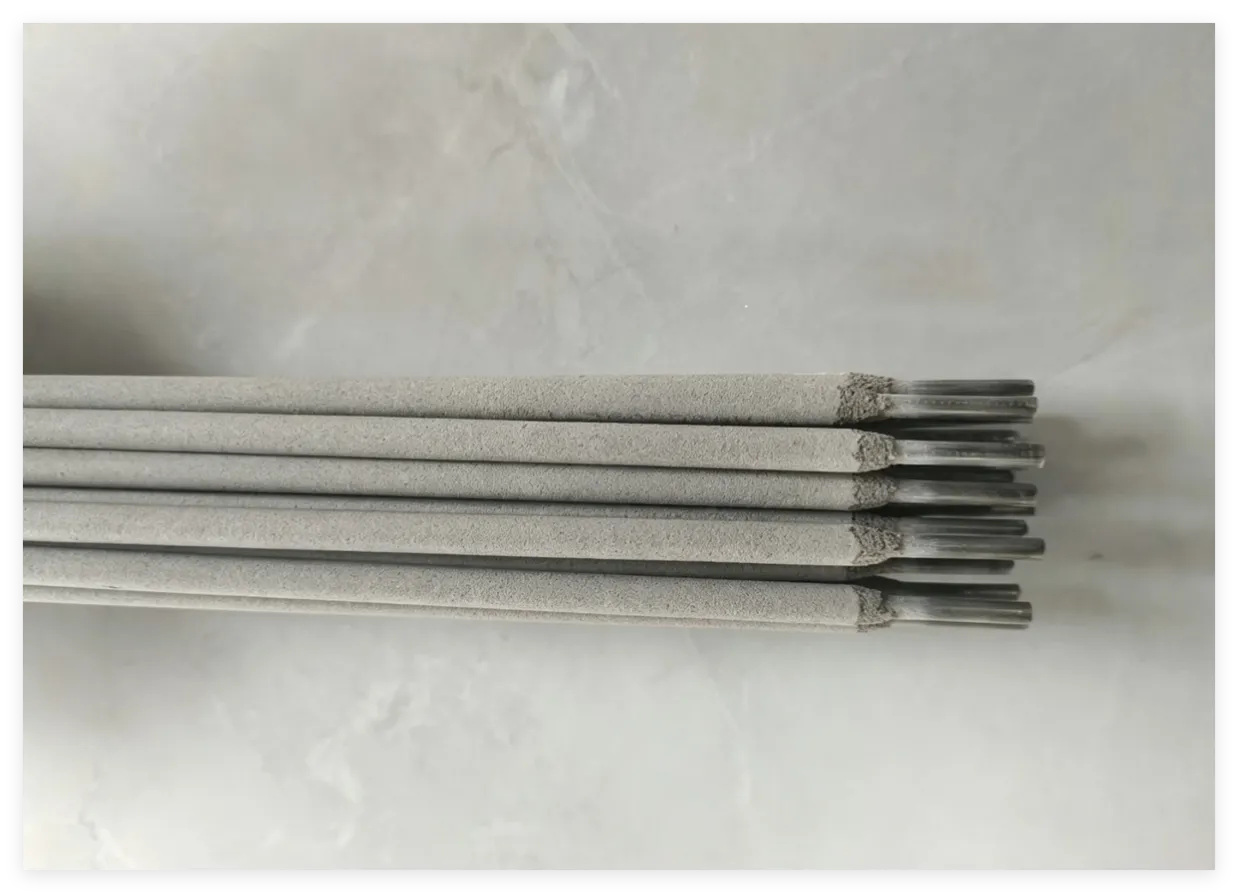
E9018-G High Strength Low Alloy Welding Electrode
E9018-G is a 90 ksi high-strength low-alloy steel welding electrode classified under AWS A5.5/A5.5M. It is a basic, low-hydrogen SMAW electrode for high-strength steel and demanding low-alloy welding applications. Unlike fixed-alloy classifications such as E9018-B2, E9018-B3 and E9018-B91, the E9018-G classification allows an agreed weld-metal chemistry. The manufacturer's TDS and MTC are therefore important when selecting the electrode for a specific steel grade or application.
Heat Resistant & Cr-Mo
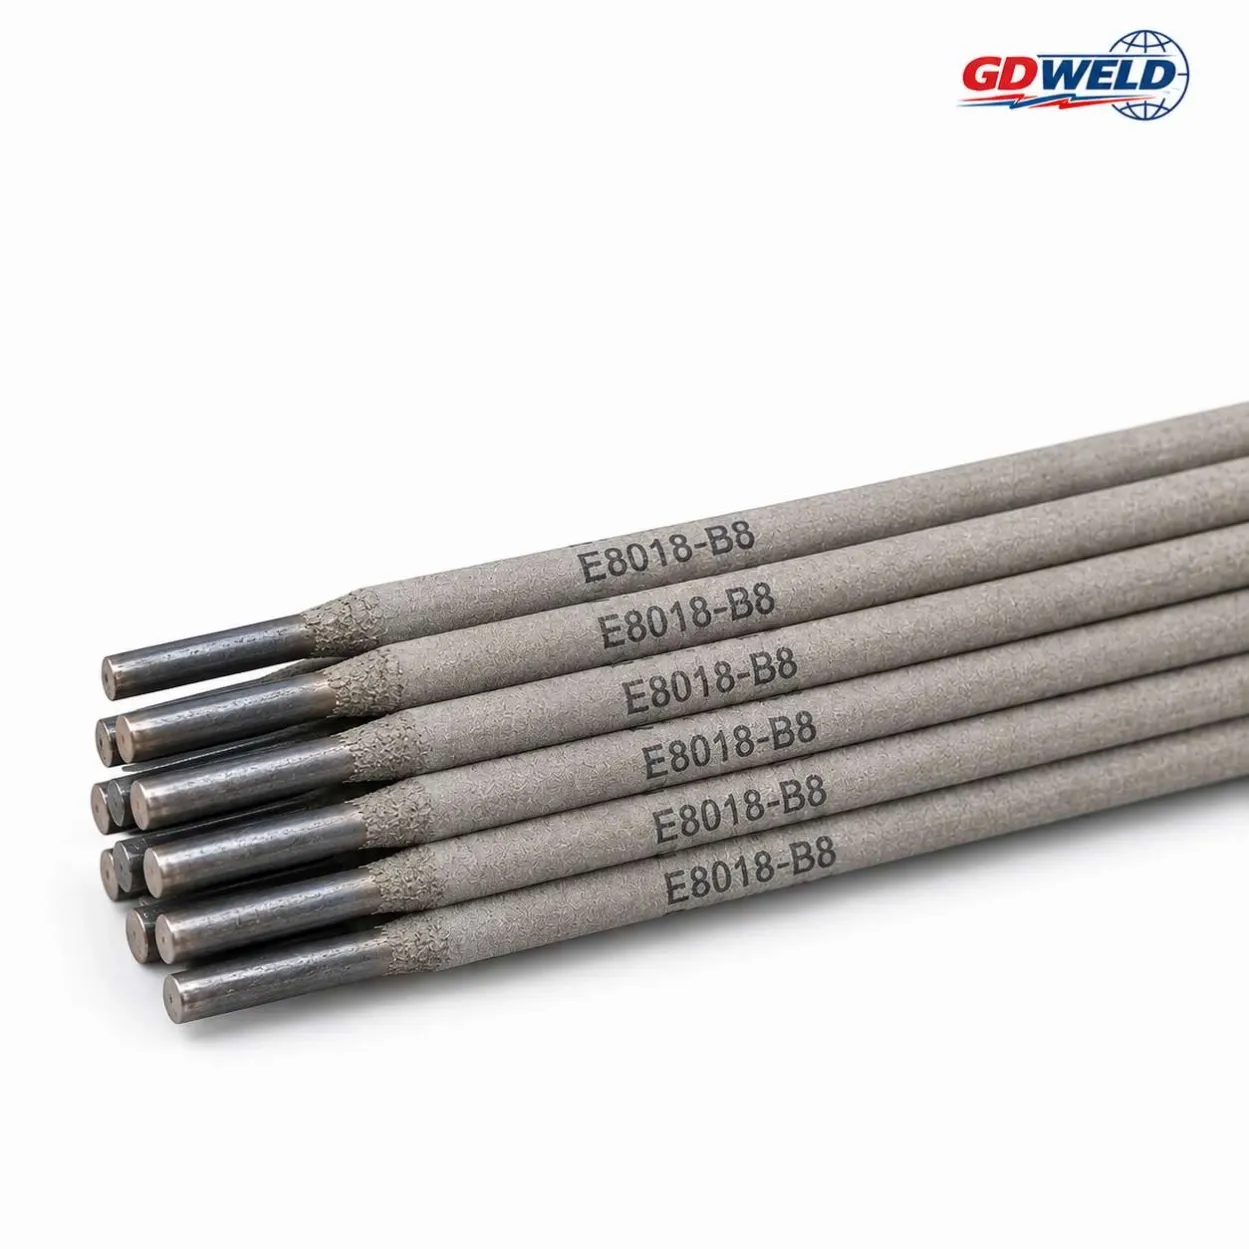
E8018-B8 Cr-Mo Welding Electrode for P9 and T9 Steel
E8018-B8 is a low-hydrogen Cr-Mo SMAW electrode for 9Cr-1Mo steels, including ASTM A335 P9 and ASTM A213 T9. It is used for high-temperature piping, boilers, pressure equipment, refinery and petrochemical applications where weld-metal compatibility with the 9Cr-1Mo base-metal system is required.
Heat Resistant & Cr-Mo
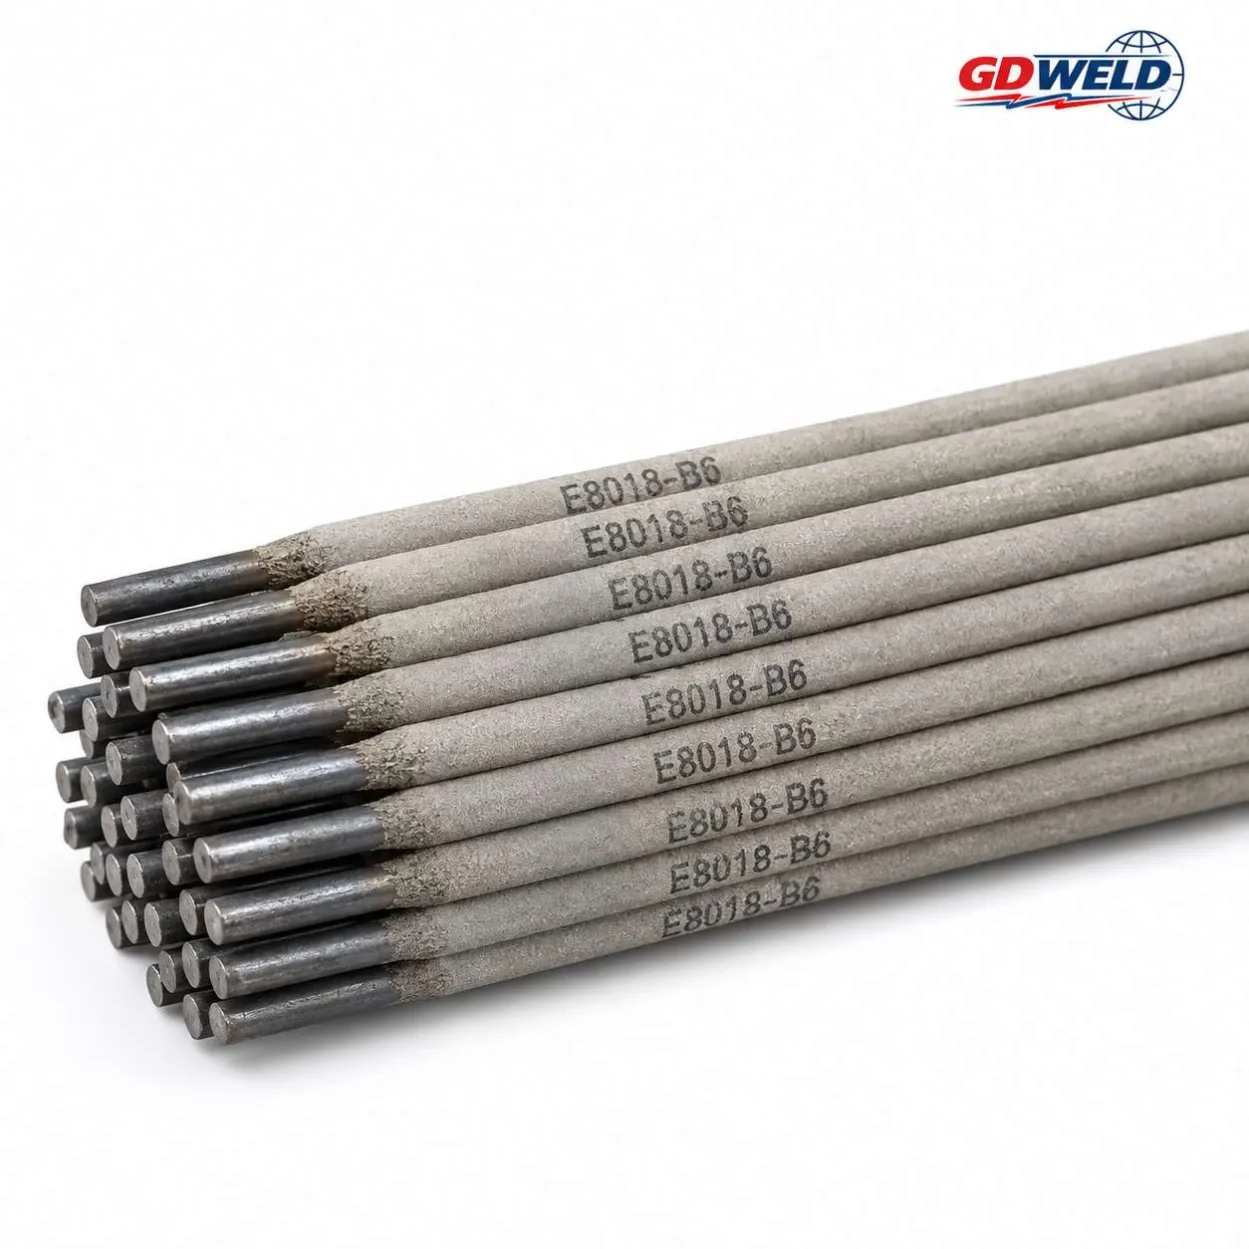
E8018-B6 Cr-Mo Welding Electrode for P5 and T5 Steel
E8018-B6 is a low-hydrogen Cr-Mo welding electrode for 5Cr-0.5Mo heat-resistant steel. It is mainly used for ASTM A335 P5, A213 T5 and similar Cr-Mo steels in refinery piping, petrochemical equipment, boilers, pressure vessels and high-temperature process systems. Classified under AWS A5.5/A5.5M E8018-B6, the electrode produces weld metal with a controlled chromium-molybdenum alloy system for matching 5Cr-0.5Mo steel. E502 is an older classification designation associated with this electrode ty
Page 8 of 12
Technical Blog
Welding Guides & Technical Resources
Practical guides for selecting welding consumables, understanding AWS classifications and solving material-specific welding challenges.
View all
FeaturedOct 16, 2026
ER2209 vs E2209 for Duplex 2205: Solid Wire, Flux-Cored Wire, or Stick Electrode?
Choosing ER2209 solid wire, E2209 flux-cored wire, or a stick electrode for Duplex 2205? Compare the product forms, welding processes, and key selection requirements.
Latest
Oct 15, 2026
Can I Substitute One AWS Welding Wire for Another? What Should I Check?
Can you replace one AWS welding wire with another? Check classification, base material, mechanical properties and welding procedure requirements before approving a substitute.
Oct 13, 2026
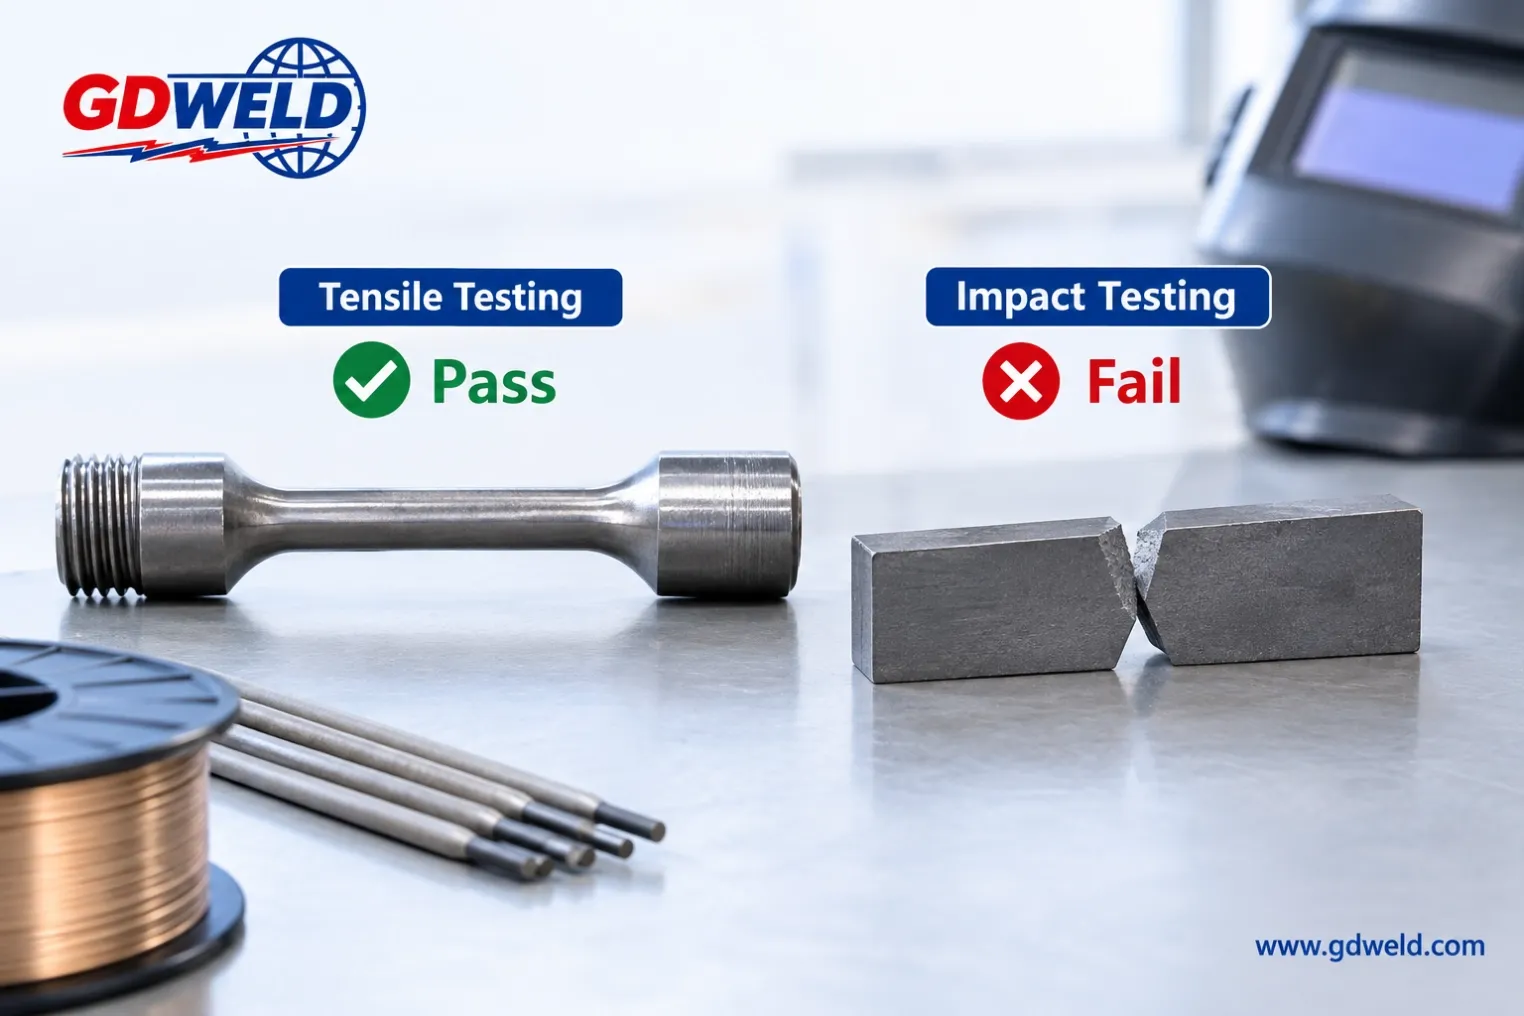
Why Does My Low-Temperature Weld Pass Tensile Test but Fail Charpy Impact Test?
Why does a low-temperature weld pass tensile test but fail the Charpy impact test? Learn how welding wire selection, weld toughness and temperature affect low-temperature steel welding performance.
About GD WELD
Specialty Welding Consumables
Looking for a specific or hard-to-source welding grade? Send us your AWS classification, base material, diameter and application. We will help you identify a suitable product and supply solution.
GD WELD is a China-based specialty welding consumables supplier, focused on sourcing and supplying welding wires and electrodes for demanding industrial applications. Specialty Grades · Reliable Sourcing · Technical Matching · Global Supply
Contact
Specialty Welding Consumables
Need a hard-to-source welding consumables? Please contact GD WELD.
Email
info@gdweld.com
WHATSAPP
+86 189 5451 5522
Office
District Lingcheng,City Dezhou,Province Shandong,
China
Working Time
From Monday To Friday
Inquiry
Send the Inquiry
If you are looking for a specific or hard-to-source welding grade...