
Can E6011 Weld Through Rust or Paint? What Should You Remove First?
Can E6011 weld through rust or paint? Learn what surface contamination it can tolerate, what must be removed first, and how to prevent weld defects.
Technical Blog
Practical guides for selecting welding consumables, understanding AWS classifications and solving material-specific welding challenges.
Can E6011 weld through rust or paint? Learn what surface contamination it can tolerate, what must be removed first, and how to prevent weld defects.
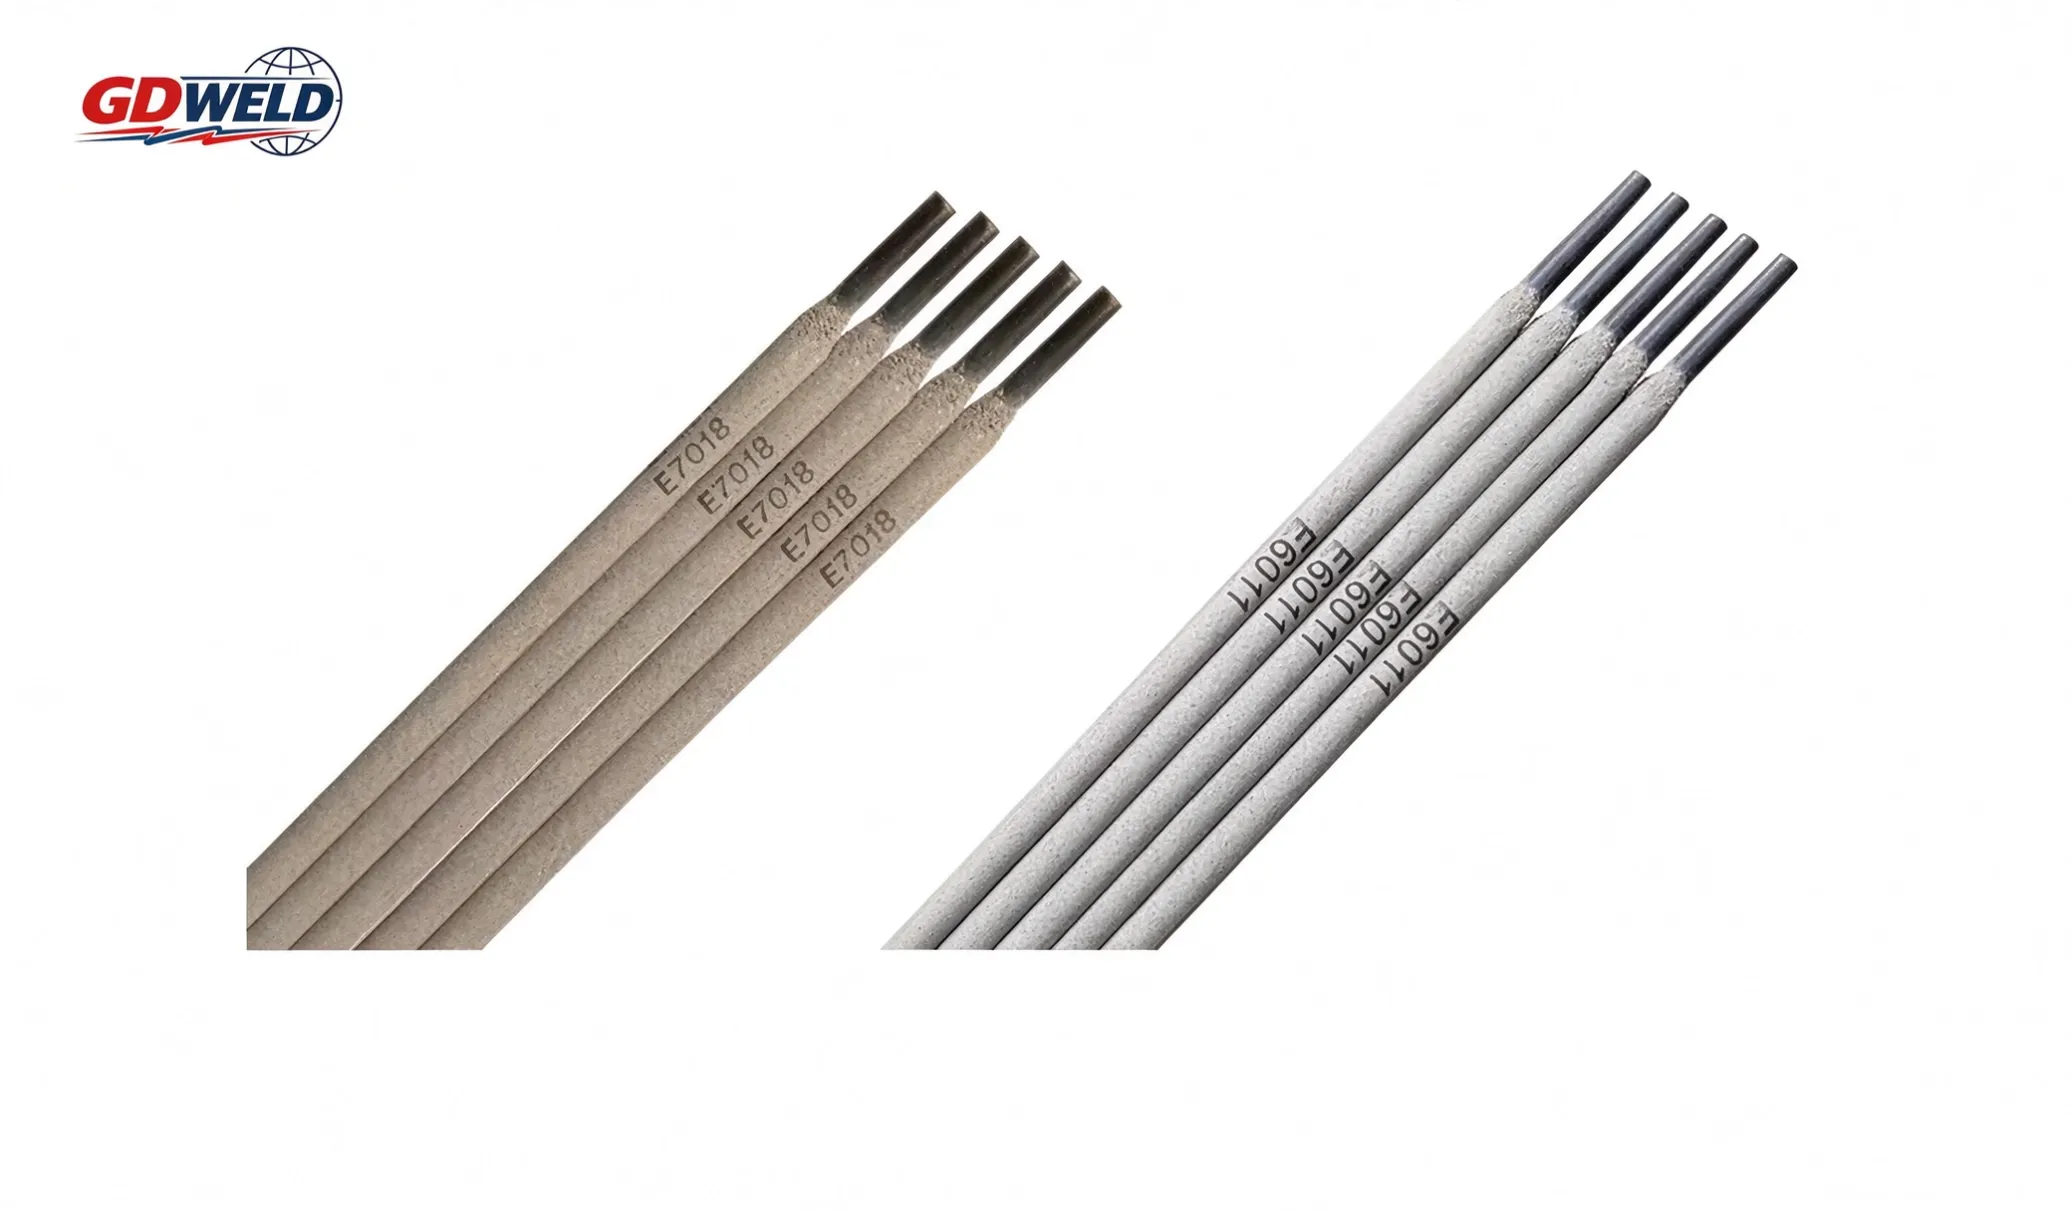
Compare E6011 vs E7018 welding electrodes. Learn about coating, penetration, strength, applications and storage to choose the right electrode.
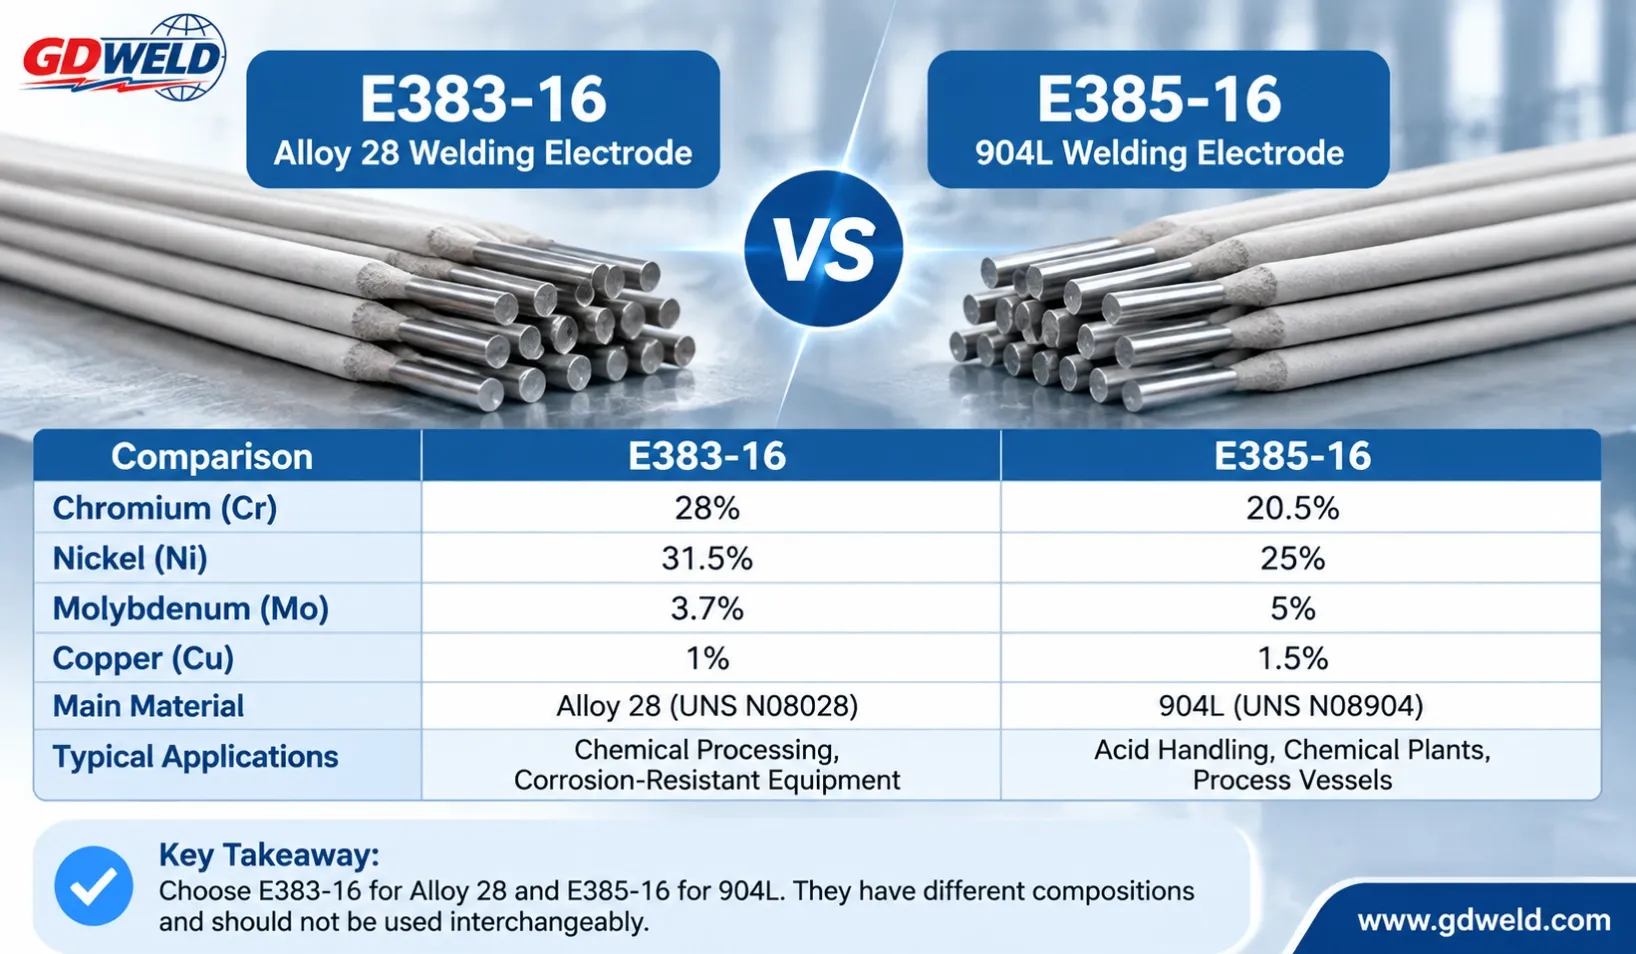
What is the difference between E383-16 and E385-16? Compare their chemical composition, applications, and suitability for Alloy 28 and 904L.
Which welding electrode is suitable for Alloy 28 (UNS N08028)? Learn when to use E383-16 or ER383 and what to check before welding.
Compare ER4043 and ER5356 welding wire for 6061 aluminum. Learn about weld strength, cracking resistance and filler metal selection.
Can E6011 weld thin metal without burn-through? Learn how electrode size, current, arc length and travel speed affect thin steel welding.
Why does moisture matter for E7018 welding rods? Learn proper storage, exposure control and when drying or rebaking may be necessary.
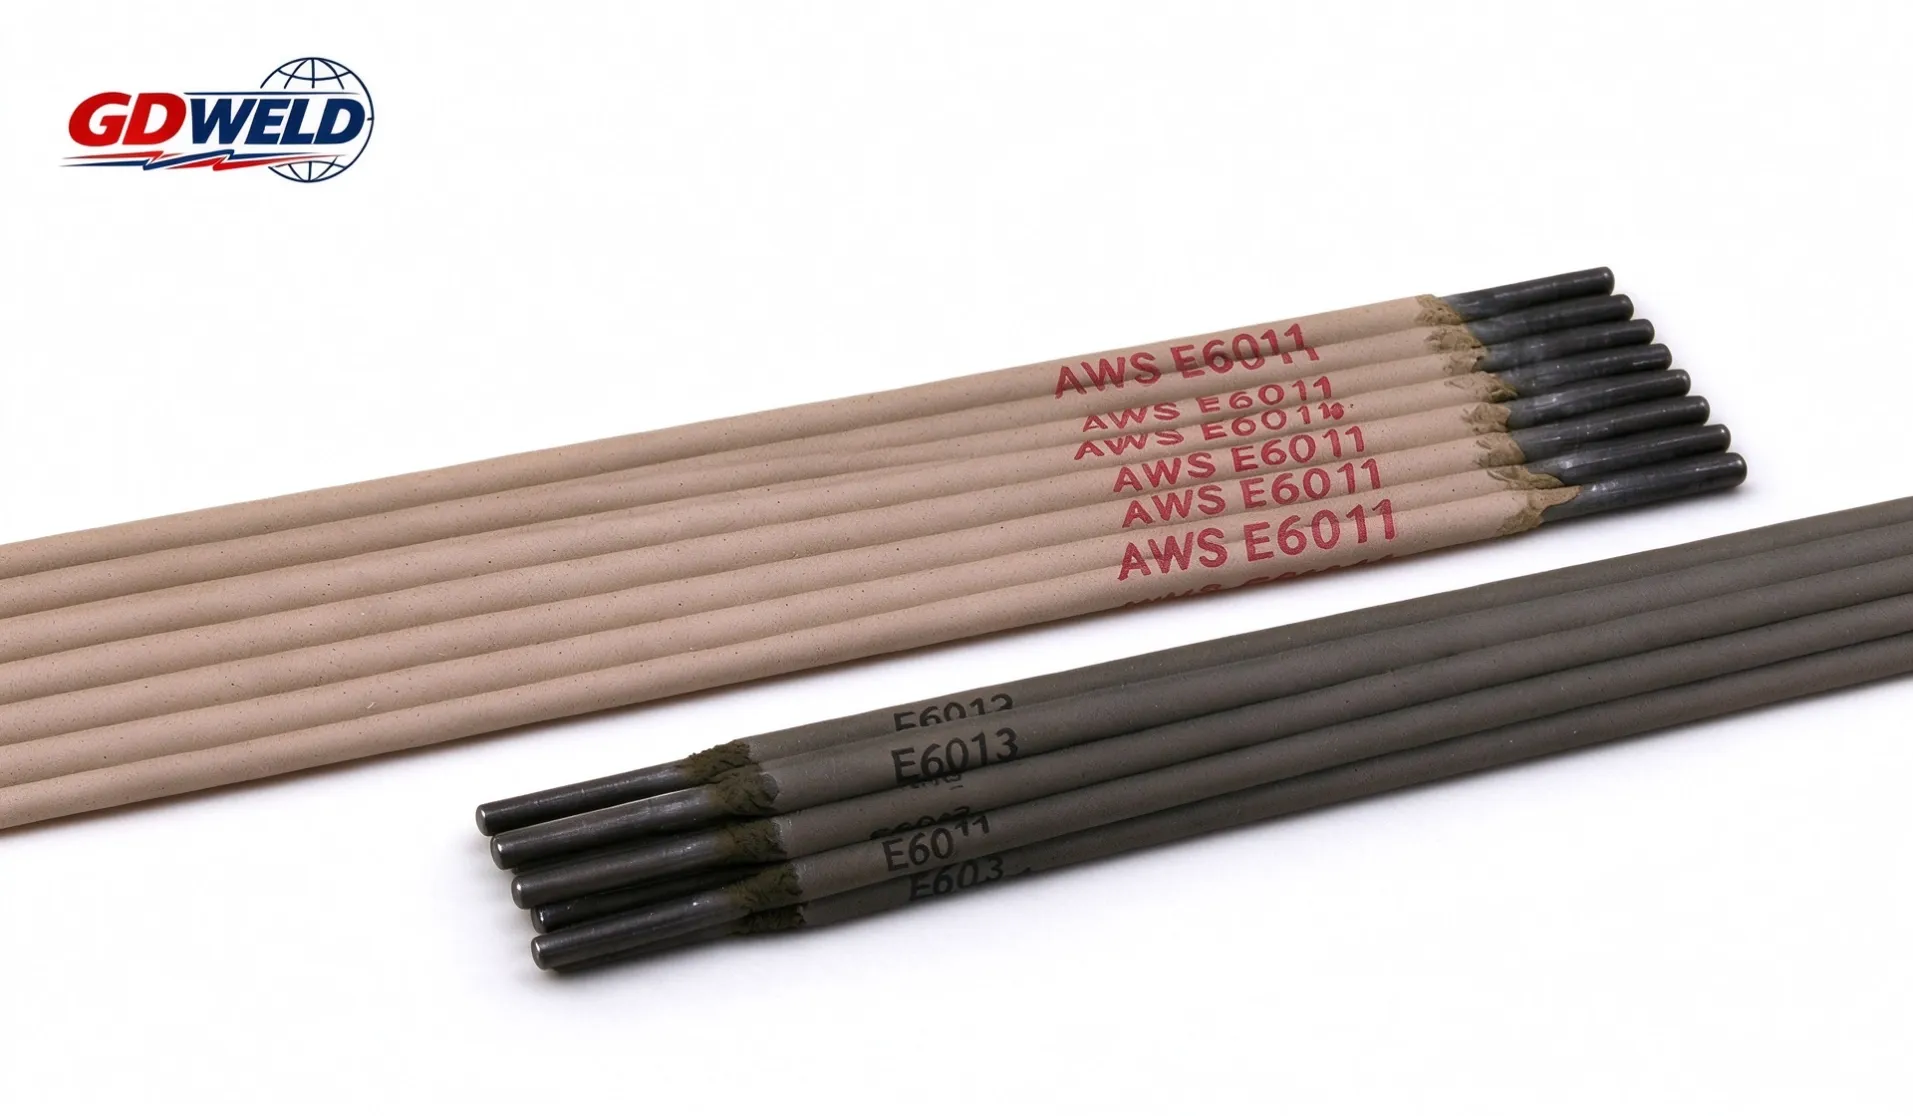
Compare E6011 vs E6013 welding rods for penetration, arc control, thin steel, surface condition and common applications. Find the right electrode for your job.
Why does an E6011 weld have porosity? Identify common causes and learn how to fix pinholes by checking arc length, electrode condition, surface contamination and welding settings.
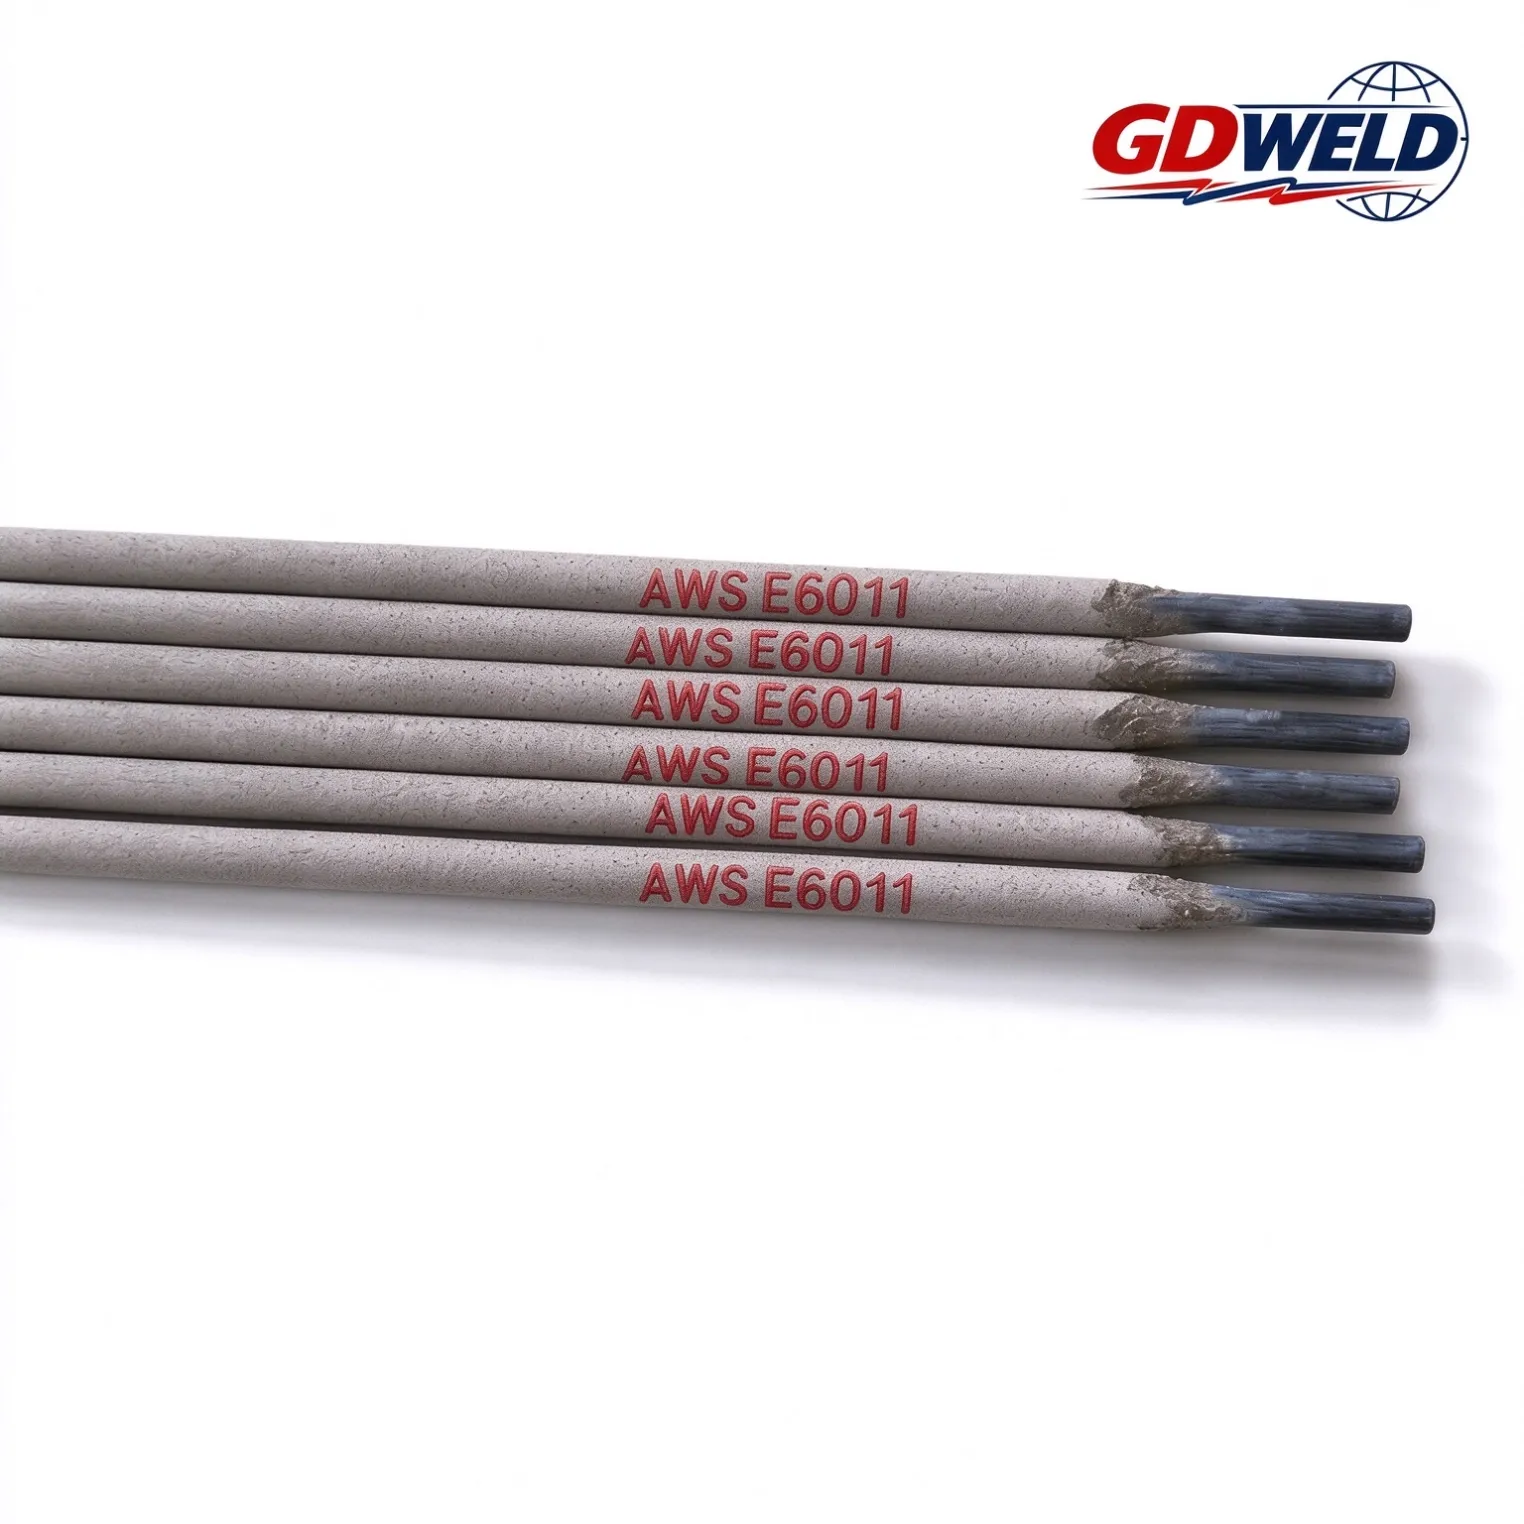
What amperage should you use for E6011 welding rods? Learn how electrode diameter, welding position and material thickness affect current settings.
Recommended products
Popular pieces selected to support the routines, repairs, and ideas featured in our journal.
ER420 is a high-carbon 13% chromium martensitic stainless steel solid welding wire and hardfacing filler metal classified under AWS A5.9. With higher carbon content than ER410, it delivers superior weld-metal hardness and abrasion resistance, making it ideal for welding matching 420 stainless steel and repairing or surfacing wear-resistant components.
ER309LMo (S309LMo) is a molybdenum-alloyed chromium-nickel stainless steel welding wire. Its higher molybdenum content distinguishes it from conventional ER309L and makes it suitable for applications where a Mo-containing filler metal is specified. GD WELD offers ER309LMo welding wire in 0.8, 1.0, 1.2, 1.6, 2.0, 2.4 and 3.2 mm diameters. The supplied 1.2 mm material certificate reports 23.18% chromium, 13.86% nickel, 2.12% molybdenum and 620 MPa deposited weld metal tensile strength.
ER410NiMo is a chromium-nickel-molybdenum stainless steel welding wire designation listed in AWS A5.9-2022. The supplied material certificate also identifies the product as H05Cr12Ni4Mo. GD WELD supplies this welding wire in a tested diameter of 1.2 mm. Its material certificate reports 12.27% chromium, 4.72% nickel, 0.49% molybdenum and a deposited weld metal tensile strength of 800 MPa.