
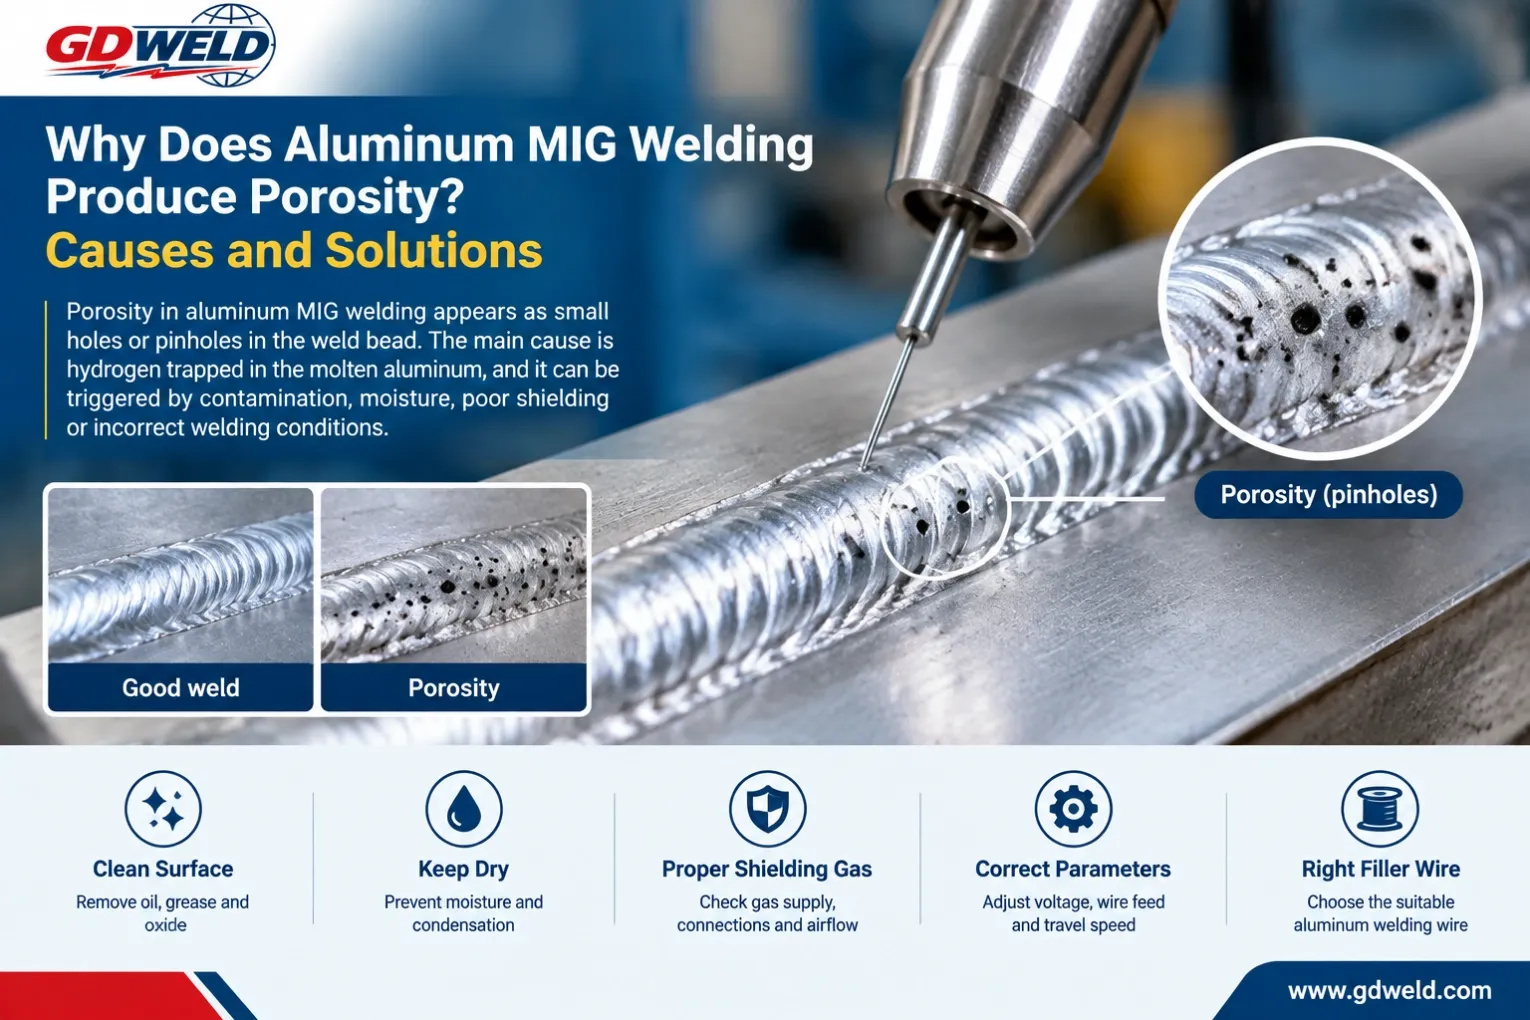
Why Does Aluminum MIG Welding Produce Porosity? Causes and Solutions
Learn what causes porosity in aluminum MIG welding and how to prevent it by checking contamination, moisture, shielding gas, wire feeding and welding settings.
Technical Blog
Practical guides for selecting welding consumables, understanding AWS classifications and solving material-specific welding challenges.
Learn what causes porosity in aluminum MIG welding and how to prevent it by checking contamination, moisture, shielding gas, wire feeding and welding settings.
E6011 or E6010 for pipe welding? Compare AC/DC compatibility, root pass applications, and welding procedure requirements before choosing an electrode.
ER1070 or ER1100 aluminum welding wire? Compare aluminum purity, applications and base-metal compatibility to select the right filler.
ER410 or ER420 welding wire? Learn the key differences in hardness, applications and heat treatment to select the right martensitic stainless steel filler.
ER309L vs ER308L welding wire: which filler metal suits your base metals? Compare common welding scenarios and key selection factors before ordering.
ER4043 vs ER4047 aluminum welding wire: compare silicon content, weldability, and applications to choose the right filler metal for 6061, 6063, and aluminum casting repair.
Need E2209-16 electrodes for Duplex 2205? Check these five key requirements before ordering to help avoid specification mismatches and procurement delays.
Why does a Duplex 2205 flux-cored weld fail corrosion tests? Learn how to investigate weld chemistry, phase balance, slag inclusions and surface contamination.
What is an E6013 welding electrode used for? Explore common applications, key advantages and limitations before choosing an electrode.
Can E308L weld 304, 304L, 321 or 347 stainless steel? Compare common applications and learn when another electrode may be more suitable.
Recommended products
Popular pieces selected to support the routines, repairs, and ideas featured in our journal.
ER420 is a high-carbon 13% chromium martensitic stainless steel solid welding wire and hardfacing filler metal classified under AWS A5.9. With higher carbon content than ER410, it delivers superior weld-metal hardness and abrasion resistance, making it ideal for welding matching 420 stainless steel and repairing or surfacing wear-resistant components.
ER309LMo (S309LMo) is a molybdenum-alloyed chromium-nickel stainless steel welding wire. Its higher molybdenum content distinguishes it from conventional ER309L and makes it suitable for applications where a Mo-containing filler metal is specified. GD WELD offers ER309LMo welding wire in 0.8, 1.0, 1.2, 1.6, 2.0, 2.4 and 3.2 mm diameters. The supplied 1.2 mm material certificate reports 23.18% chromium, 13.86% nickel, 2.12% molybdenum and 620 MPa deposited weld metal tensile strength.
ER410NiMo is a chromium-nickel-molybdenum stainless steel welding wire designation listed in AWS A5.9-2022. The supplied material certificate also identifies the product as H05Cr12Ni4Mo. GD WELD supplies this welding wire in a tested diameter of 1.2 mm. Its material certificate reports 12.27% chromium, 4.72% nickel, 0.49% molybdenum and a deposited weld metal tensile strength of 800 MPa.